We provide society with new value through our creativity and technological capabilities.
Since 1955 — Fine Chemicals & API Manufacturing
Sogo Pharmaceutical satisfies the needs of clients spanning a broad range of fields by providing them with everything from active pharmaceutical ingredients to advanced chemicals, functional cosmetic ingredients by primarily leveraging organic synthesis technologies that we have been cultivating since we were founded in 1955. The three competitive advantages that we have been building up over the course of 70 years are hereby introduced.
Ever since we were founded, we have worked closely with clients in the pharmaceutical, chemical, and cosmetics sectors to reliably supply a wide range of fine chemical products. Backed by our many years of experience, our proven manufacturing technology is a strength.
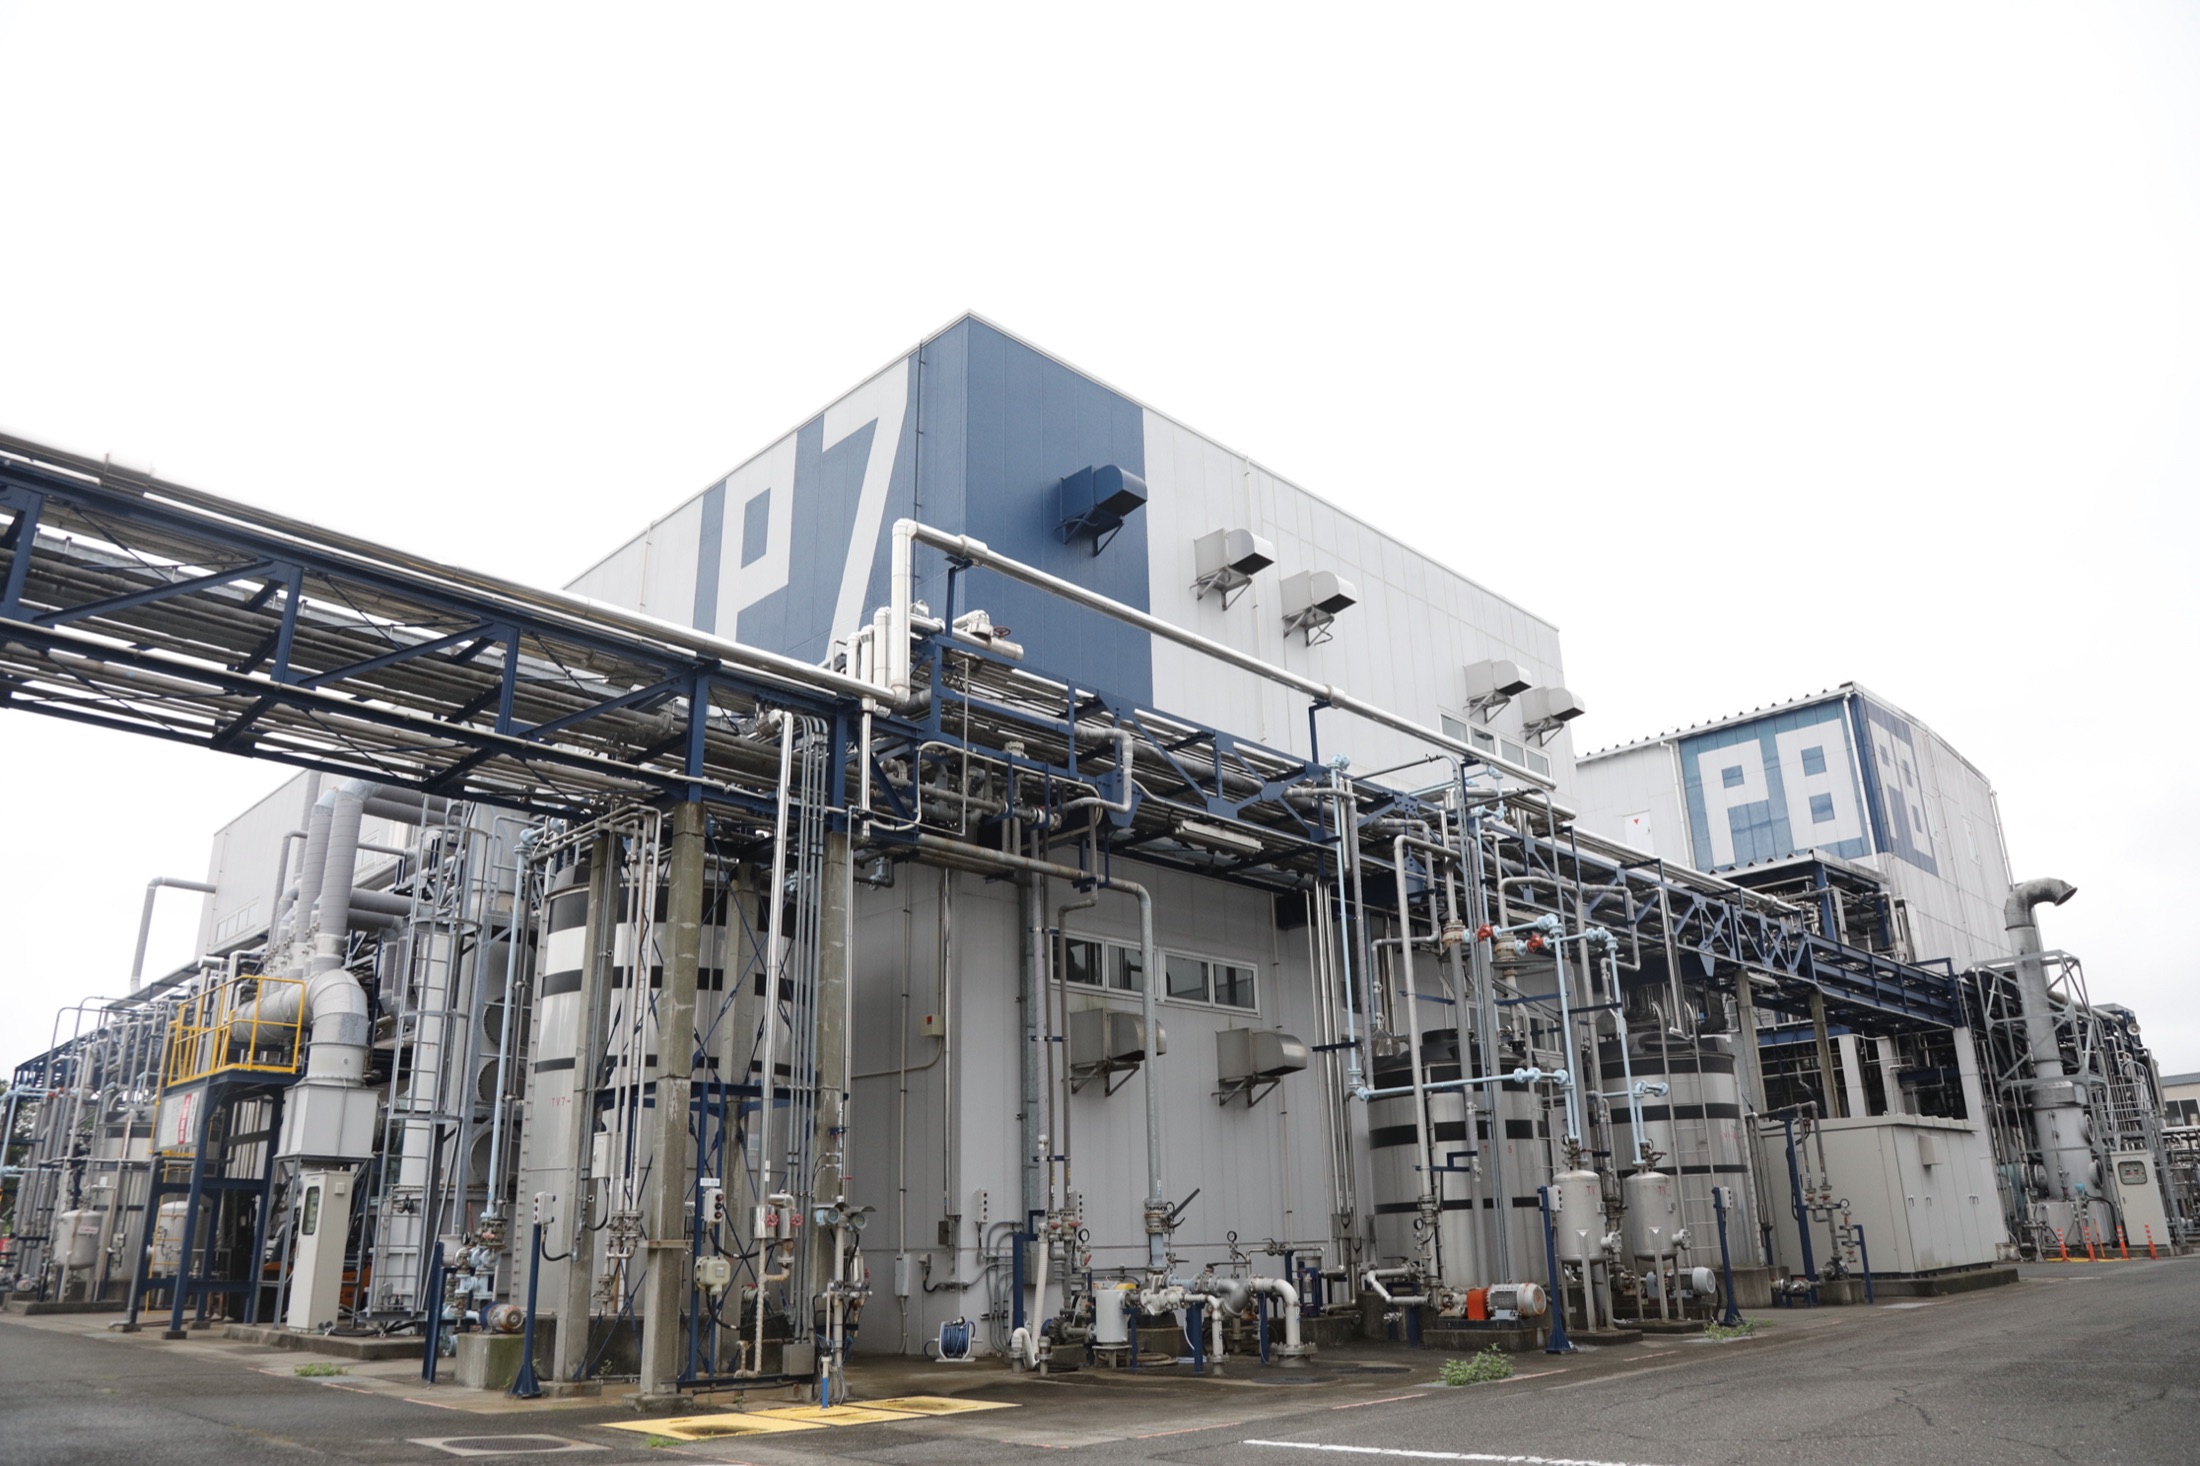
We can accommodate advanced synthesizing processes that involve everything from photoreactions and reactions at temperatures as low as -70℃ to reactions at temperatures as high as 200℃ as well as reactions based on the use of specialty ingredients. We are also capable of adapting to requirements for scaling up production.
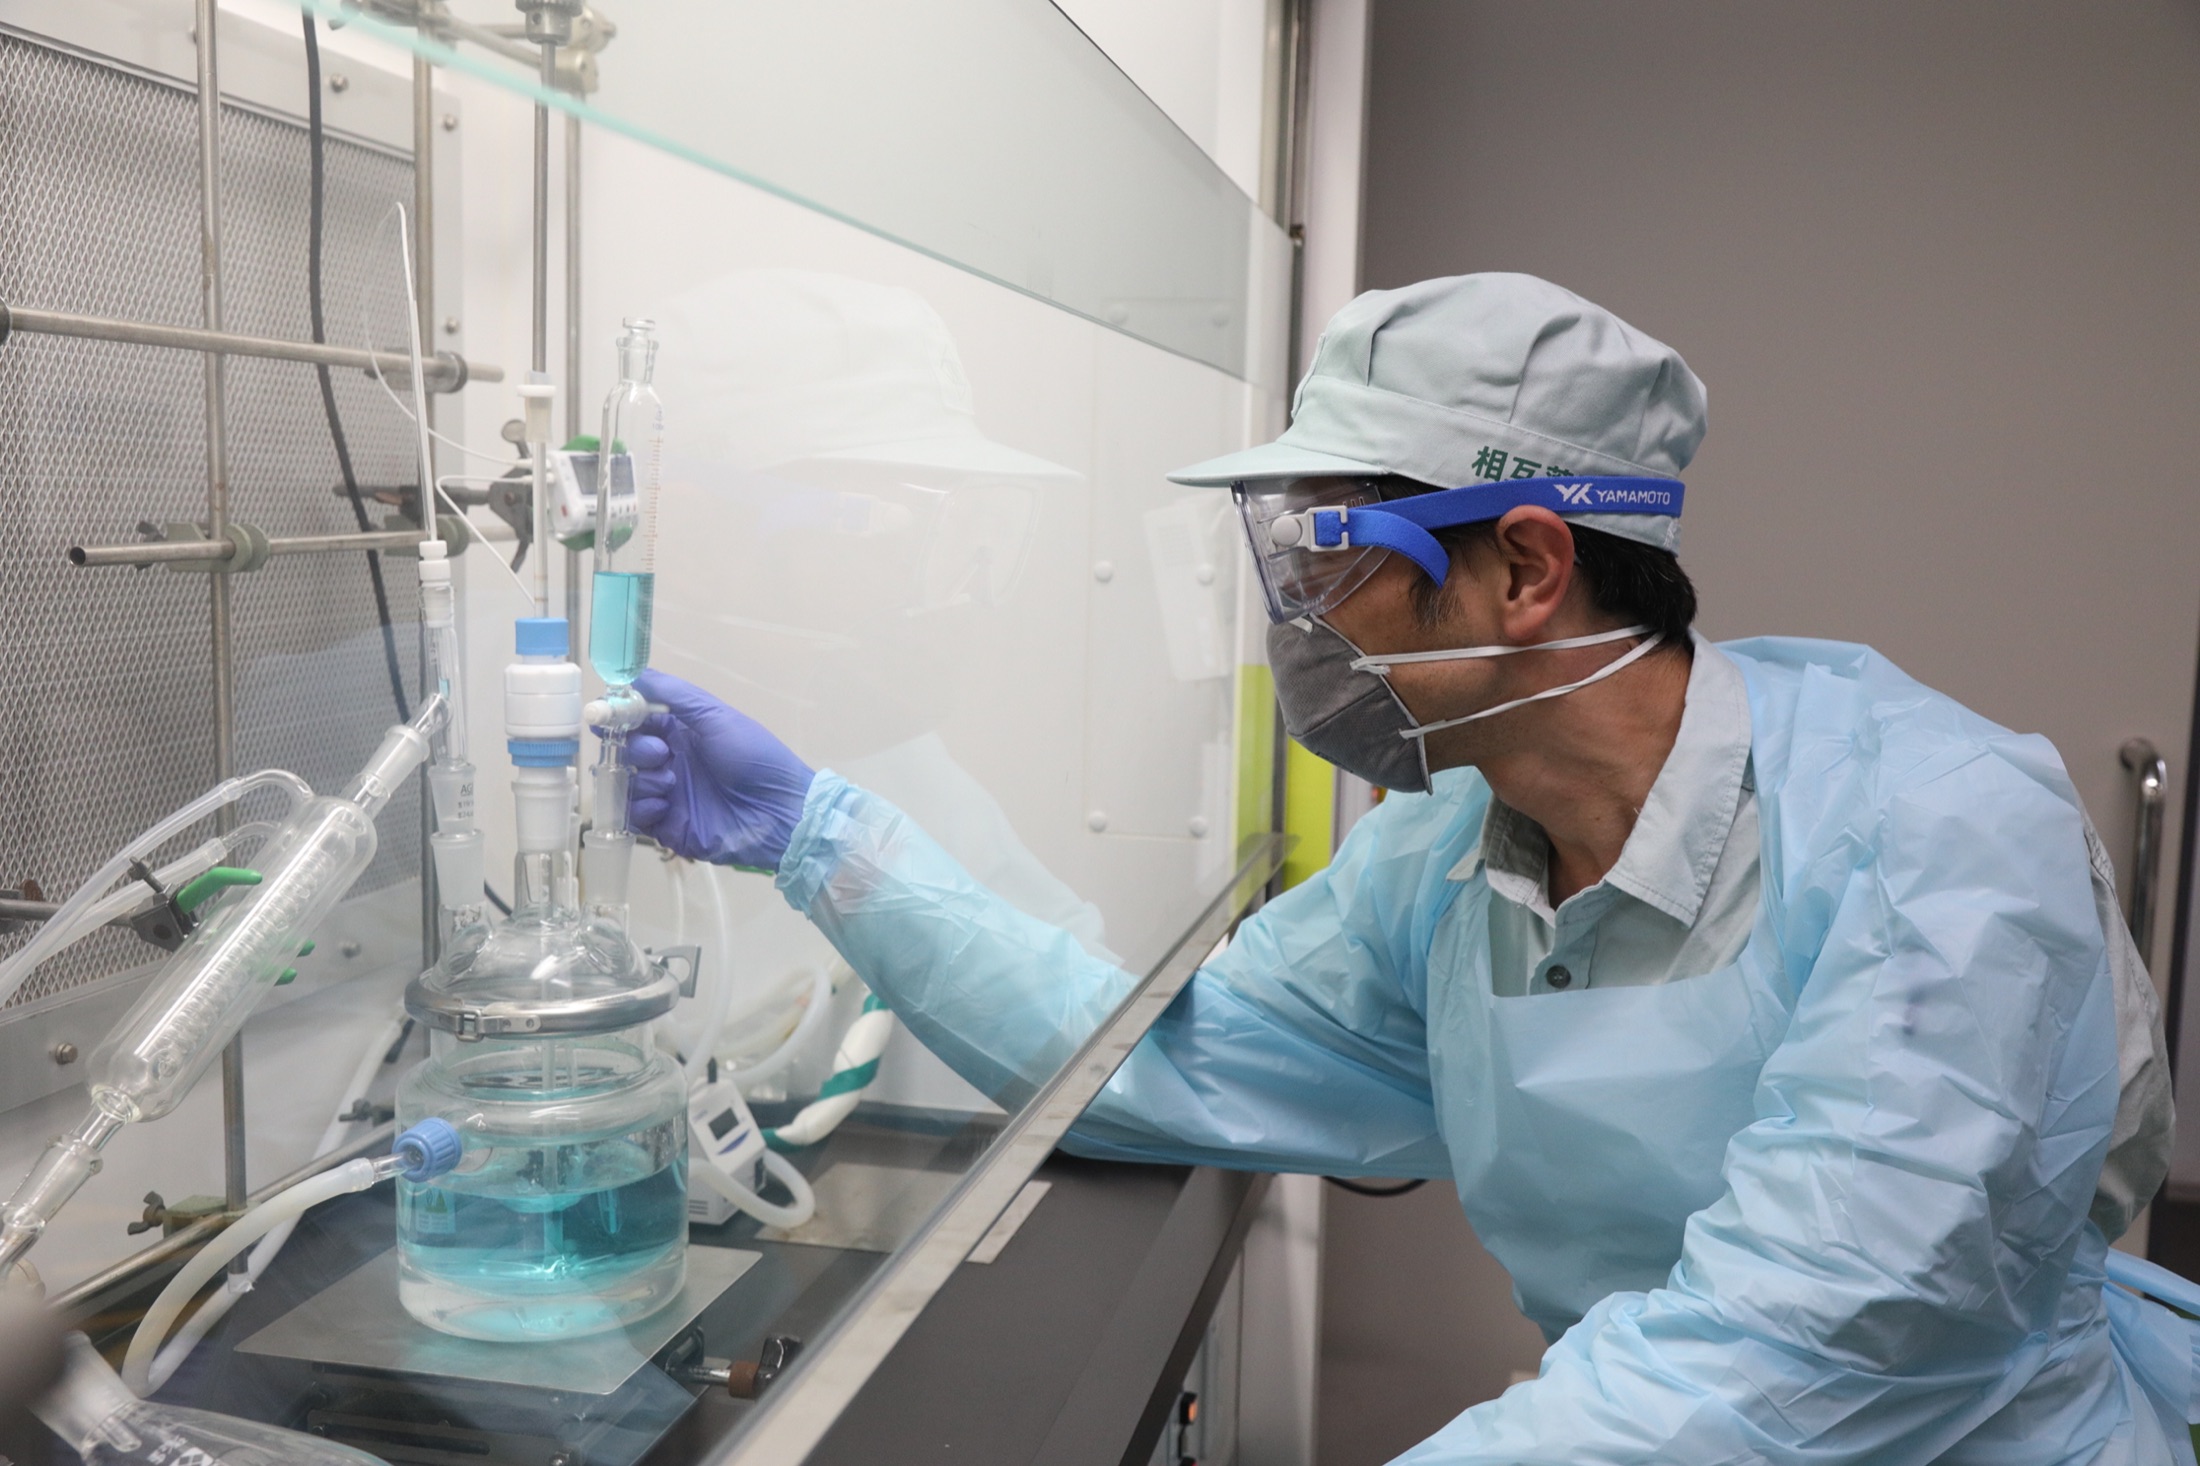
We proactively work on research and development work dealing with new fields and themes without being bound to existing frameworks of technology. We leverage our capabilities in terms of synthesis technologies to create new value.
Our history since we were founded
0years
Number of employees
0people
Capital
0million yen
Business locations
0locations
Sogo Pharmaceutical’s company profile, including an outline and history of our company and the contents of our business, is hereby presented.
Various examples of process and quality improvements as well as other initiatives that are being undertaken by us are hereby introduced.
Quality is built into the process. We deliver products that can be confidently used by clients thanks to a cGMP-based system of manufacturing and quality control.
In order to reliably supply products that satisfy our clients’ quality demands and regulatory requirements, we carry out quality-assurance activities in accordance with a ministerial ordinance on GMP and other statutory and regulatory requirements. A culture of quality is cultivated by ensuring data integrity and proper manpower training in the pursuit of trusted manufacturing.
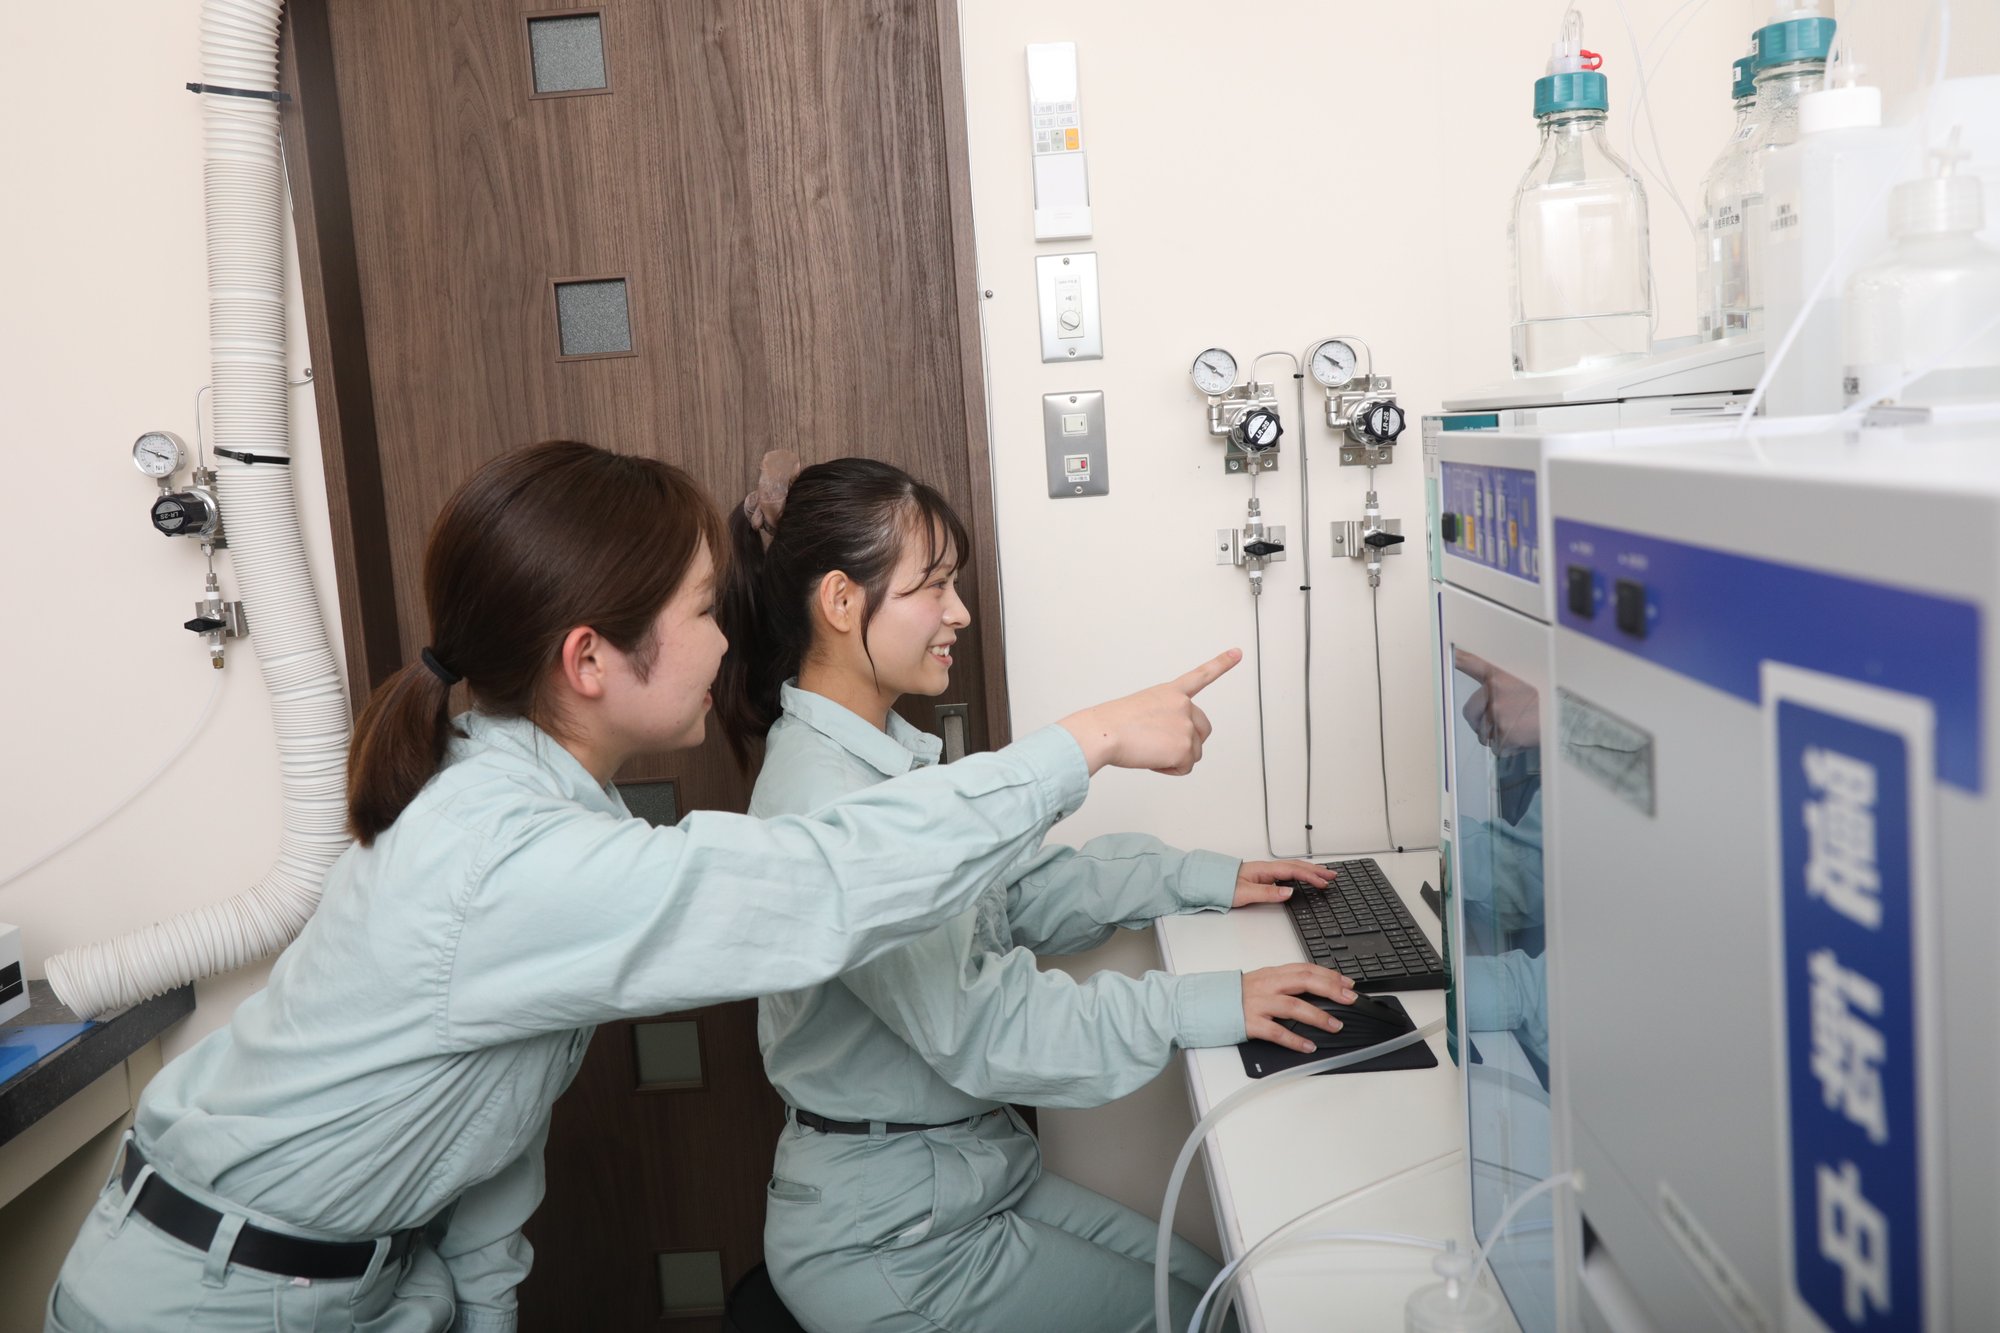
We reliably supply high-quality products that can be employed by clients with peace of mind by rigidly maintaining control over product quality with the use of properly developed analytical facilities and advanced analytical techniques.
Manufacture of active pharmaceutical ingredients (including steroid active pharmaceutical ingredients), pharmaceutical intermediates, active pharmaceutical ingredients for clinical trials, and more.
FIELD 02Manufacture of chemicals, including electronic materials, semiconductor materials, and specialty chemicals.
FIELD 03Manufacture of ingredients for one-of-a-kind skin brightening and antioxidant cosmetics.
Feel free to contact us to inquire about contract manufacturing and products.
+81-3-6273-4621
Ever since the founding of the company in 1955, we have been working on manufacturing active pharmaceutical ingredients, pharmaceutical intermediates, functional cosmetic ingredients, advanced chemicals, and more by harnessing the technology and experience that we have cultivated in the field of Pharmaceuticals.
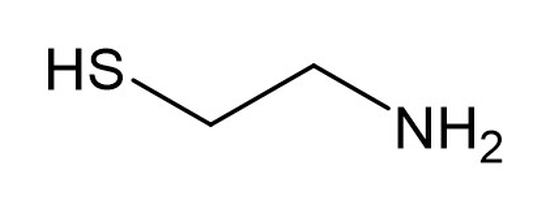
Cysteamine
Chemical nameMercaptoethylamine
CAS No.60-23-1
ApplicationsPharmaceutical intermediates, cosmetics, additives
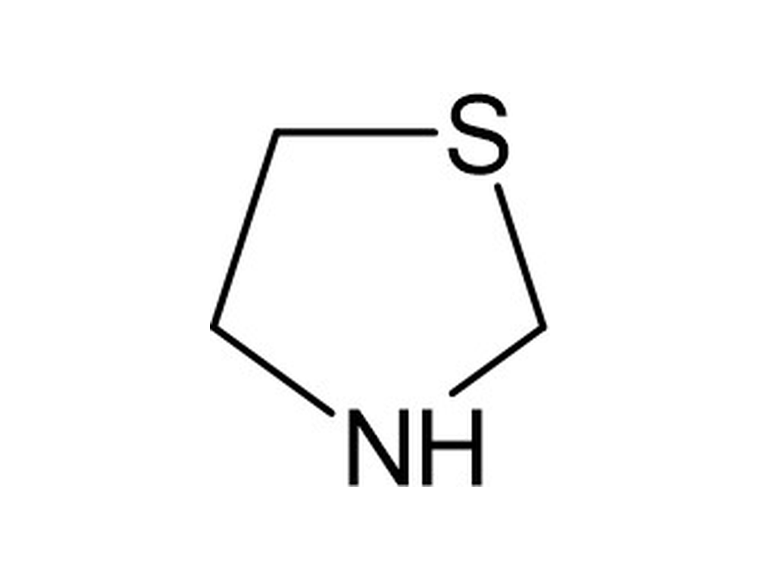
Thiazolidine
Chemical name1,3-Thiazolidine
CAS No.504-78-9
ApplicationsPharmaceutical intermediates
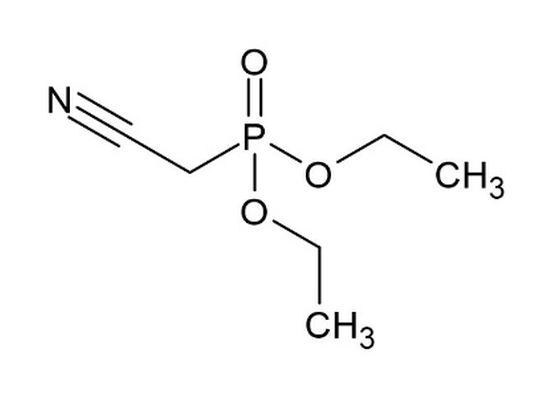
ZWT-03
Chemical nameDiethyl cyanomethylphosphonate
CAS No.2537-48-6
ApplicationsPharmaceutical intermediates
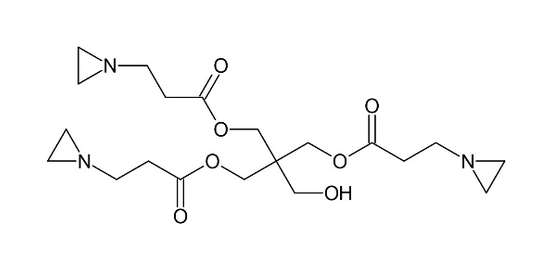
CROSSLINKER CL-427
Chemical name2-[[3-(1-Aziridinyl)-1-oxopropoxy]methyl]-2-(hydroxymethyl)-1,3-propanediyl bis(1-aziridinepropanoate)
CAS No.57116-45-7
ApplicationsCrosslinking agent
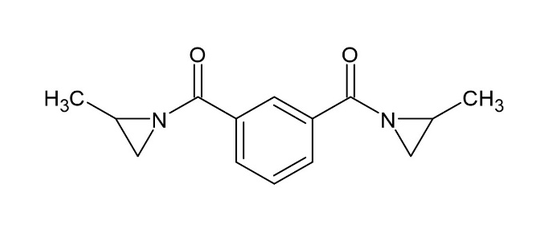
BIA
Chemical name1,1'-Isophthaloyl bis(2-methylaziridine)
CAS No.7652-64-4
ApplicationsCuring agent, binder
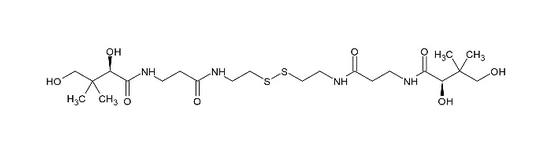
Pantethine
Chemical nameBis(2-{3-[(2R)-2,4-dihydroxy-3,3-dimethylbutanoylamino]-propanoylamino}ethyl) disulfide
CAS No.16816-67-4
ApplicationsCosmetics, additives
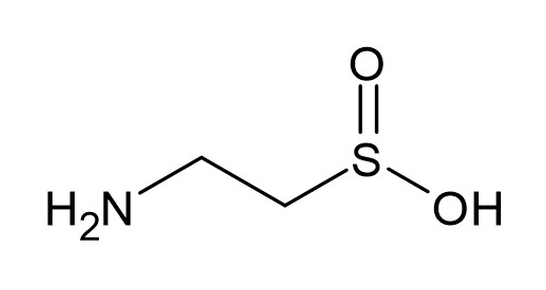
Hypotaurine
INCI nameAminoethanesulfinic acid
CAS No.300-84-5
ApplicationsAntioxidant (approved for quasi-drug use)
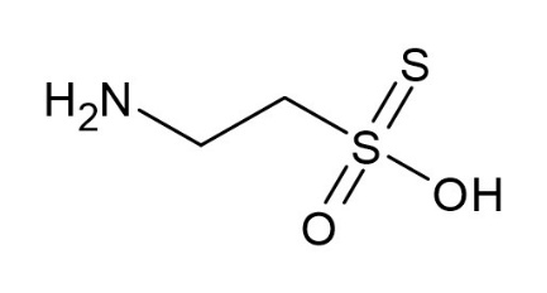
Thiotaurine
INCI nameSame as above
CAS No.2937-54-4
ApplicationsAntioxidant (approved for quasi-drug use)
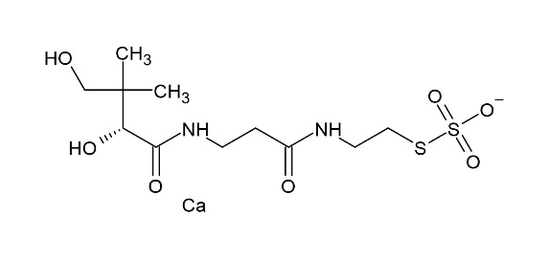
Calcium D-Pantetheine-S-sulfonate 70
INCI nameCalcium pantetheine sulfonate
CAS No.34644-00-3
ApplicationsSkin-brightening agent (approved for quasi-drug use)
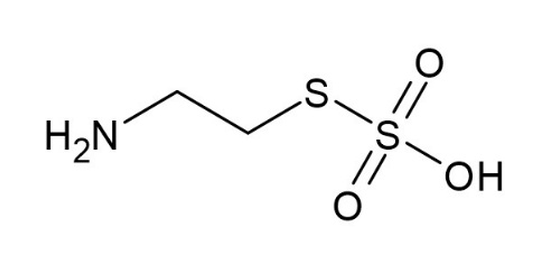
Bunte salt
Chemical nameS-(2-Aminoethyl) thiosulfuric acid
CAS No.2937-53-3
ApplicationsCosmetic intermediates
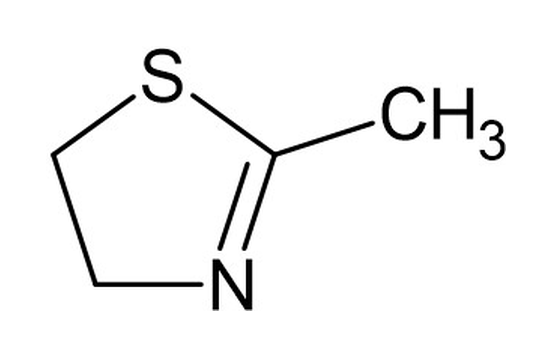
2MT
Chemical name2-Methyl-2-thiazoline
CAS No.2346-00-1
ApplicationsIntermediates
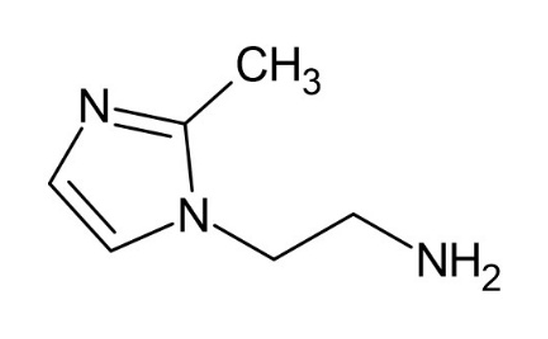
1AE2MI
Chemical name1-(2-Aminoethyl)-2-methyl-1H-imidazole
CAS No.113741-01-8
ApplicationsResin additives
We provide comprehensive support with an emphasis on collaborating with our clients on everything from the contract manufacturing of active pharmaceutical ingredients, pharmaceutical intermediates, and active pharmaceutical ingredients for clinical trials to research and development work on advanced chemicals, functional cosmetic ingredients and from laboratory-level investigations conducted during the early stages of development to the normalization of commercial production.
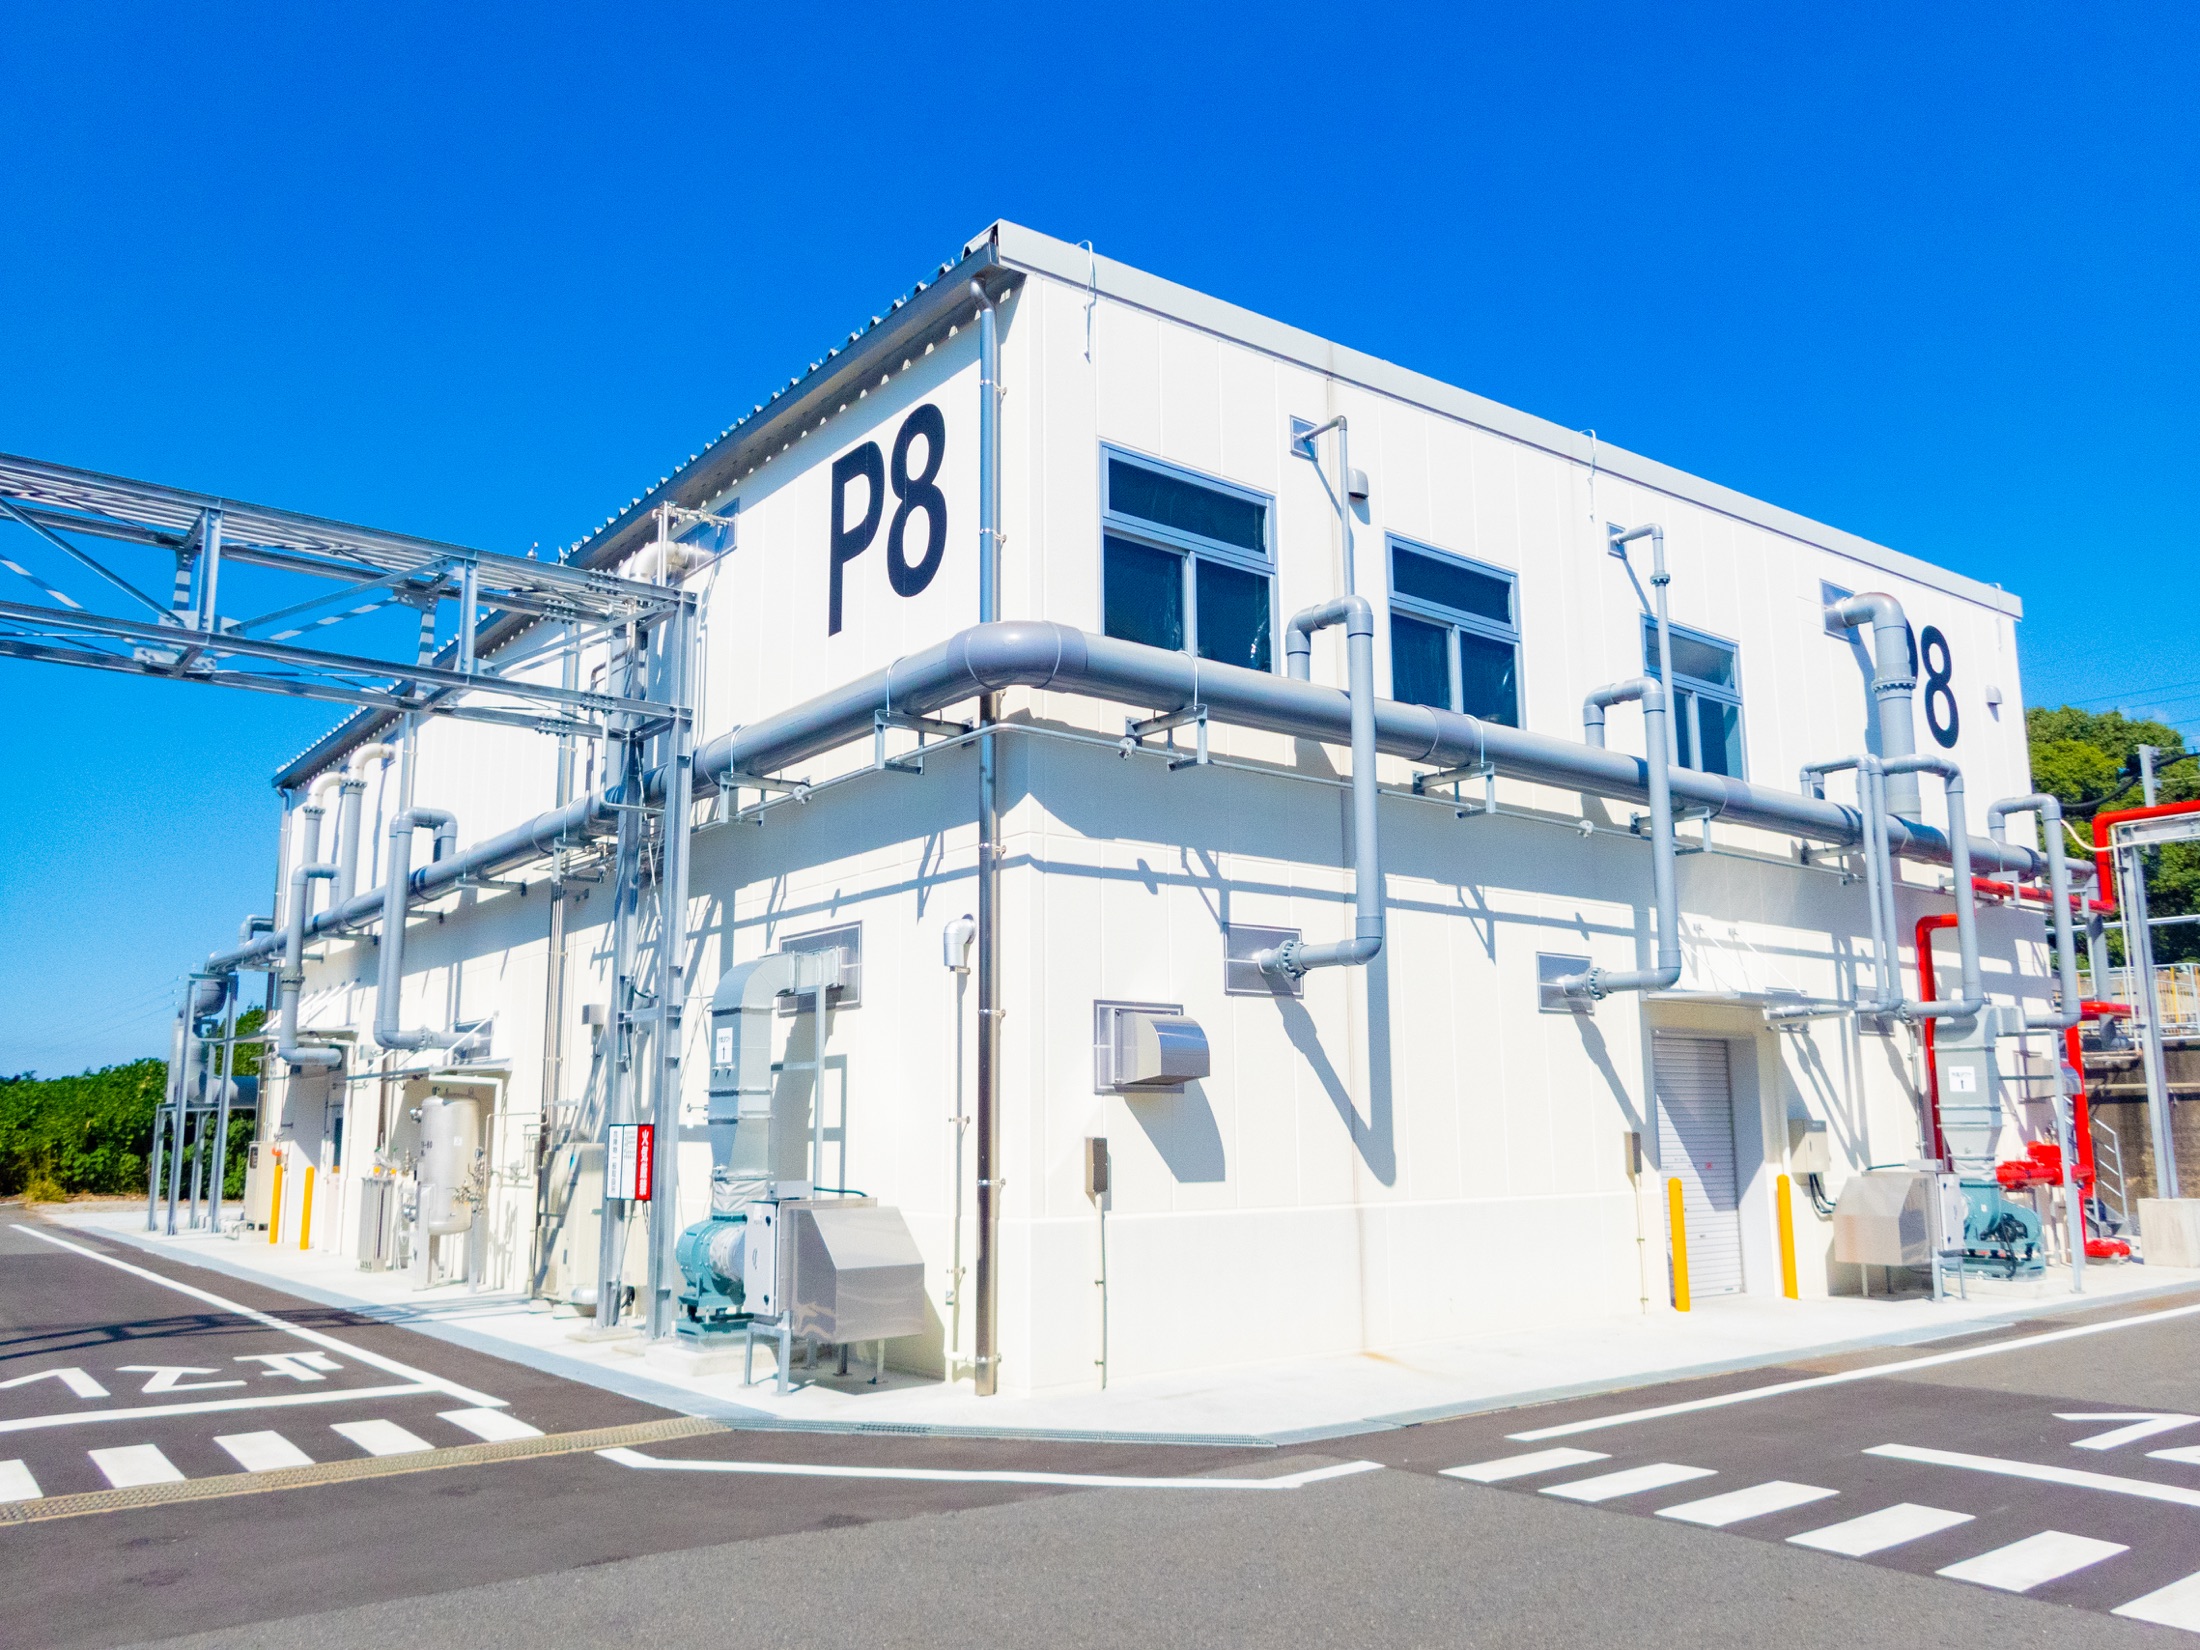
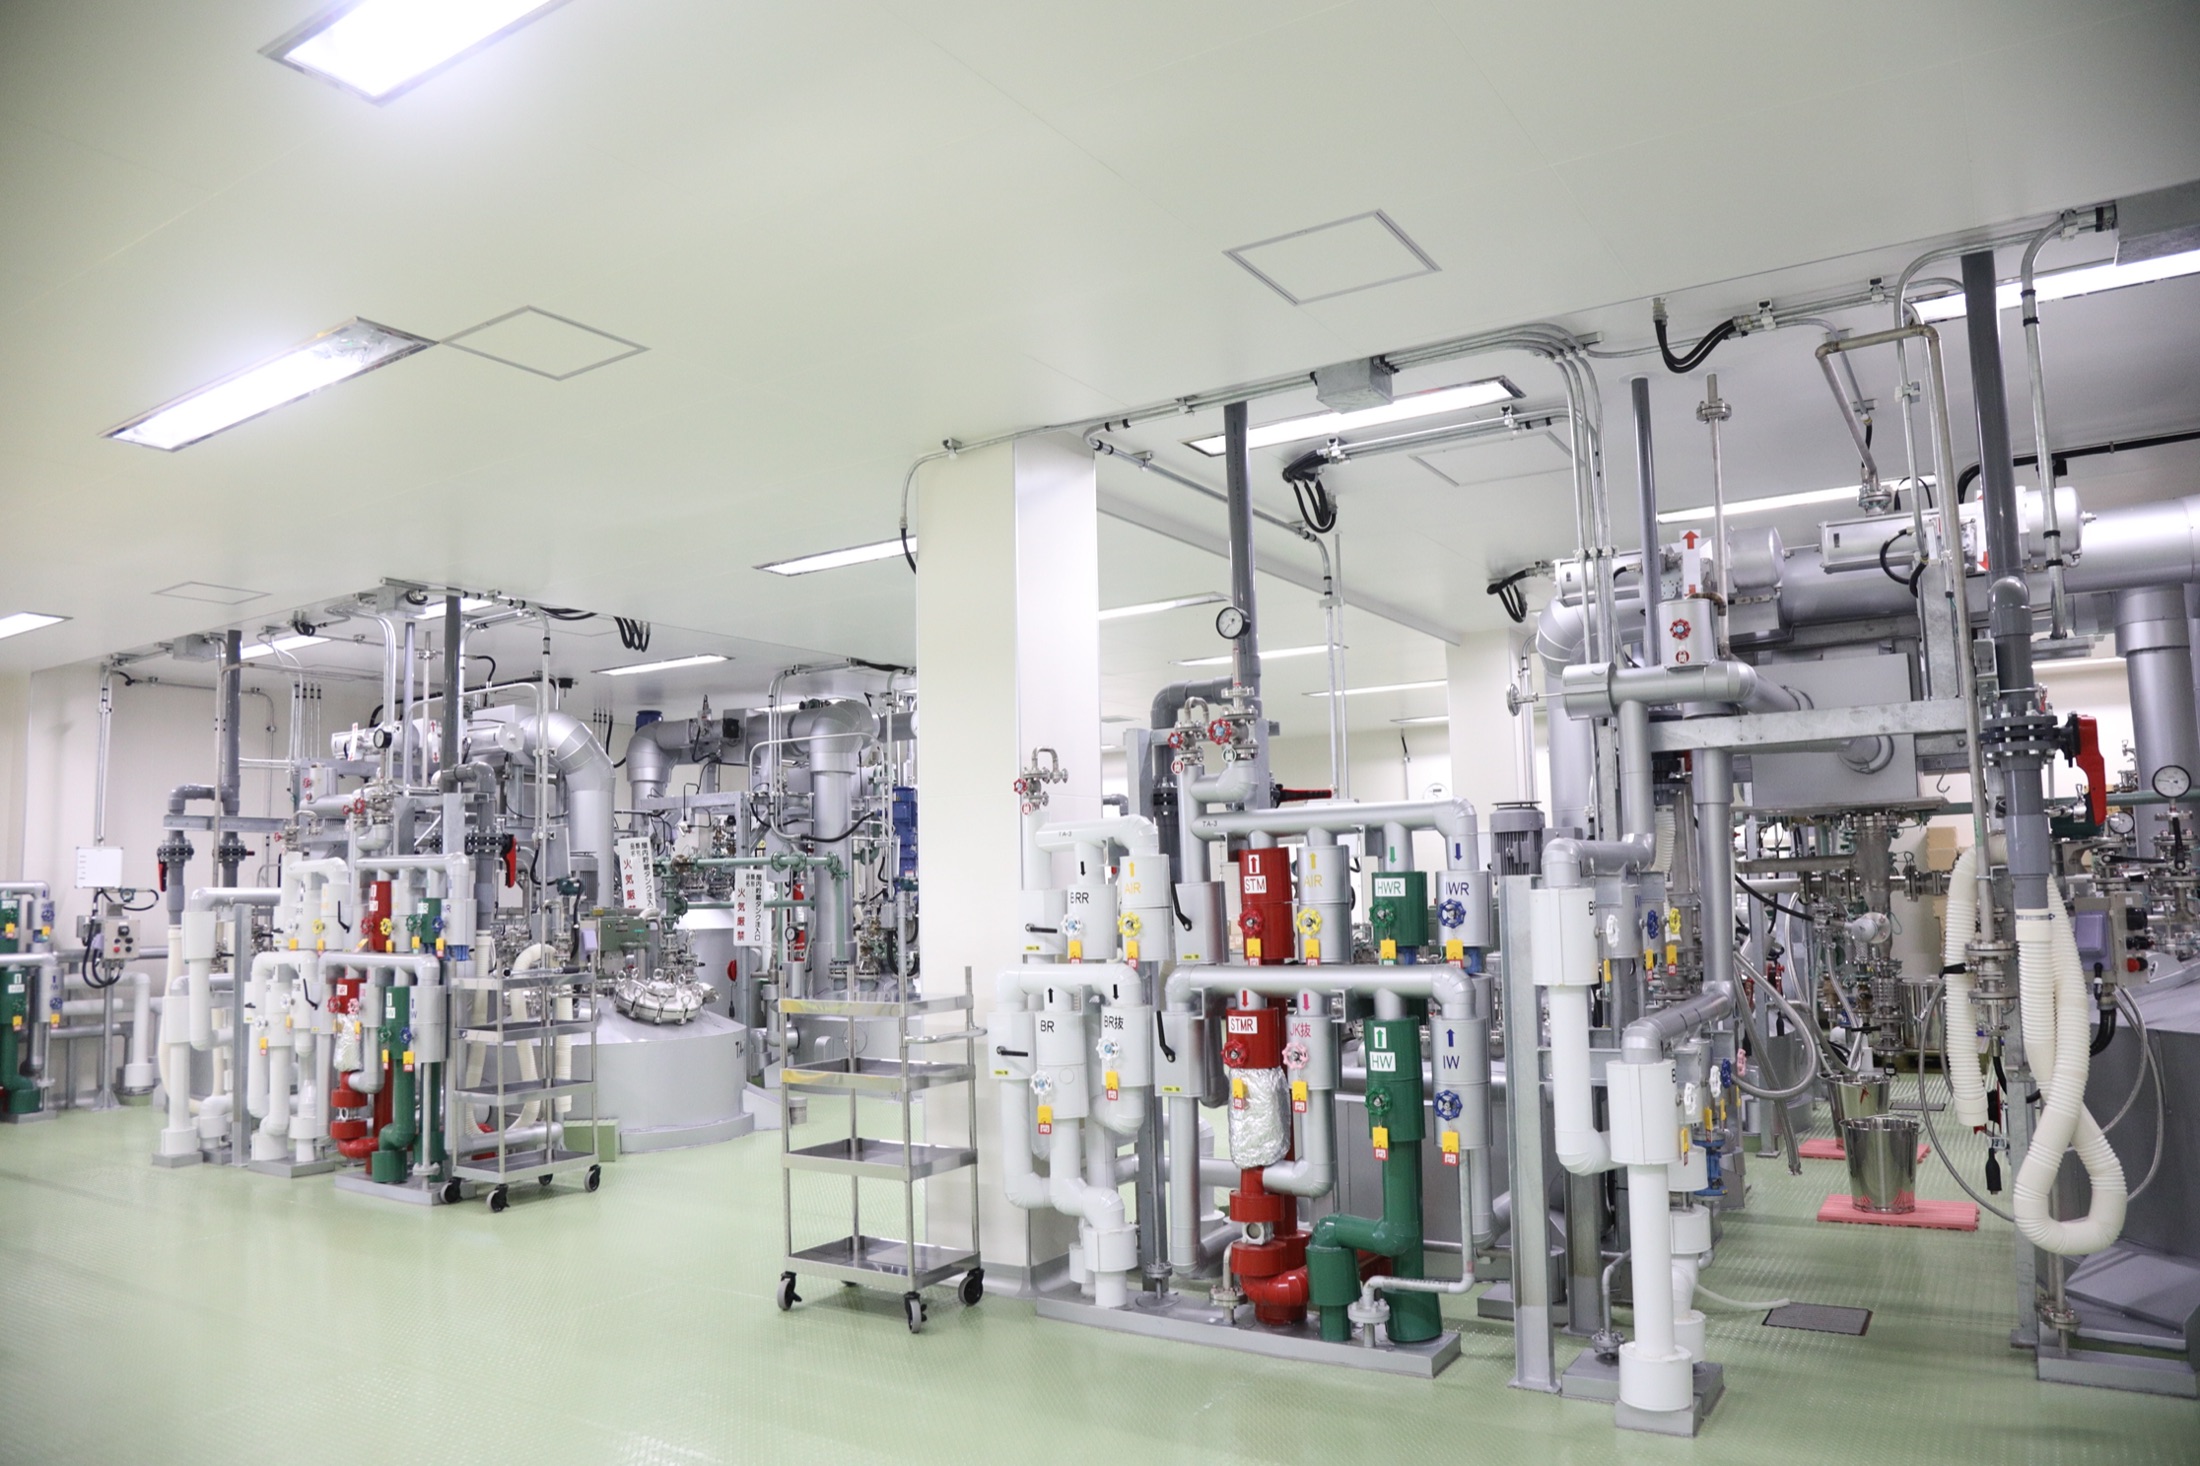
A wide range of reactors and analytical instruments, including our Fukuoka Factory Building No. 8 (P8), which is equipped with a Class 100,000 cleanroom, are hereby introduced.
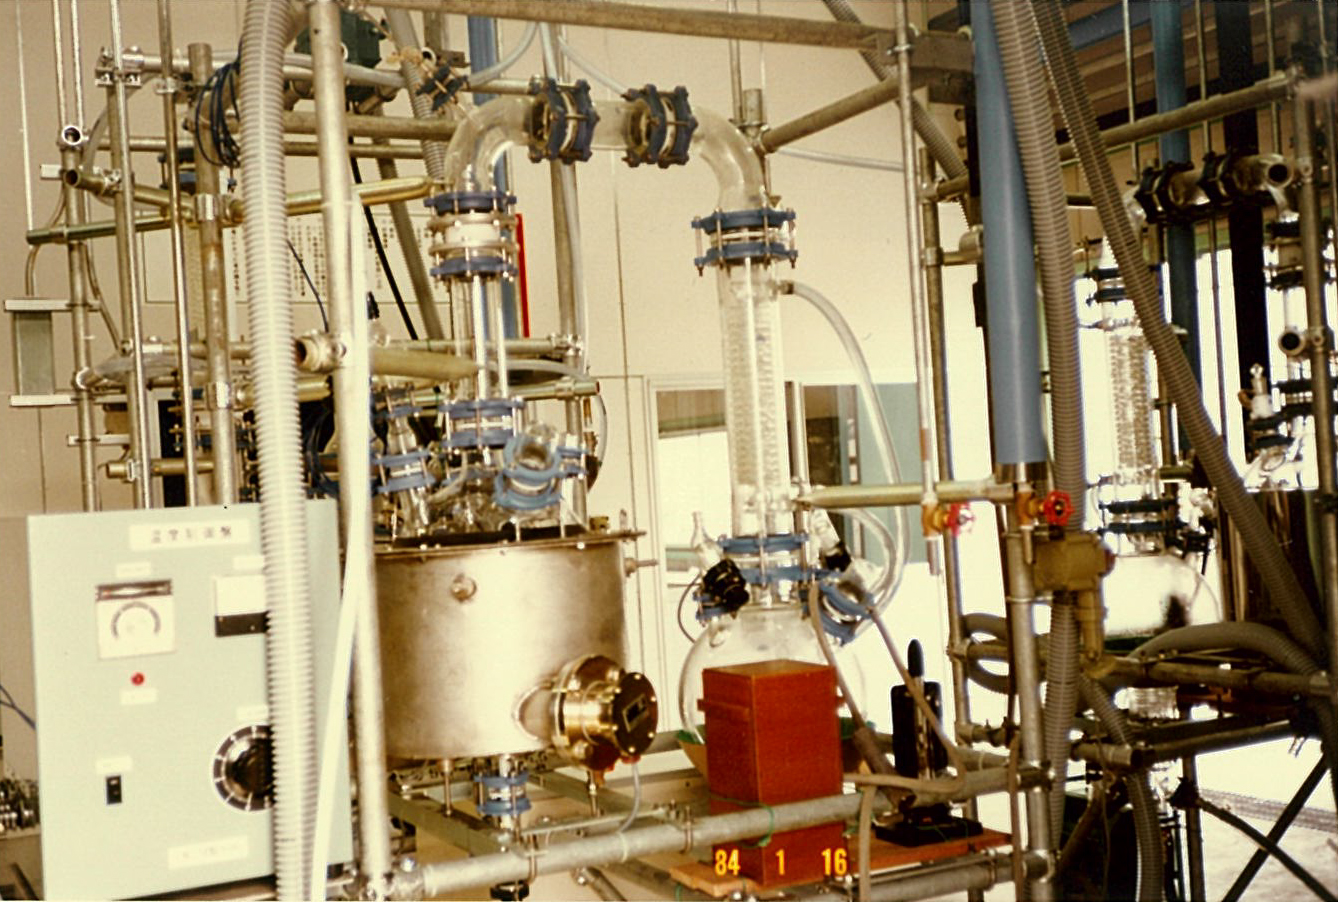
Specialized reaction technologies and advanced purification technologies corresponding to our areas of expertise, which are associated with photoreactions, low-temperature reactions, high-temperature reactions, and more, are hereby introduced.
Initiatives for engaging in research and development work on functional cosmetic ingredients and new themes are hereby introduced.
Reactions
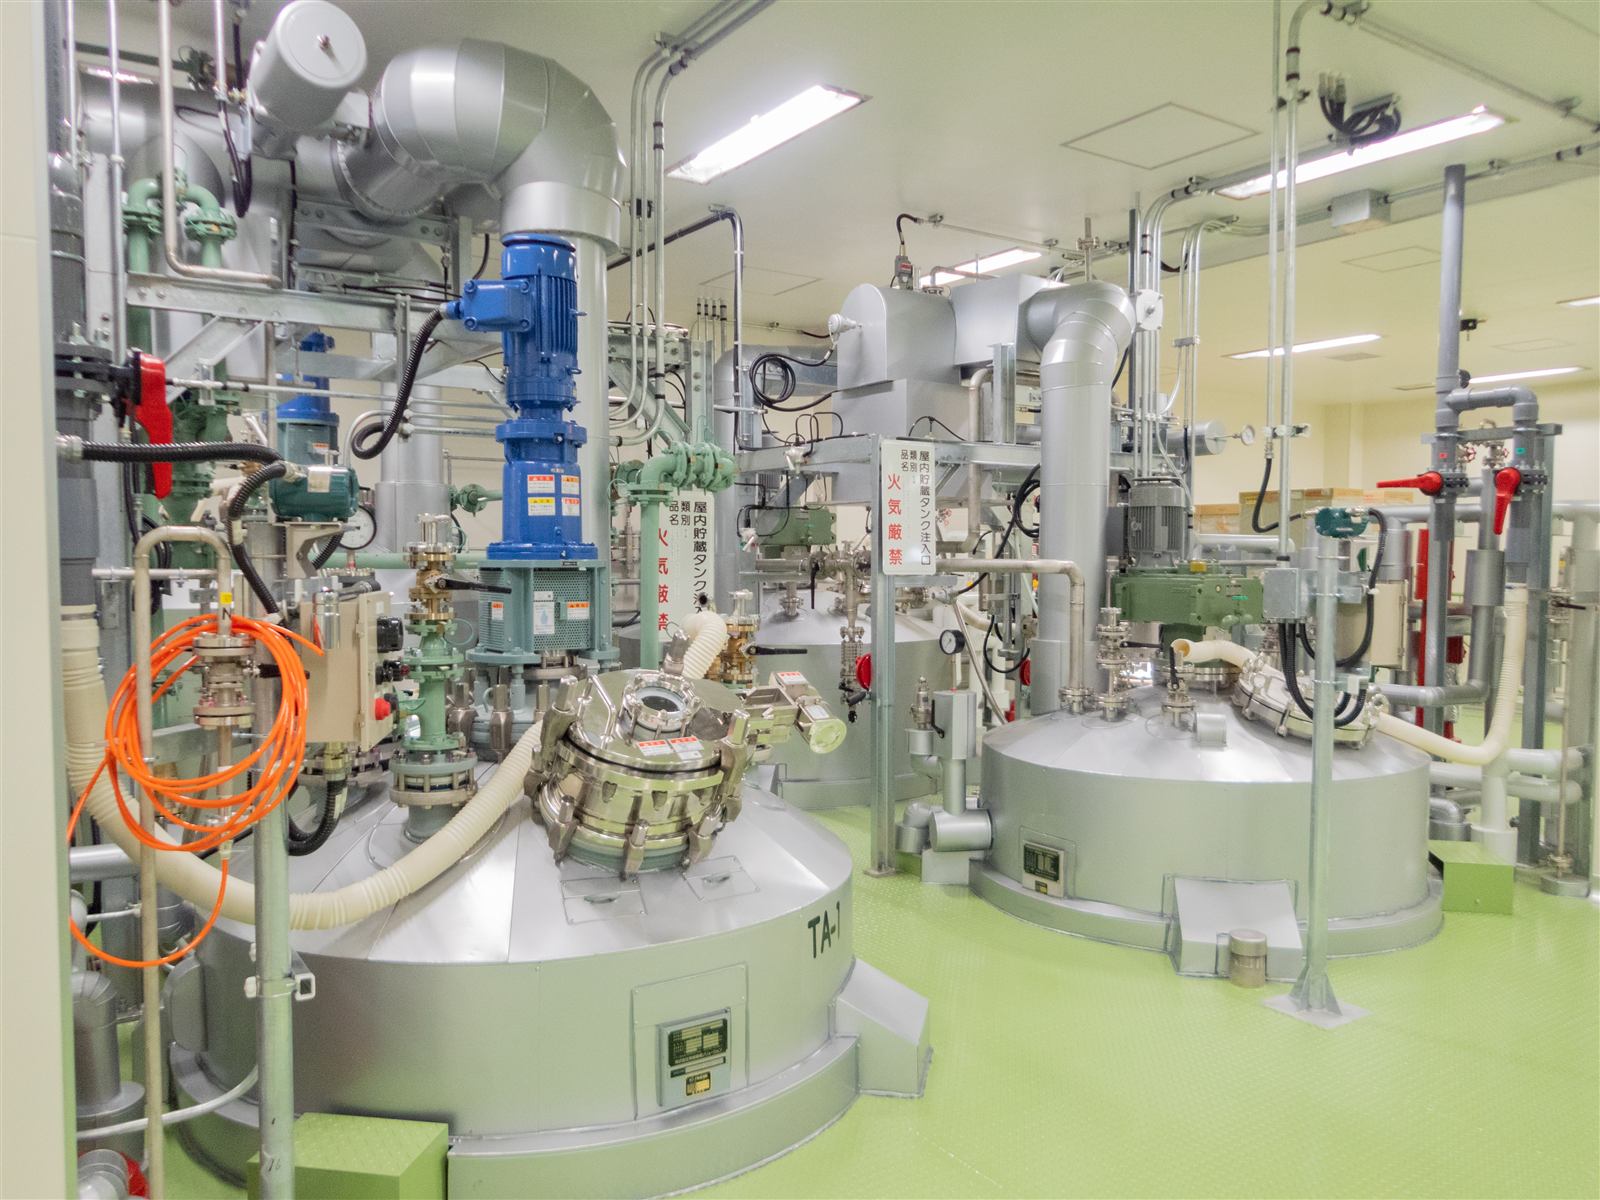
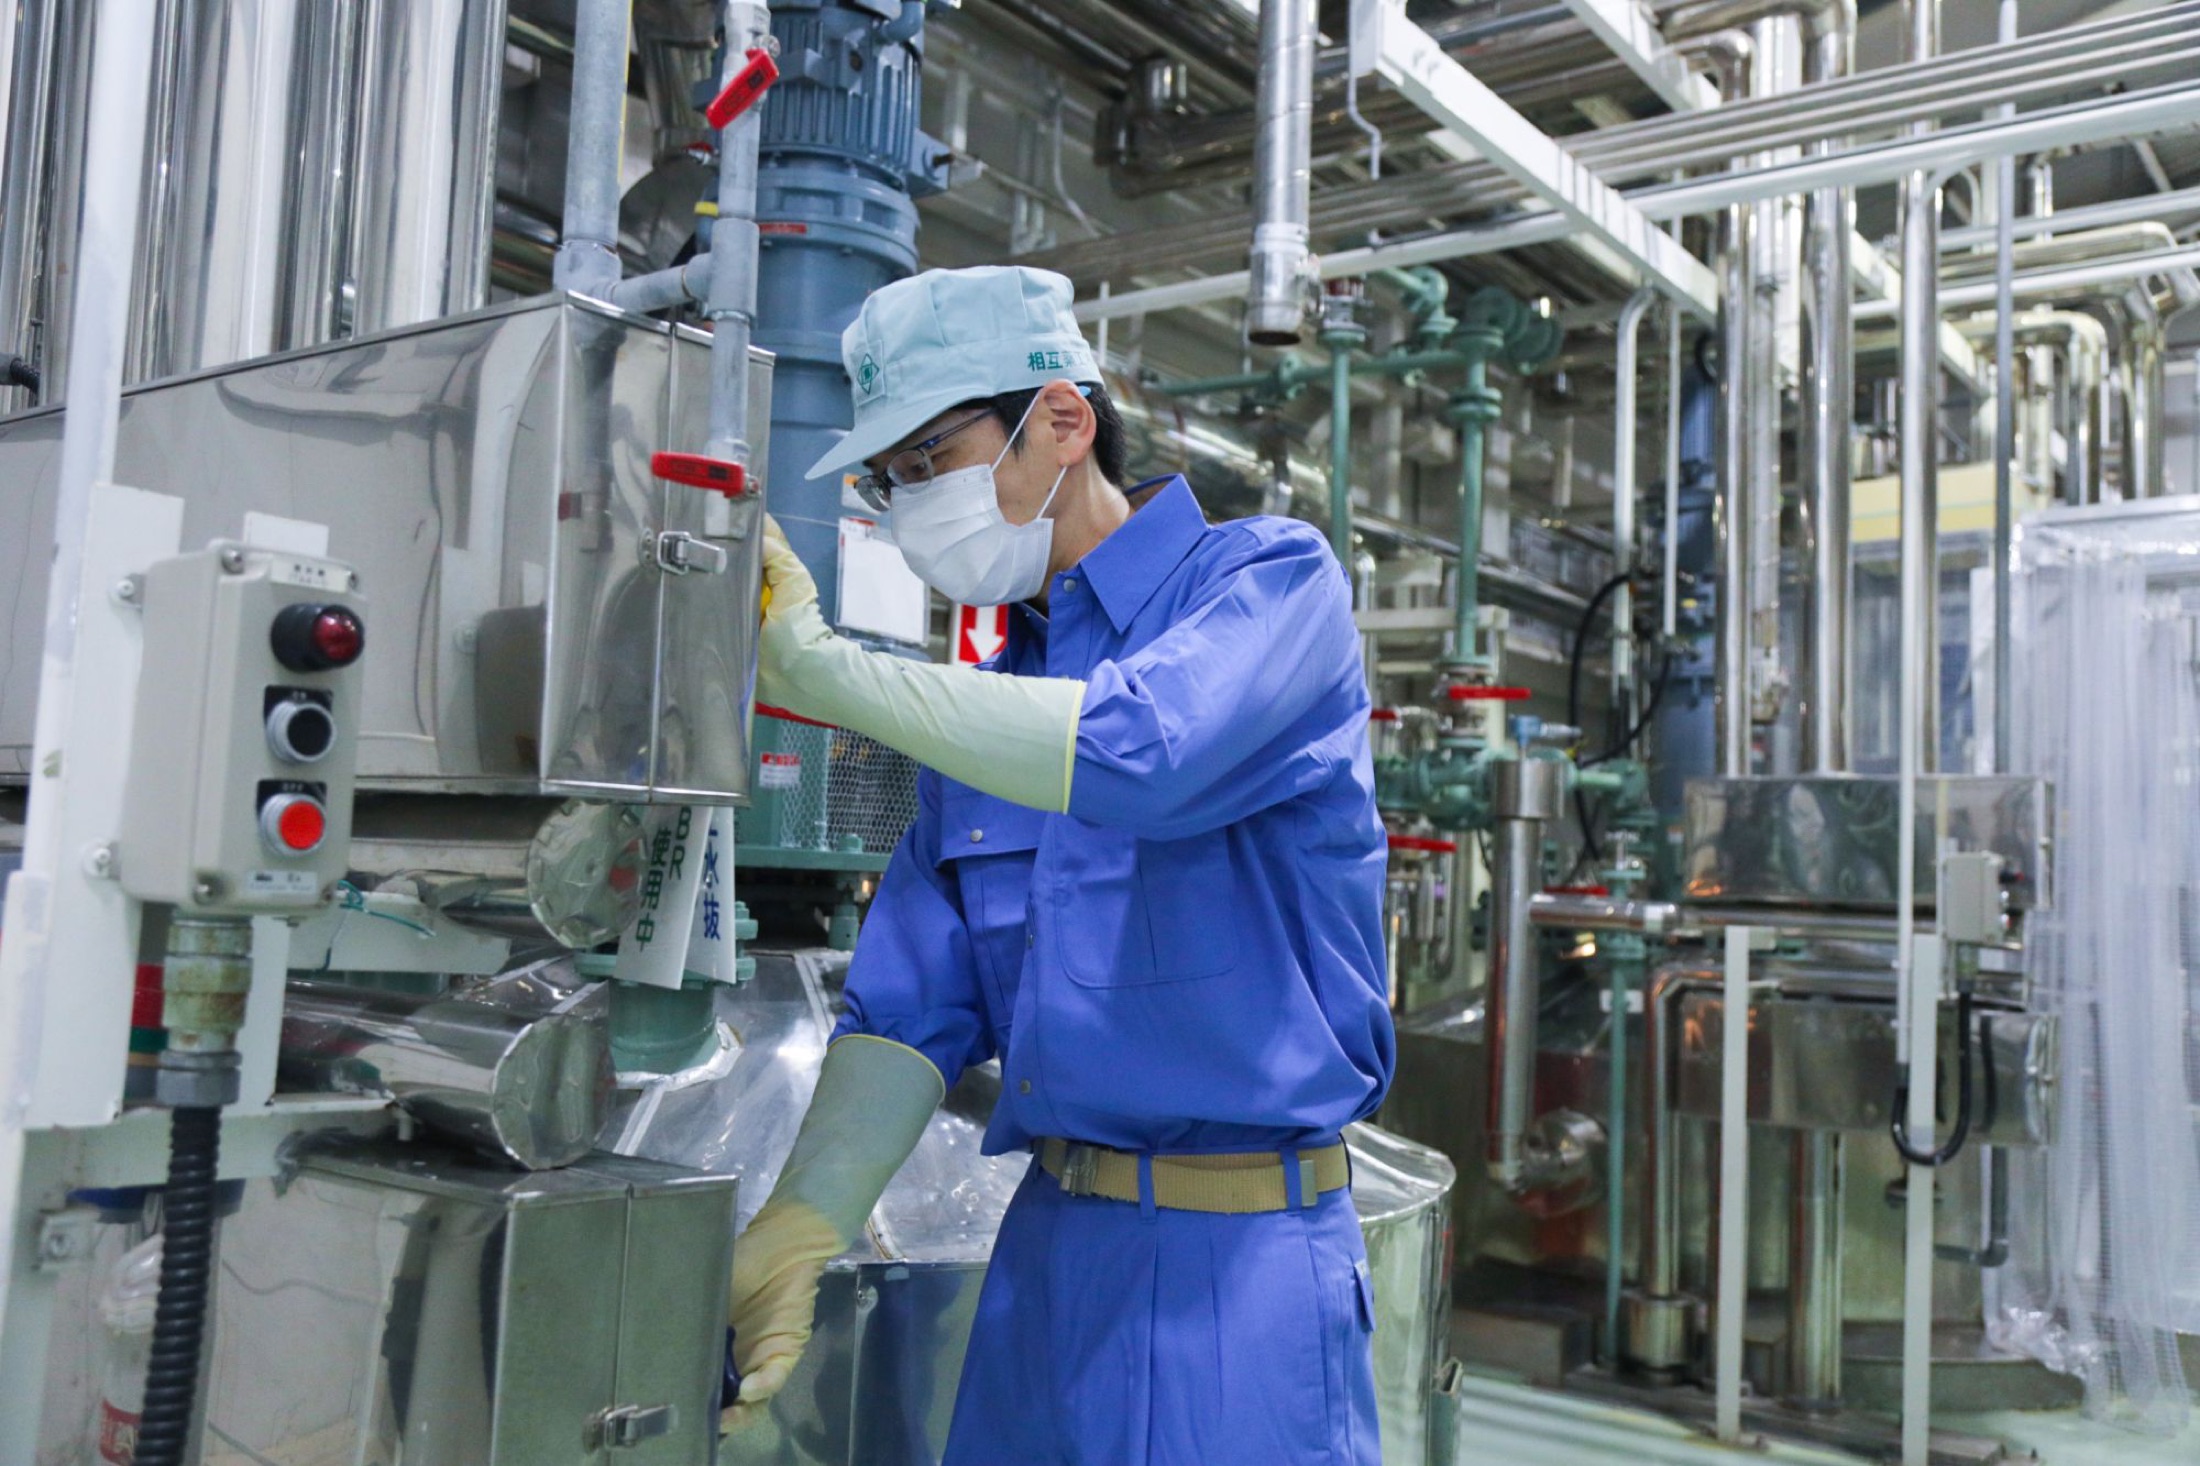
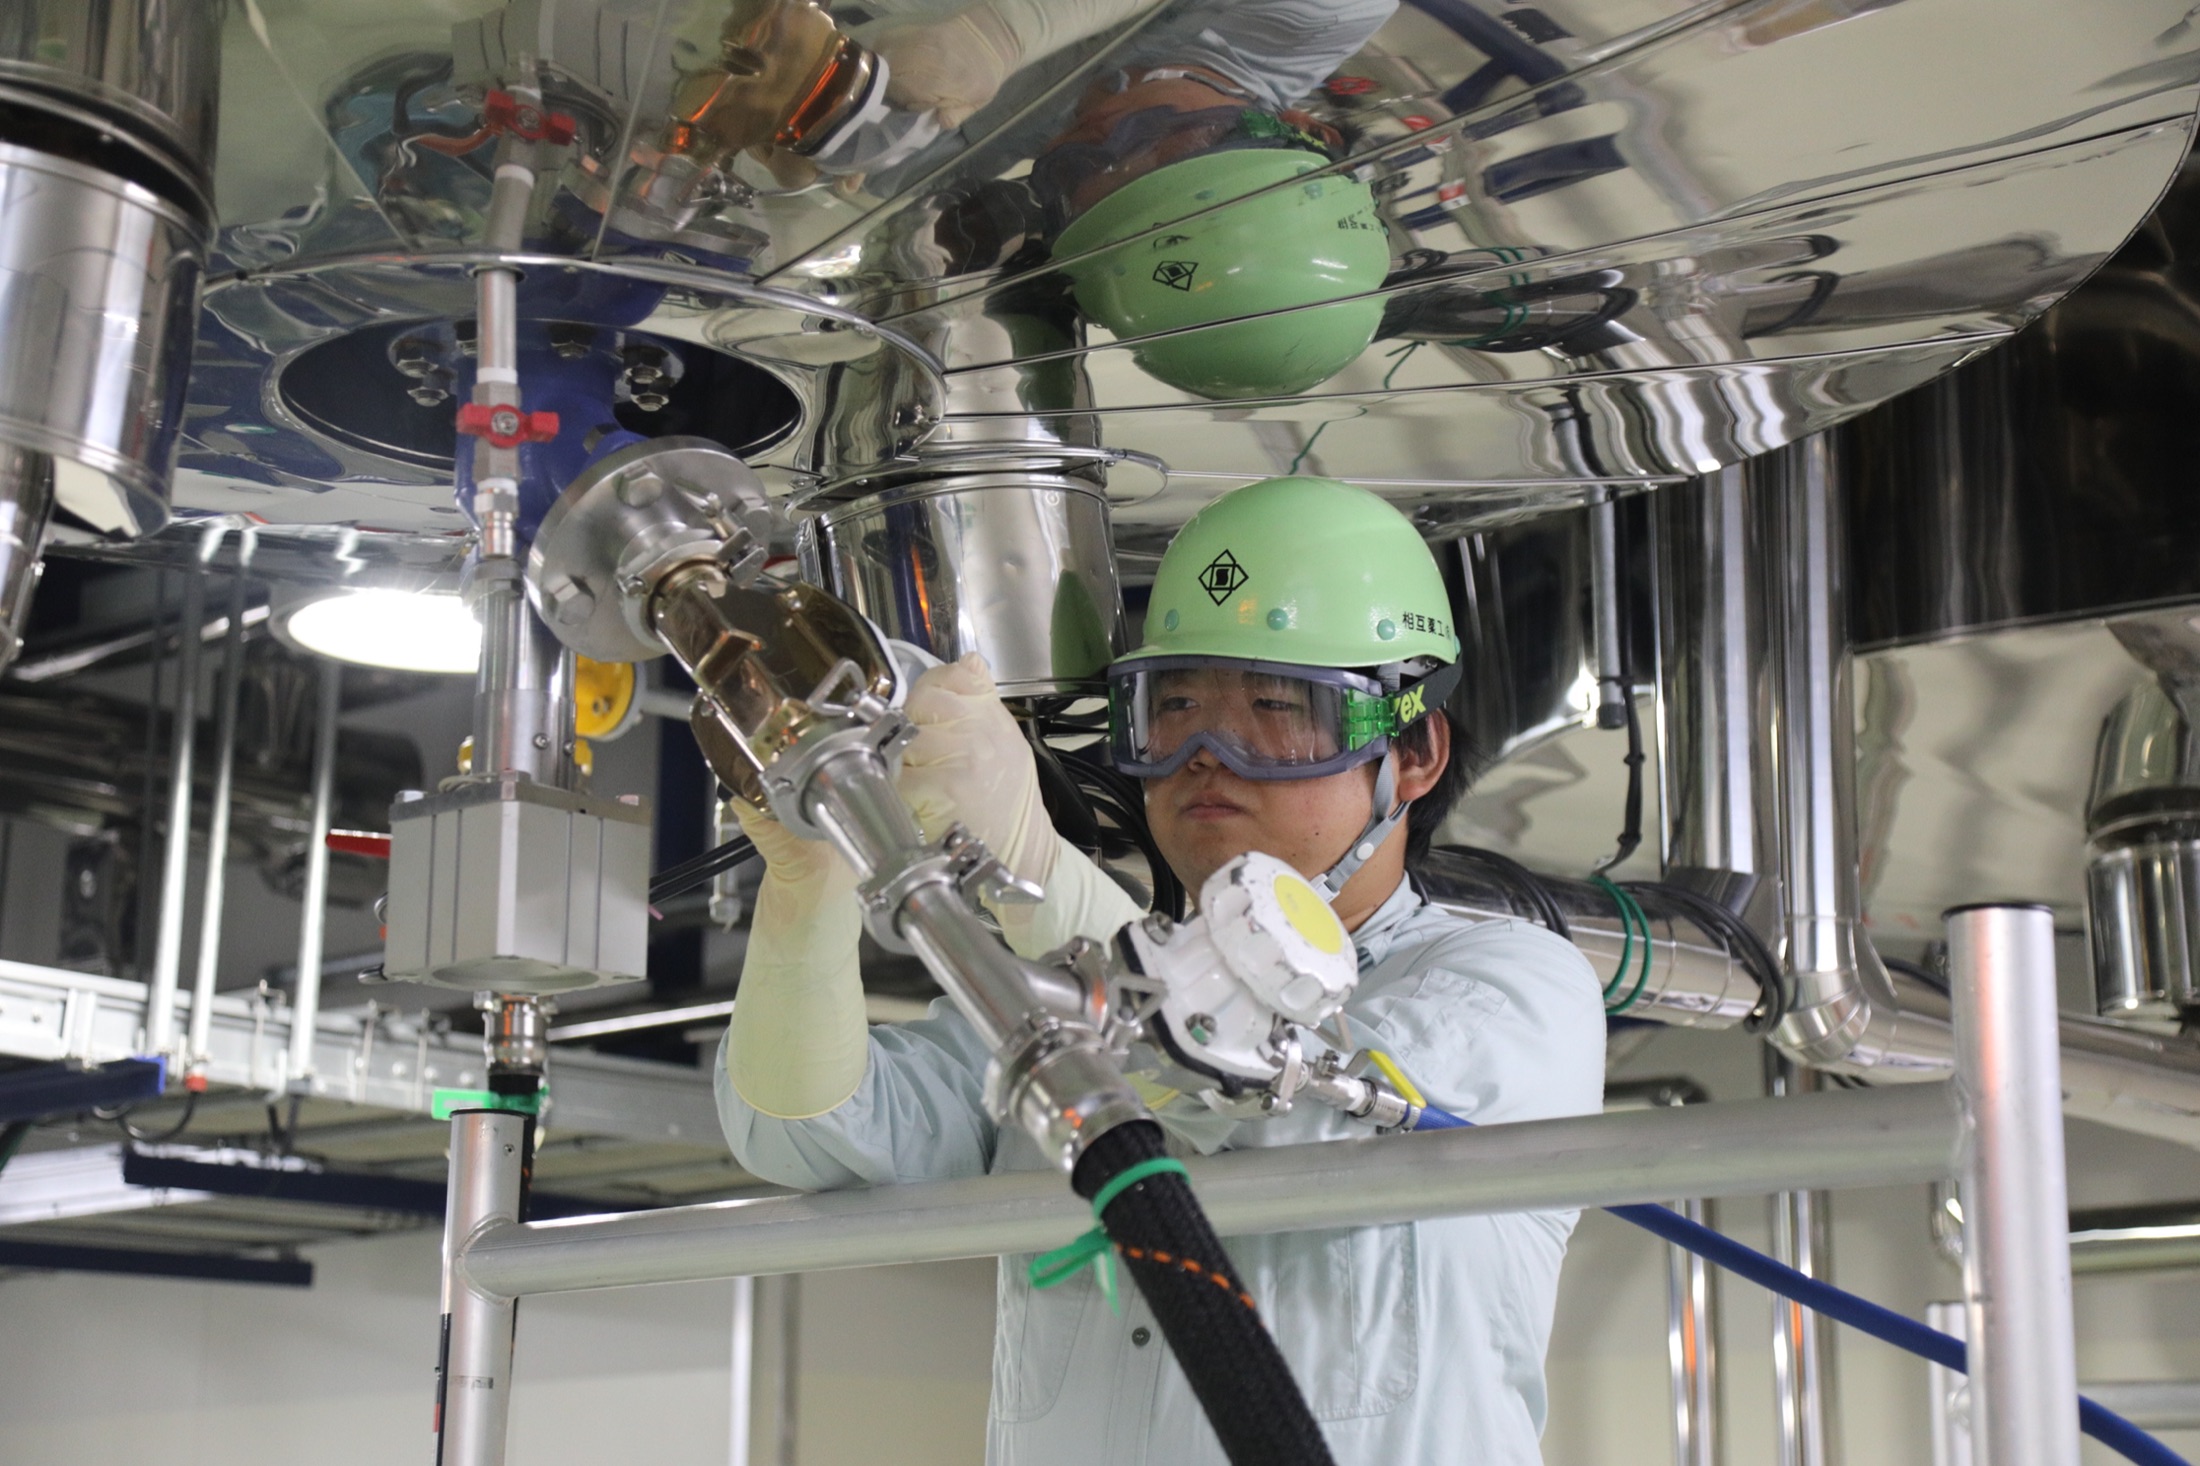
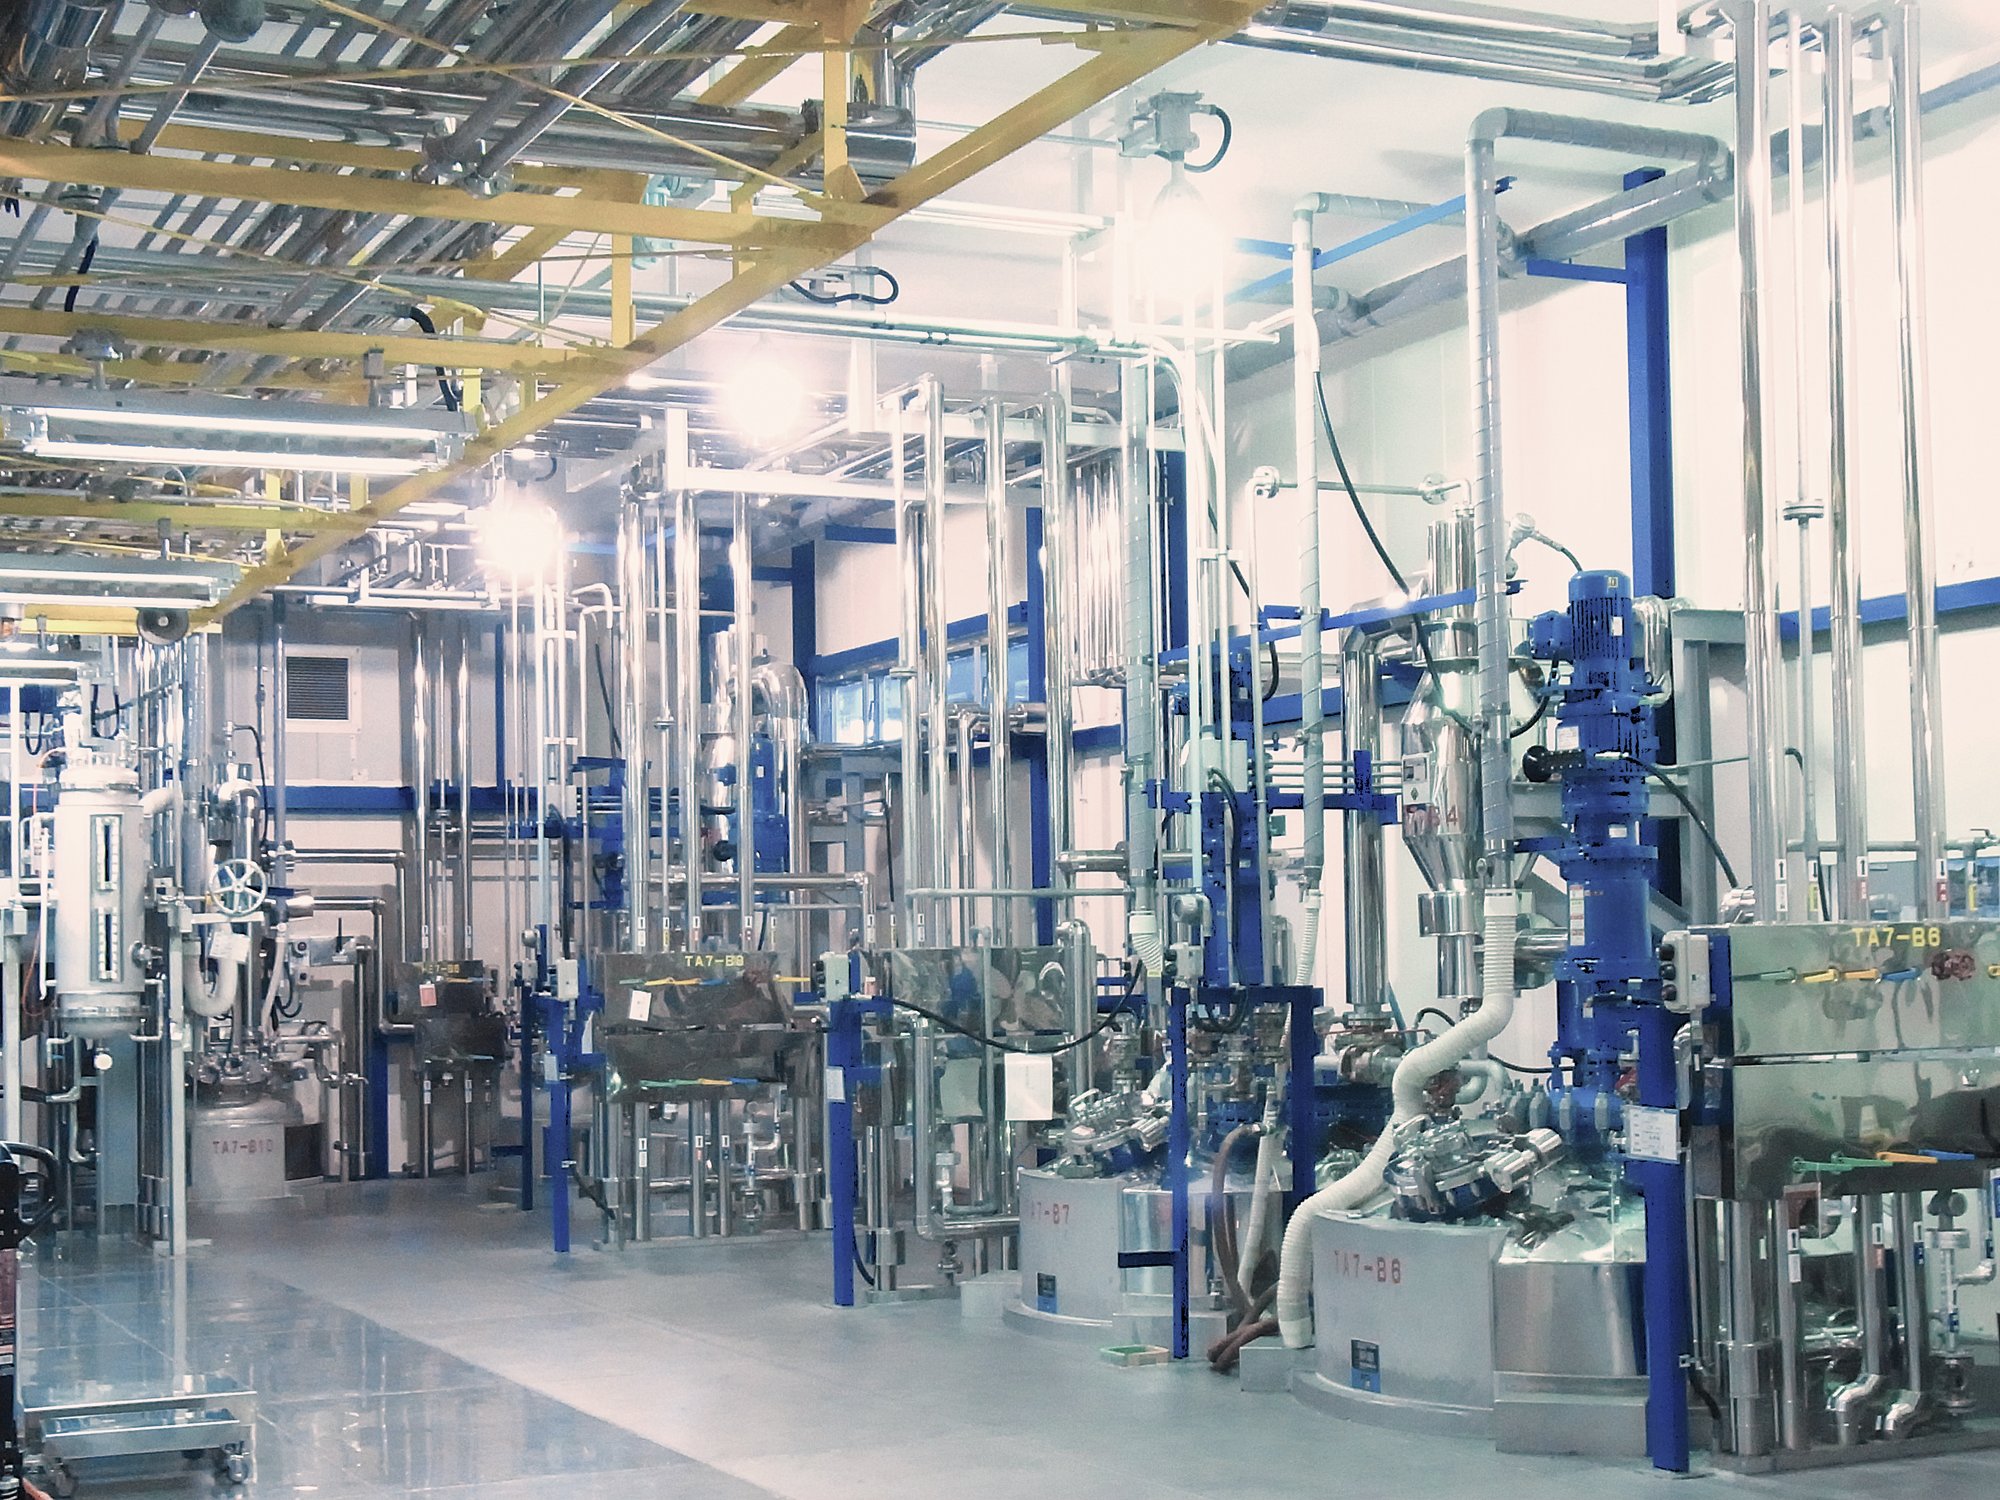
We possess many GL and SUS reactors ranging in size from 200 liters to 4,000 liters. These reactors are designed to accommodate any type of reaction in accordance with our basic concept of multi-purpose functionality.
Purification
We possess a large number of centrifuges (24 to 42 inches) that serve to separate solid particles for powered products, including stainless-steel models, as well as resin-coated units that are highly resistant to acids. We also have column purifiers, thin-film evaporators, various kinds of pressurized filters, and resin towers to remove ionic and other components.
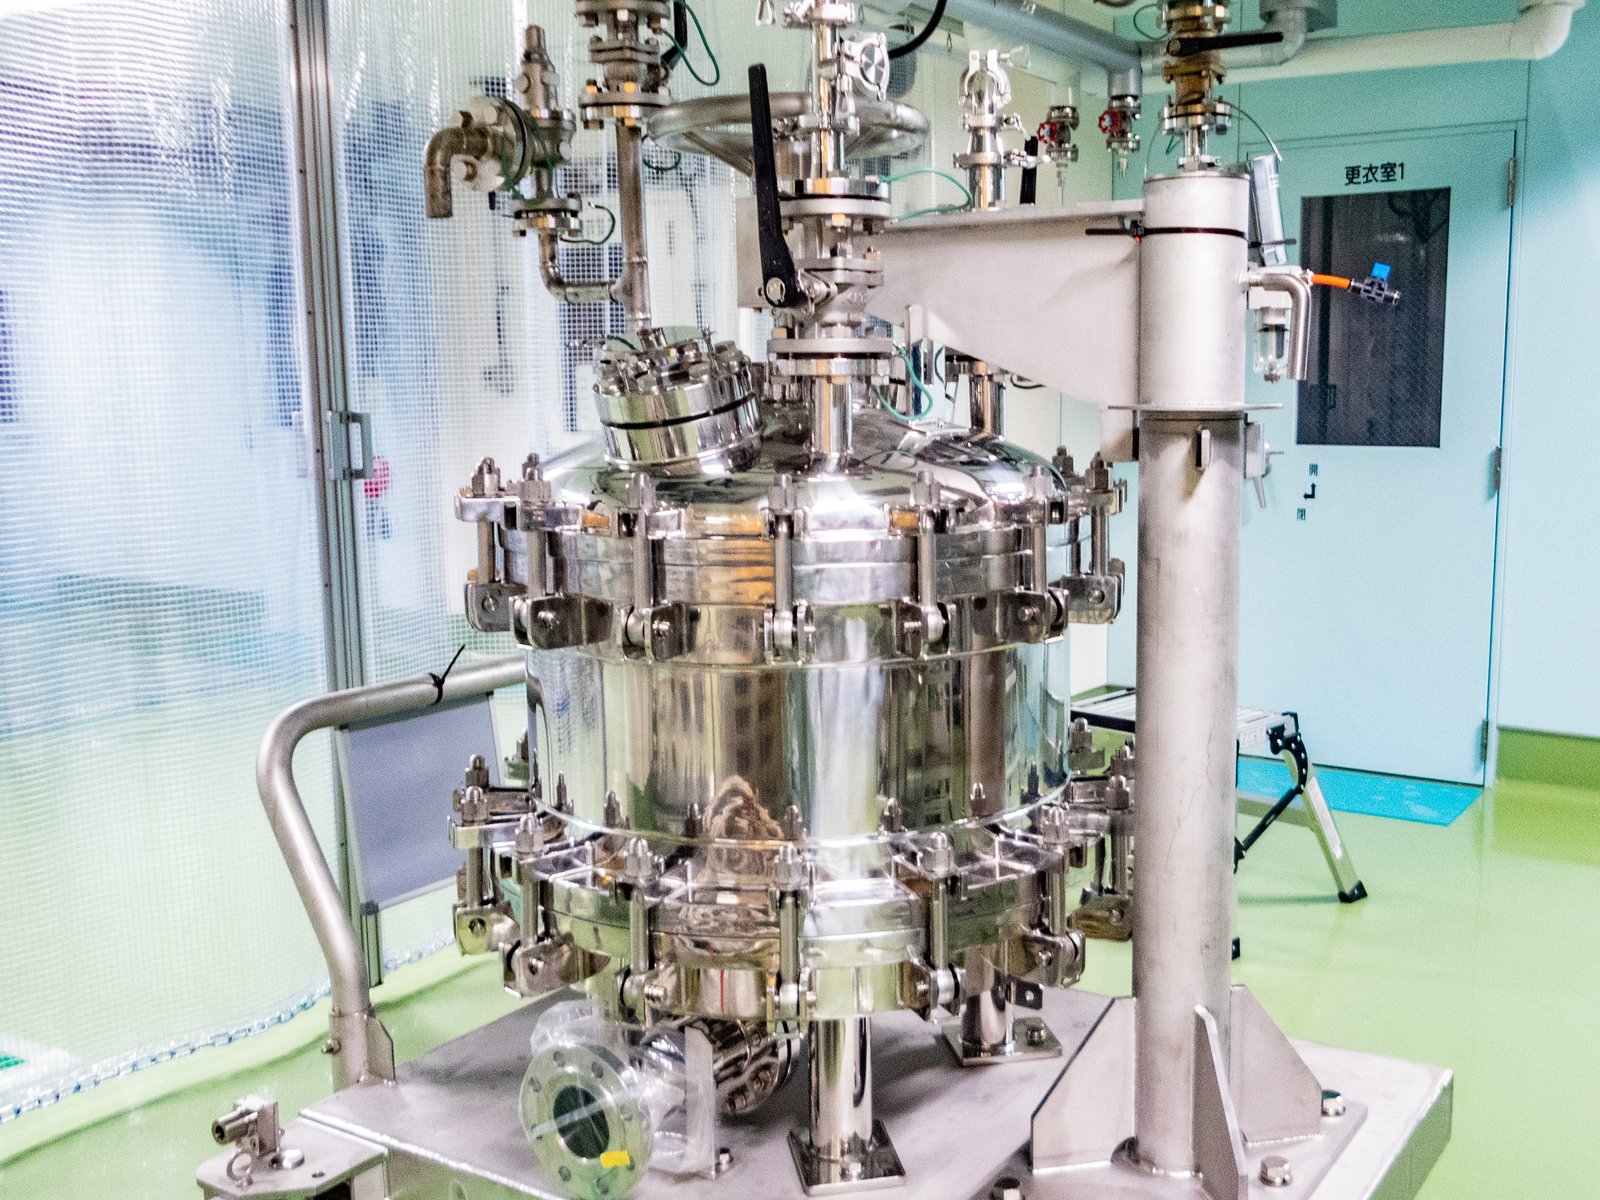
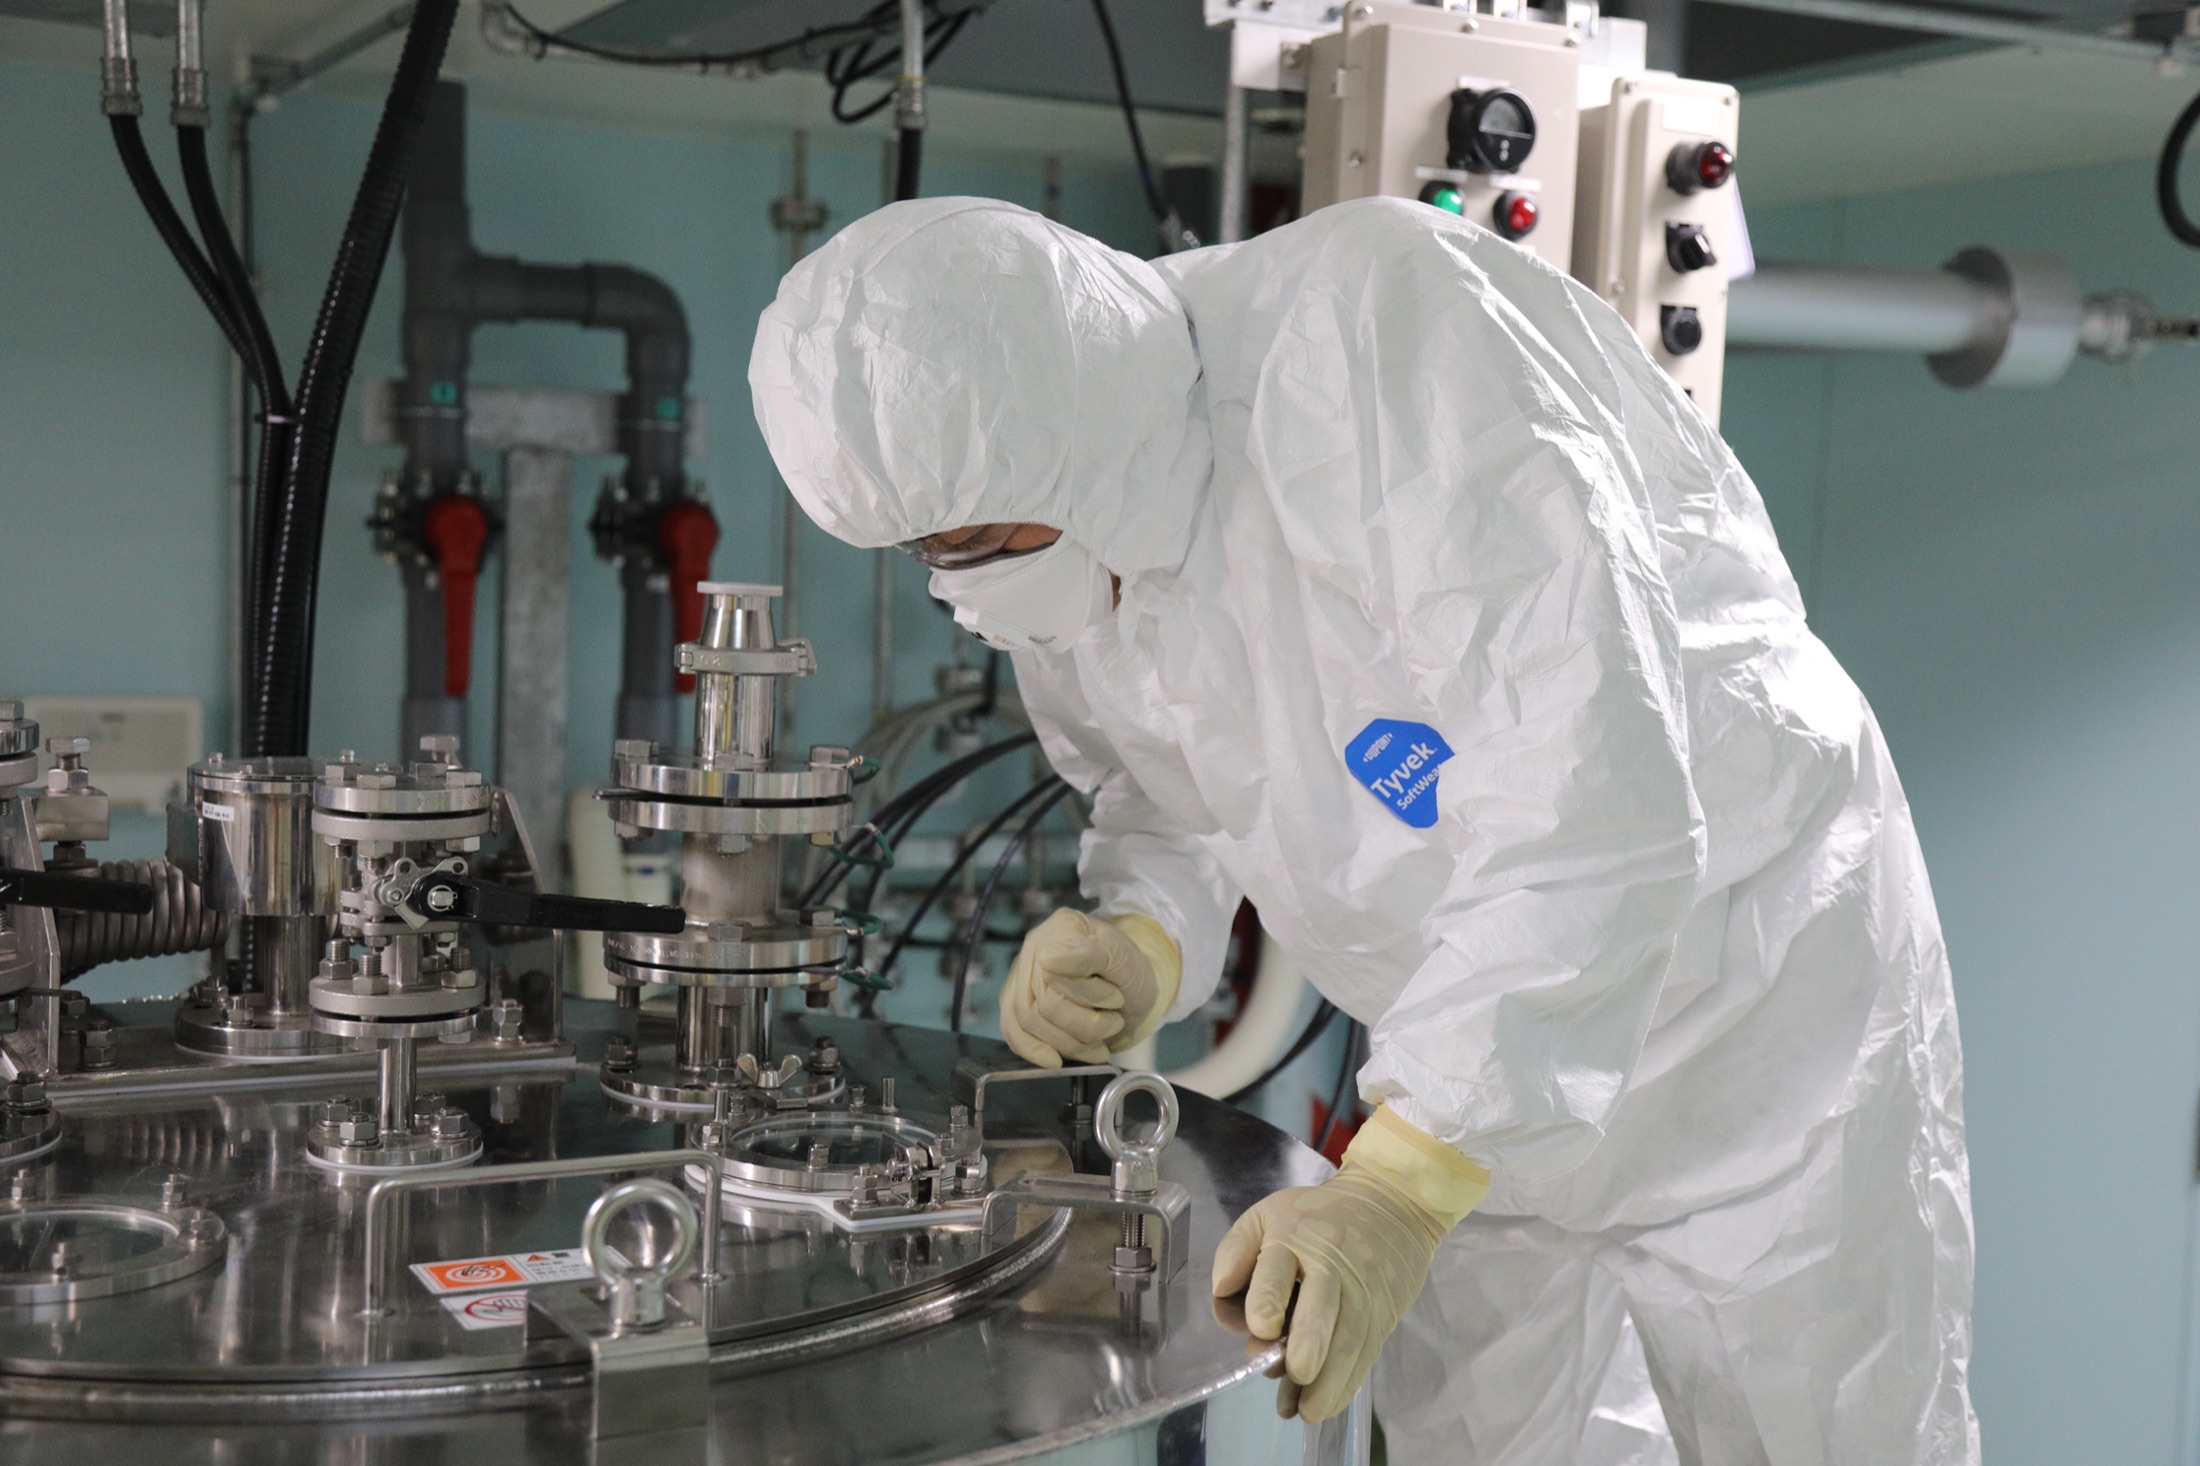
Drying
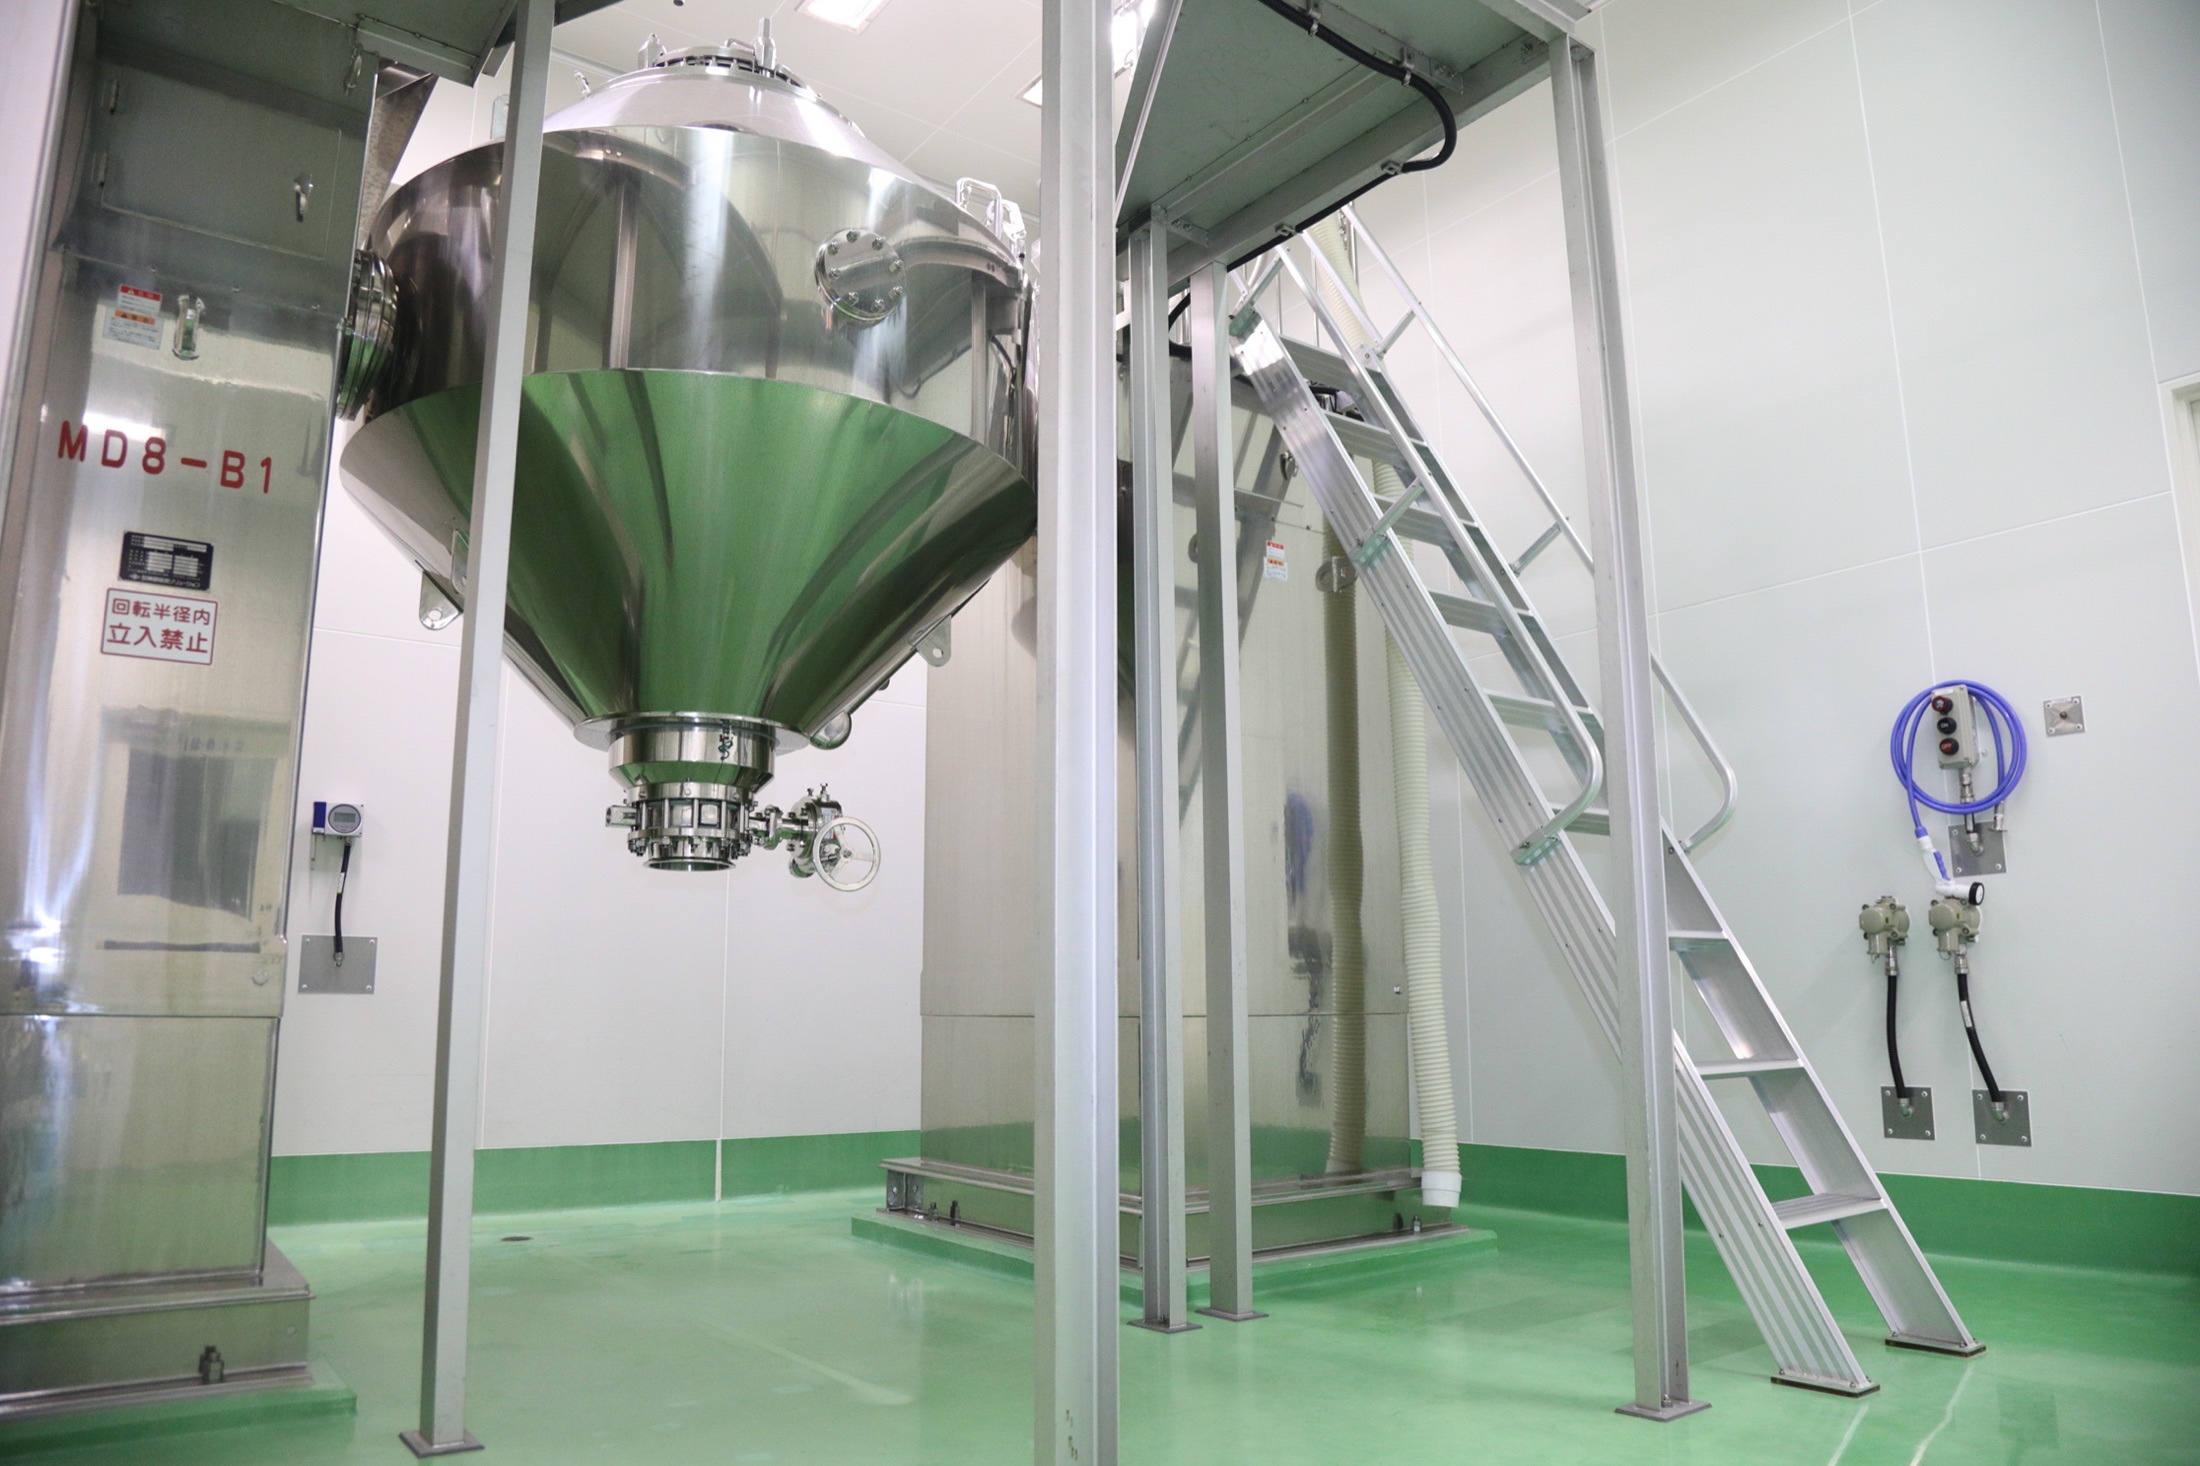
We possess many GL and SUS conical driers ranging in size from 300 liters to 2,000 liters. These driers are installed in separate rooms to prevent contamination. In addition, we also handle such post-drying operations as pulverization and sieving.
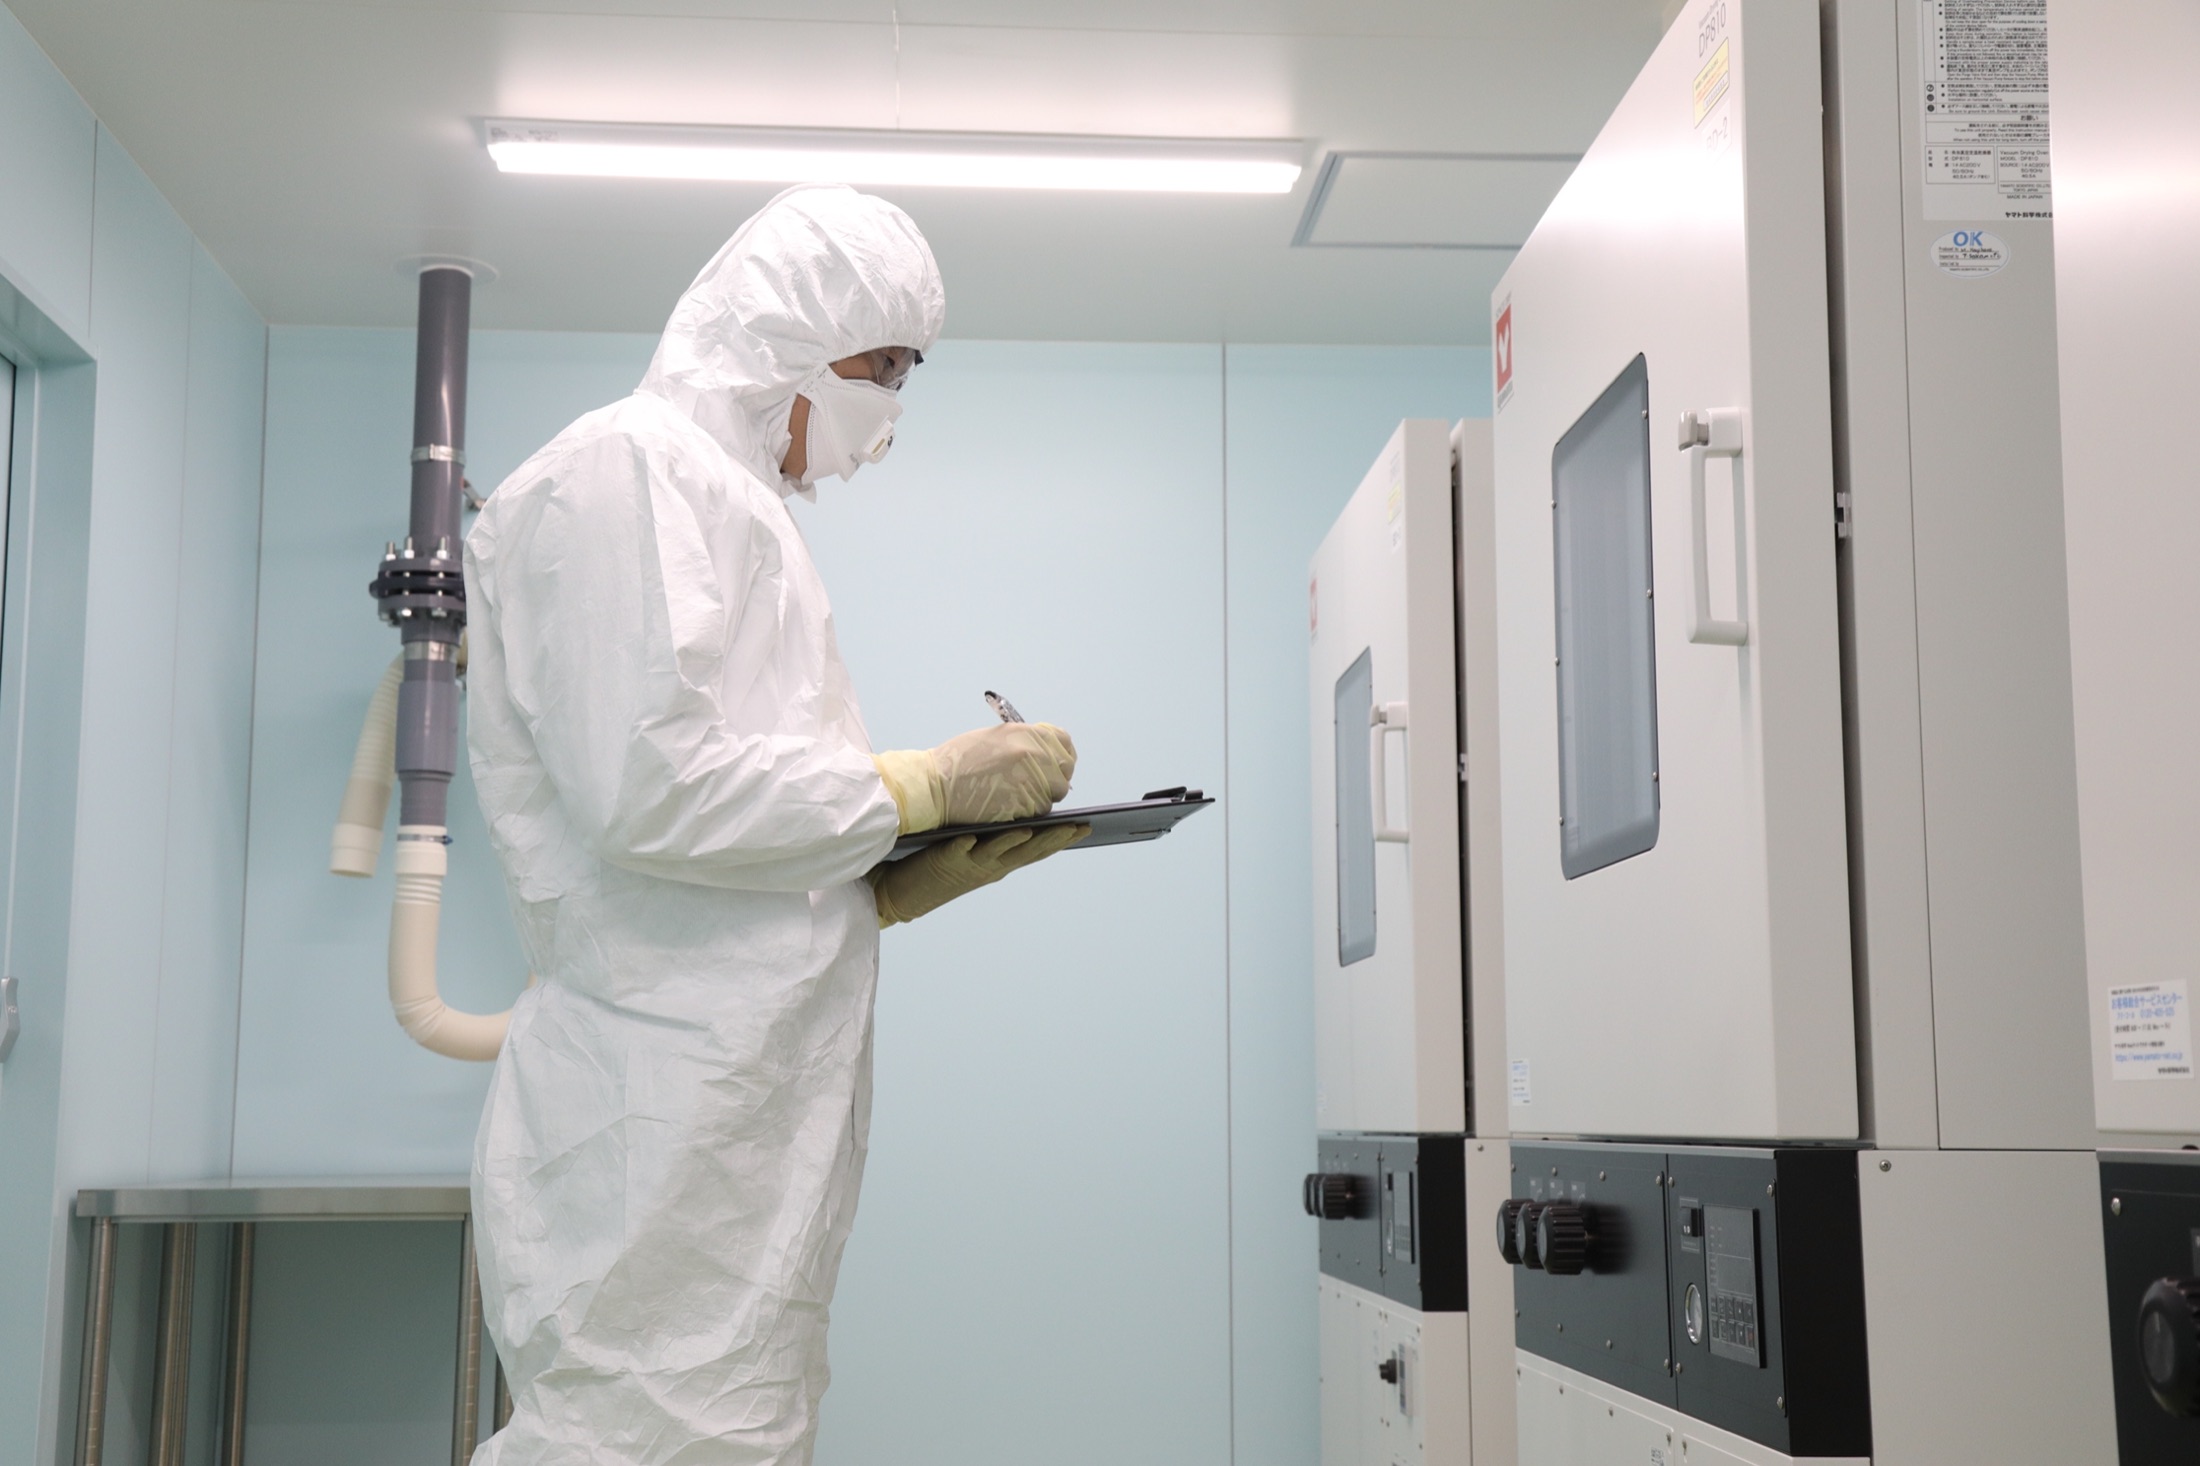
Filling and packaging
All products undergo filling in our filling rooms. Our Fukuoka Plant houses a filling room capable of handling flexible containers under GMP control.
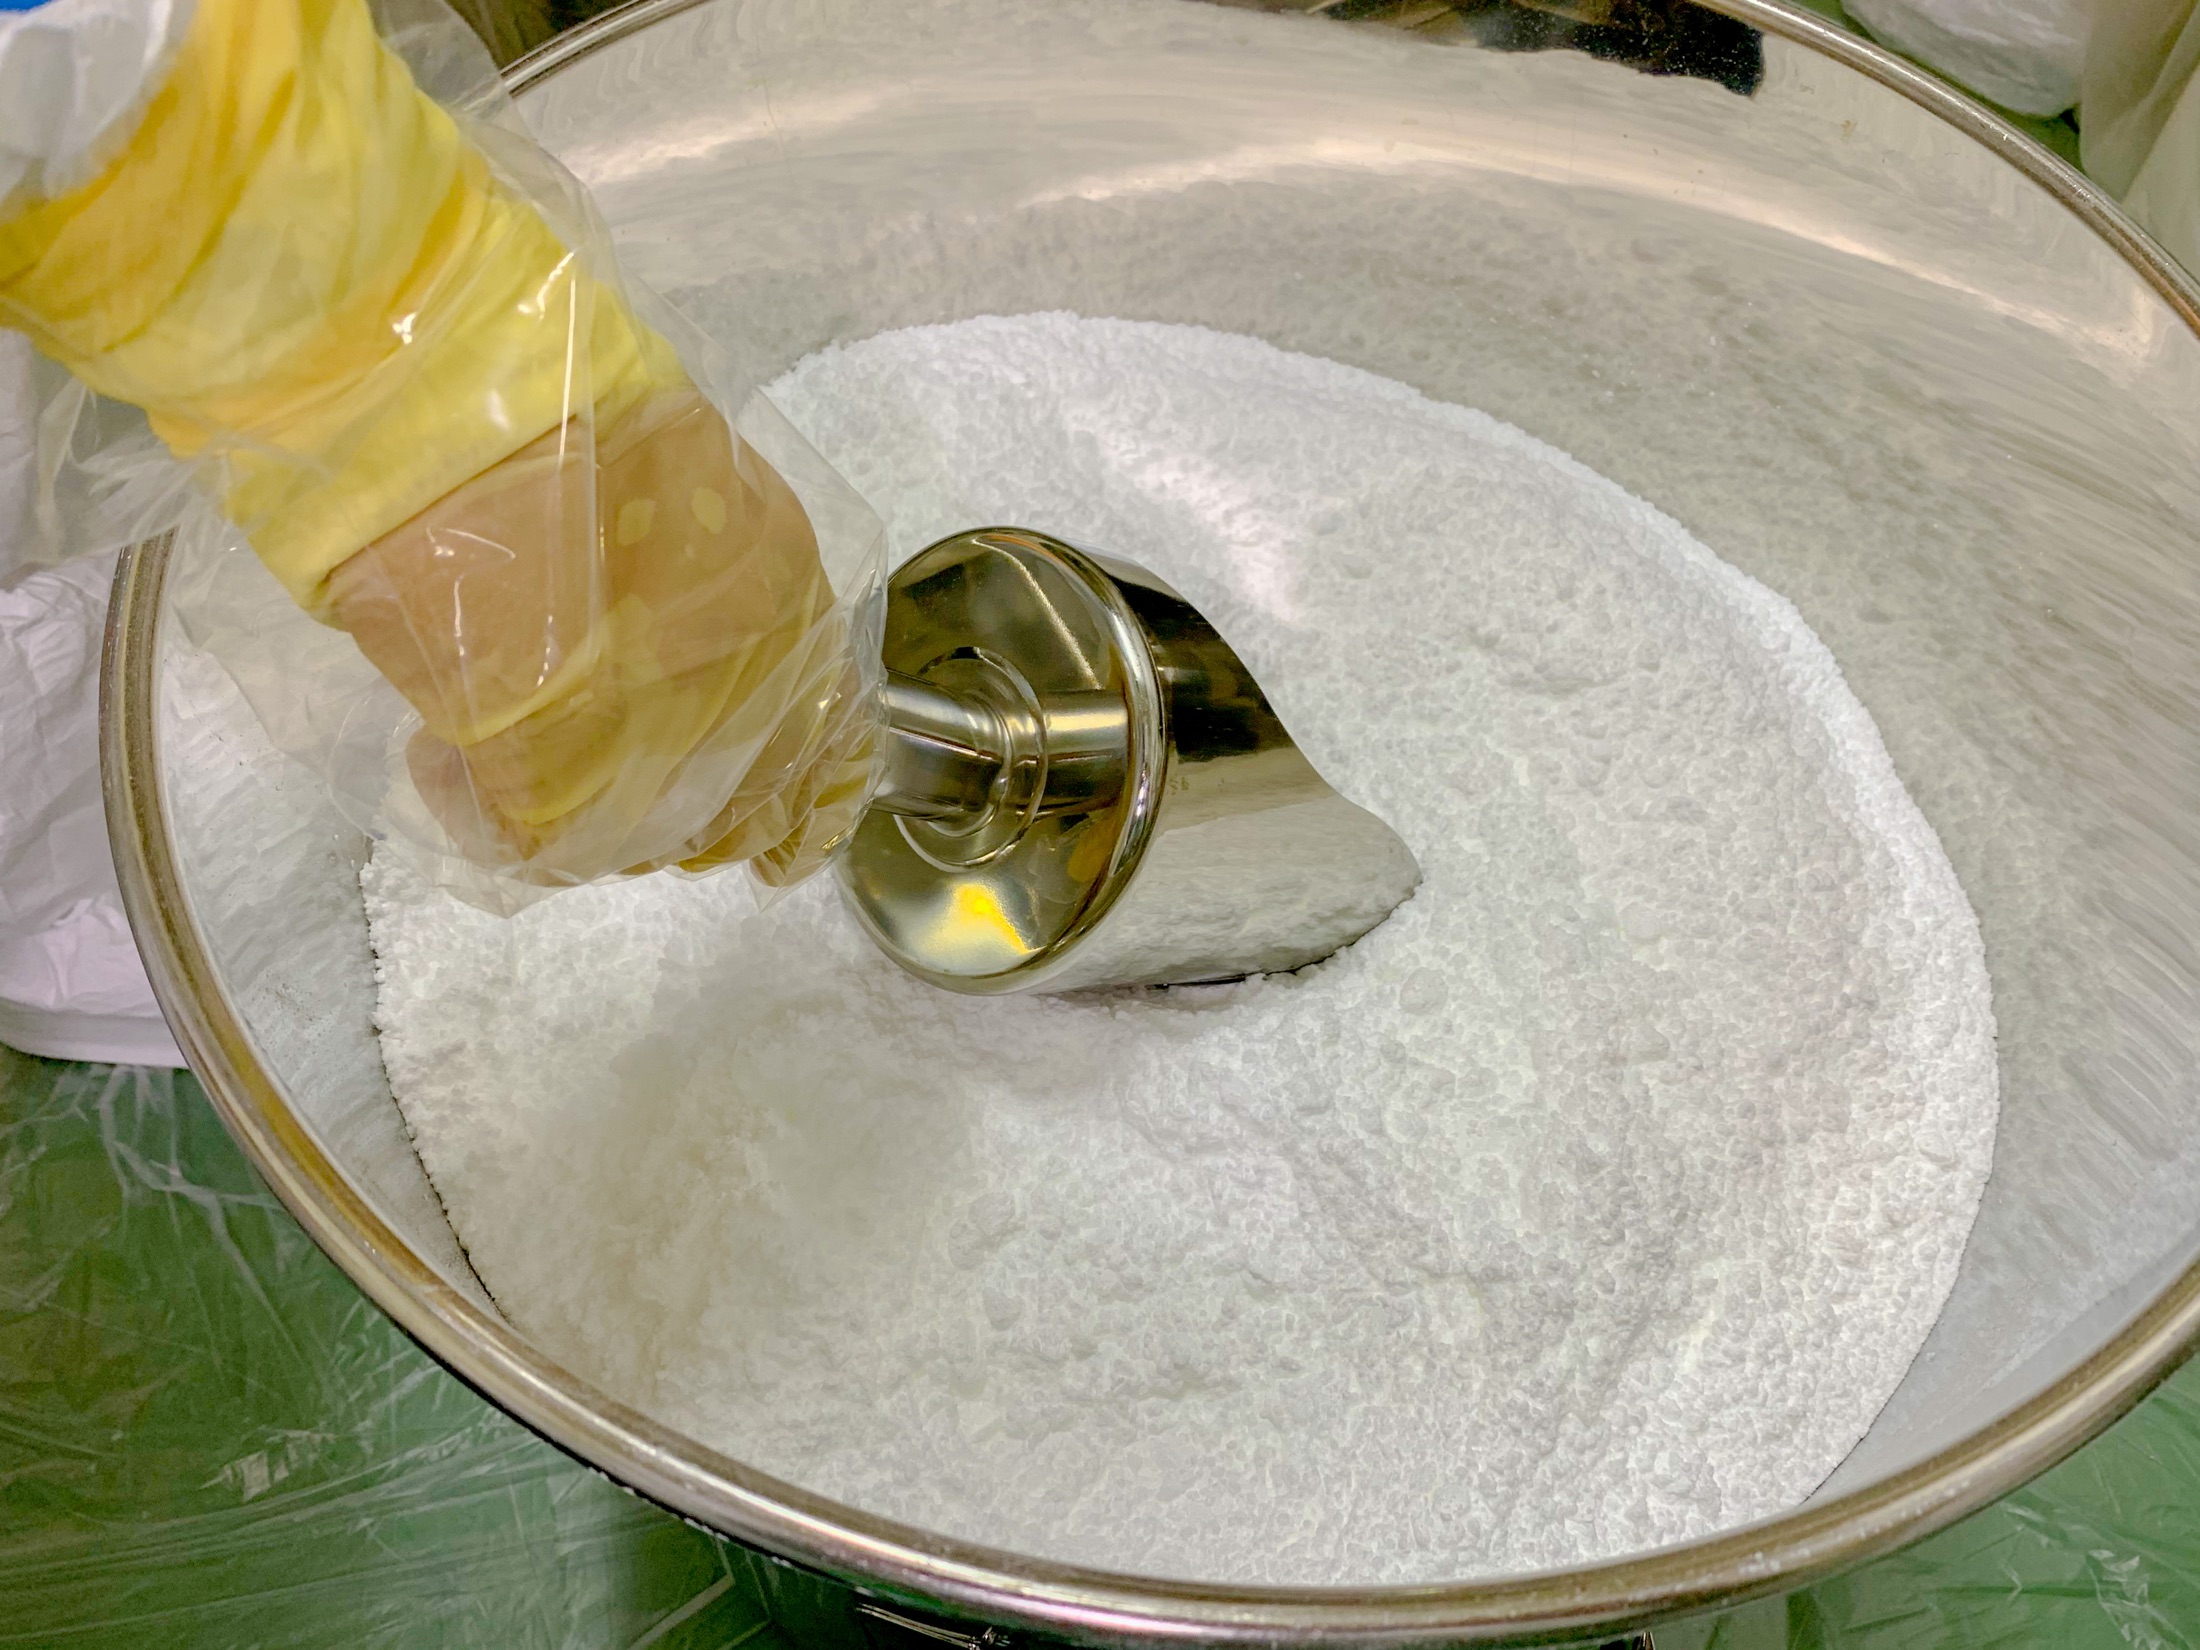
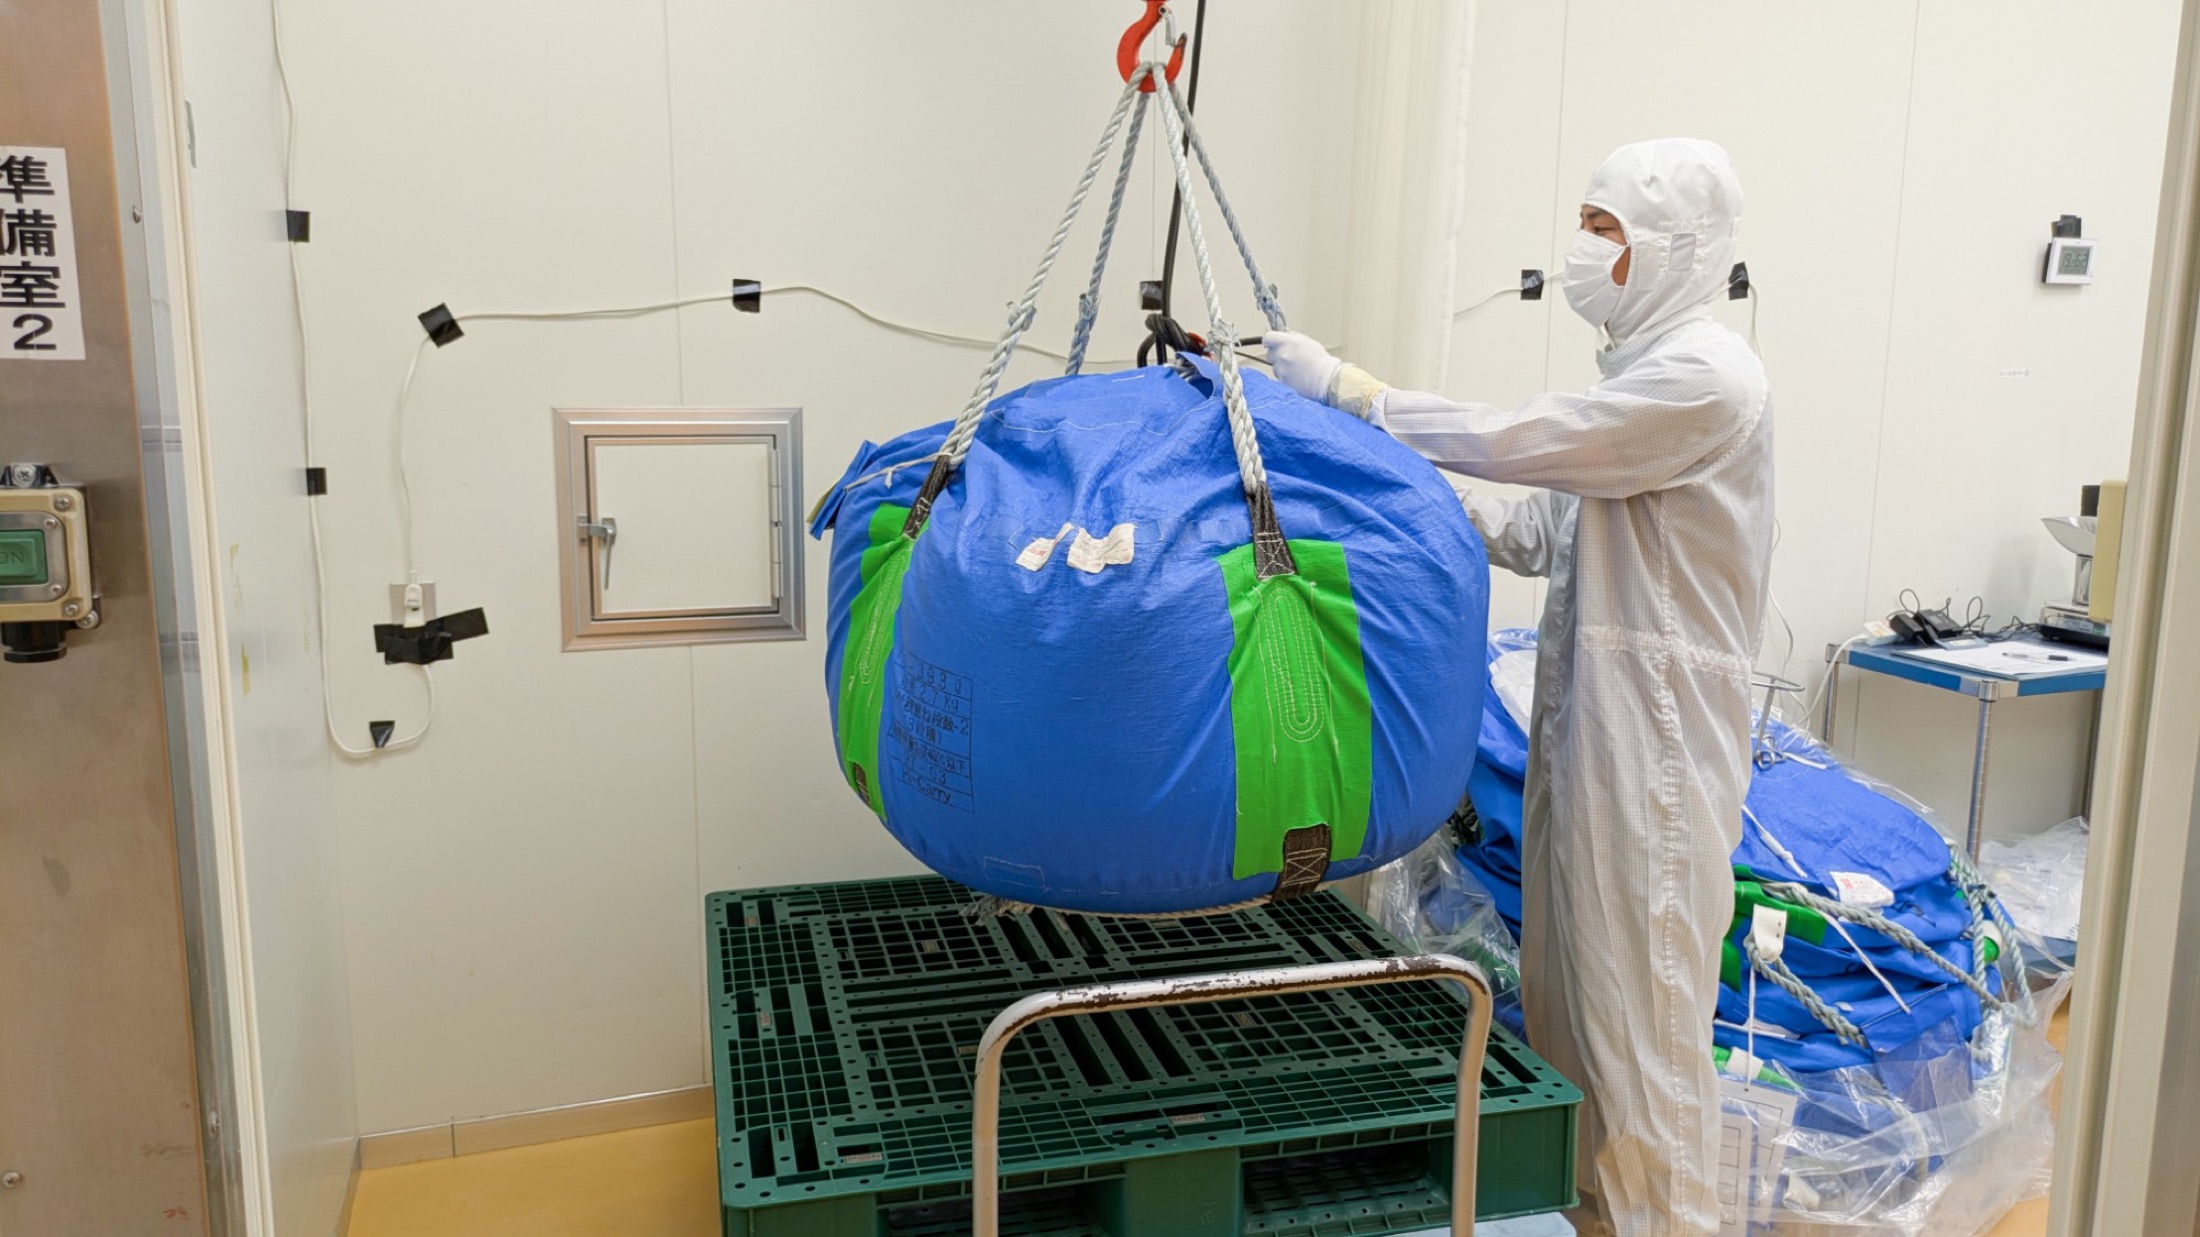
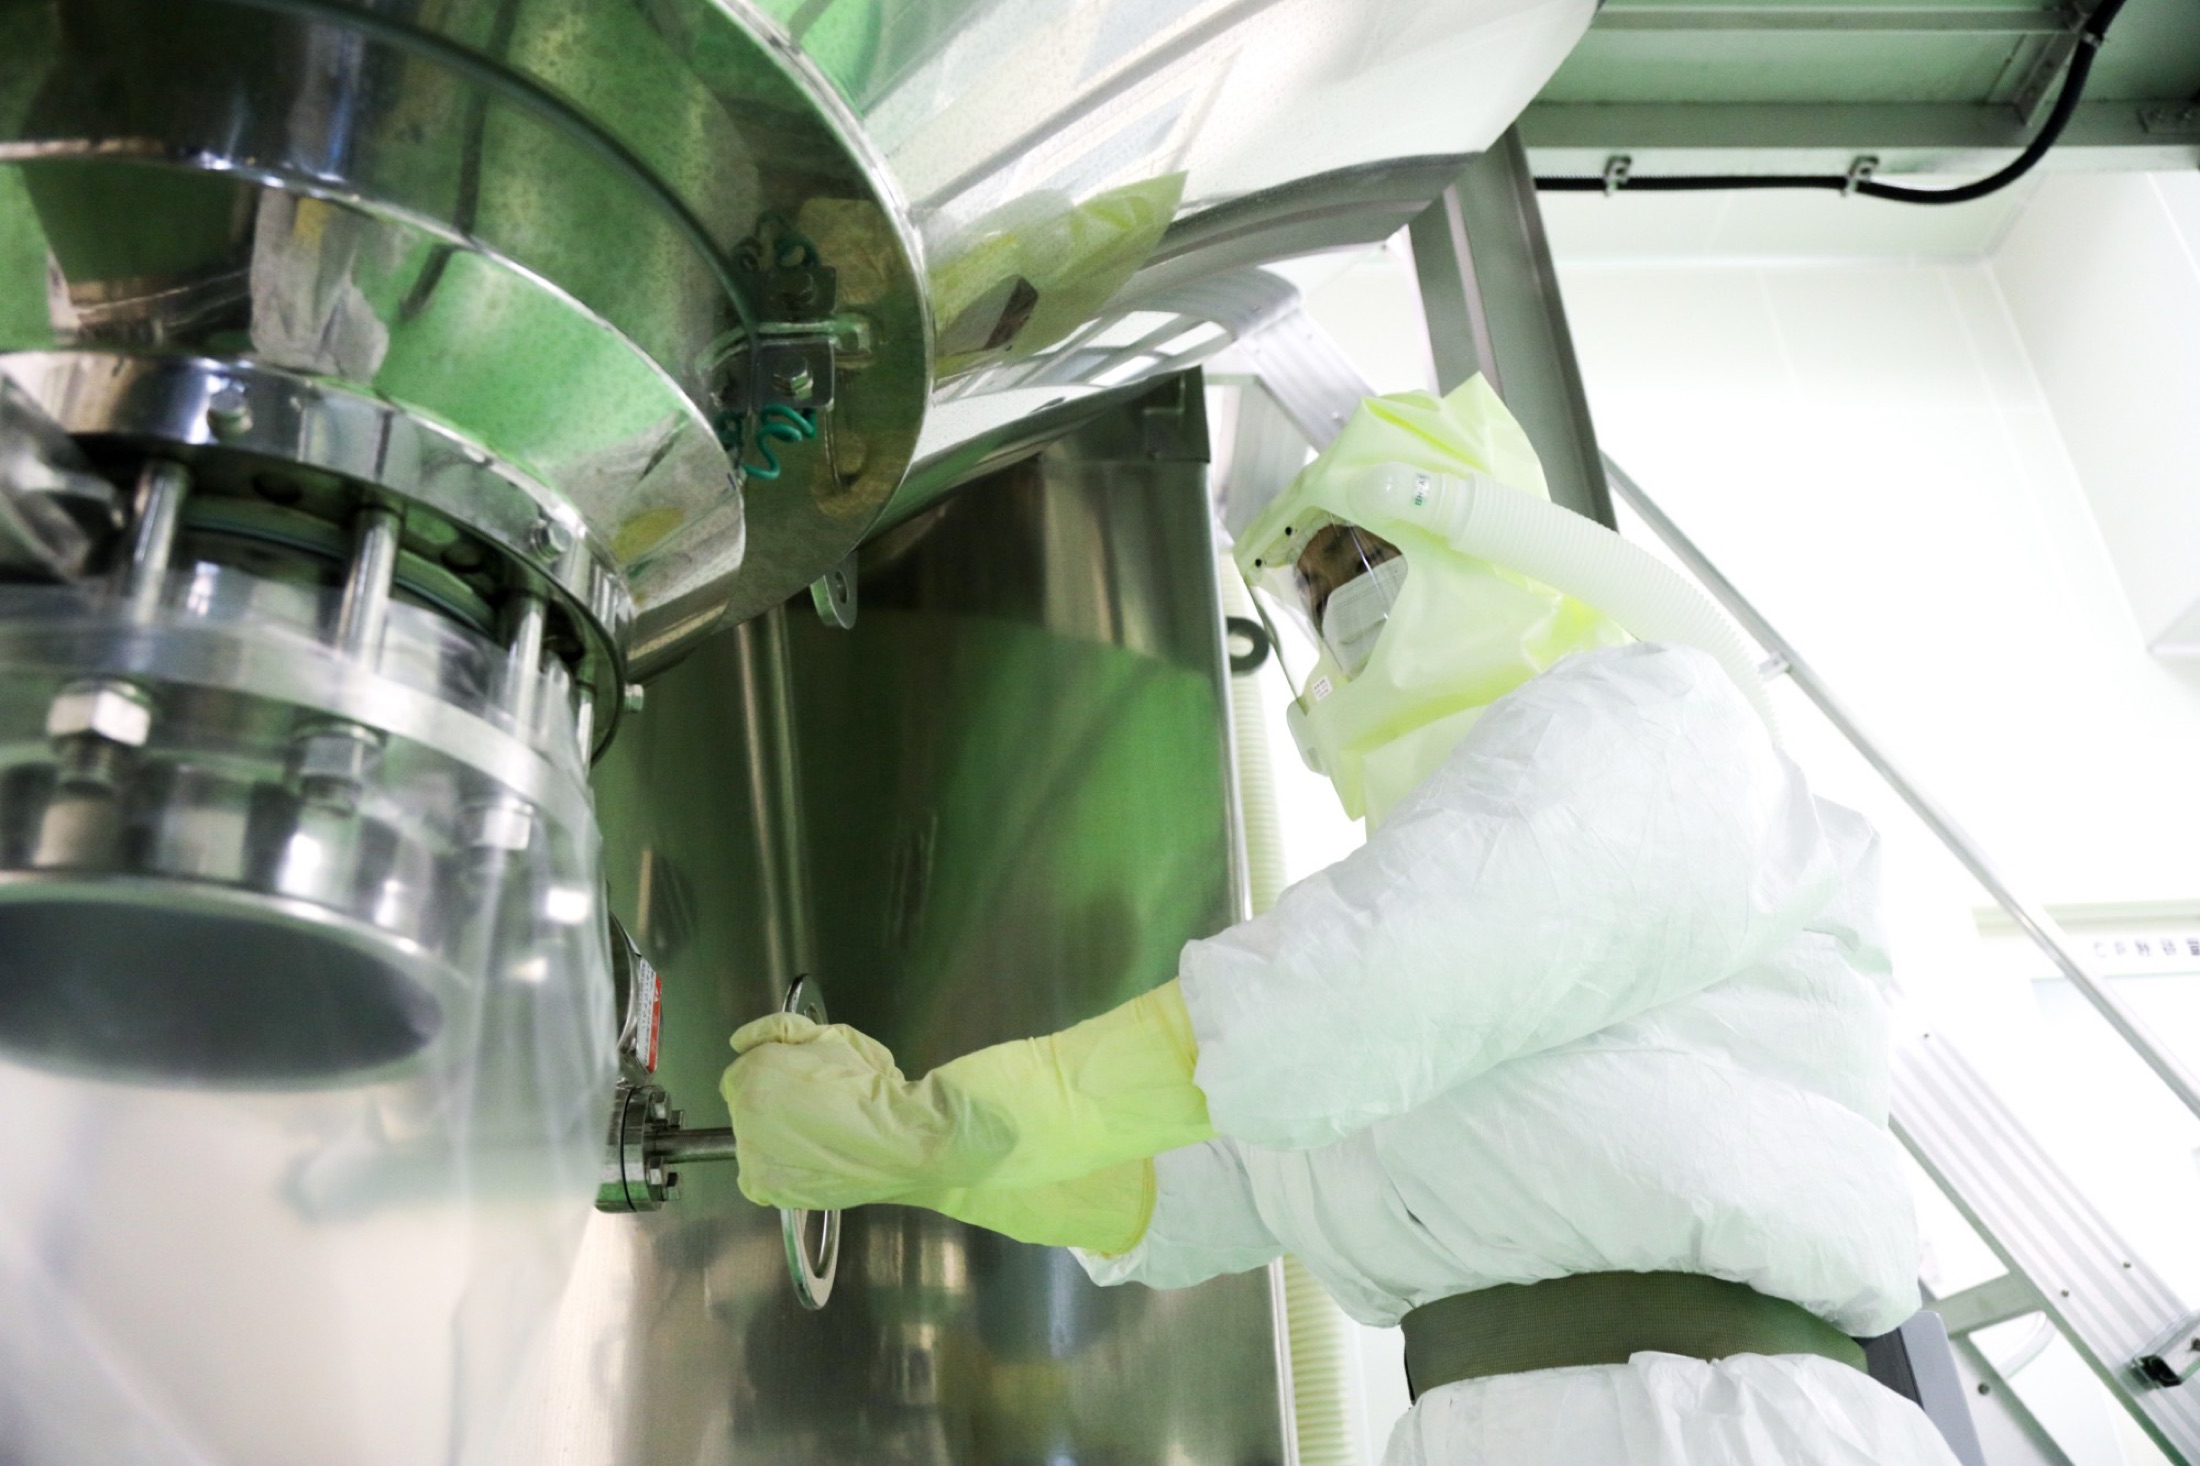
Since steroid active pharmaceutical ingredients exert strong bioactive effects on the human body even when present in trace amounts, the manufacturing process is subject to exceedingly strict standards to prevent worker exposure and prevent external environmental contamination. We possess one of just a handful of facilities dedicated to the handling of steroids and manufacture ingredients in a strictly contained environment.
Steroid active pharmaceutical ingredients building (Iwaki Plant)
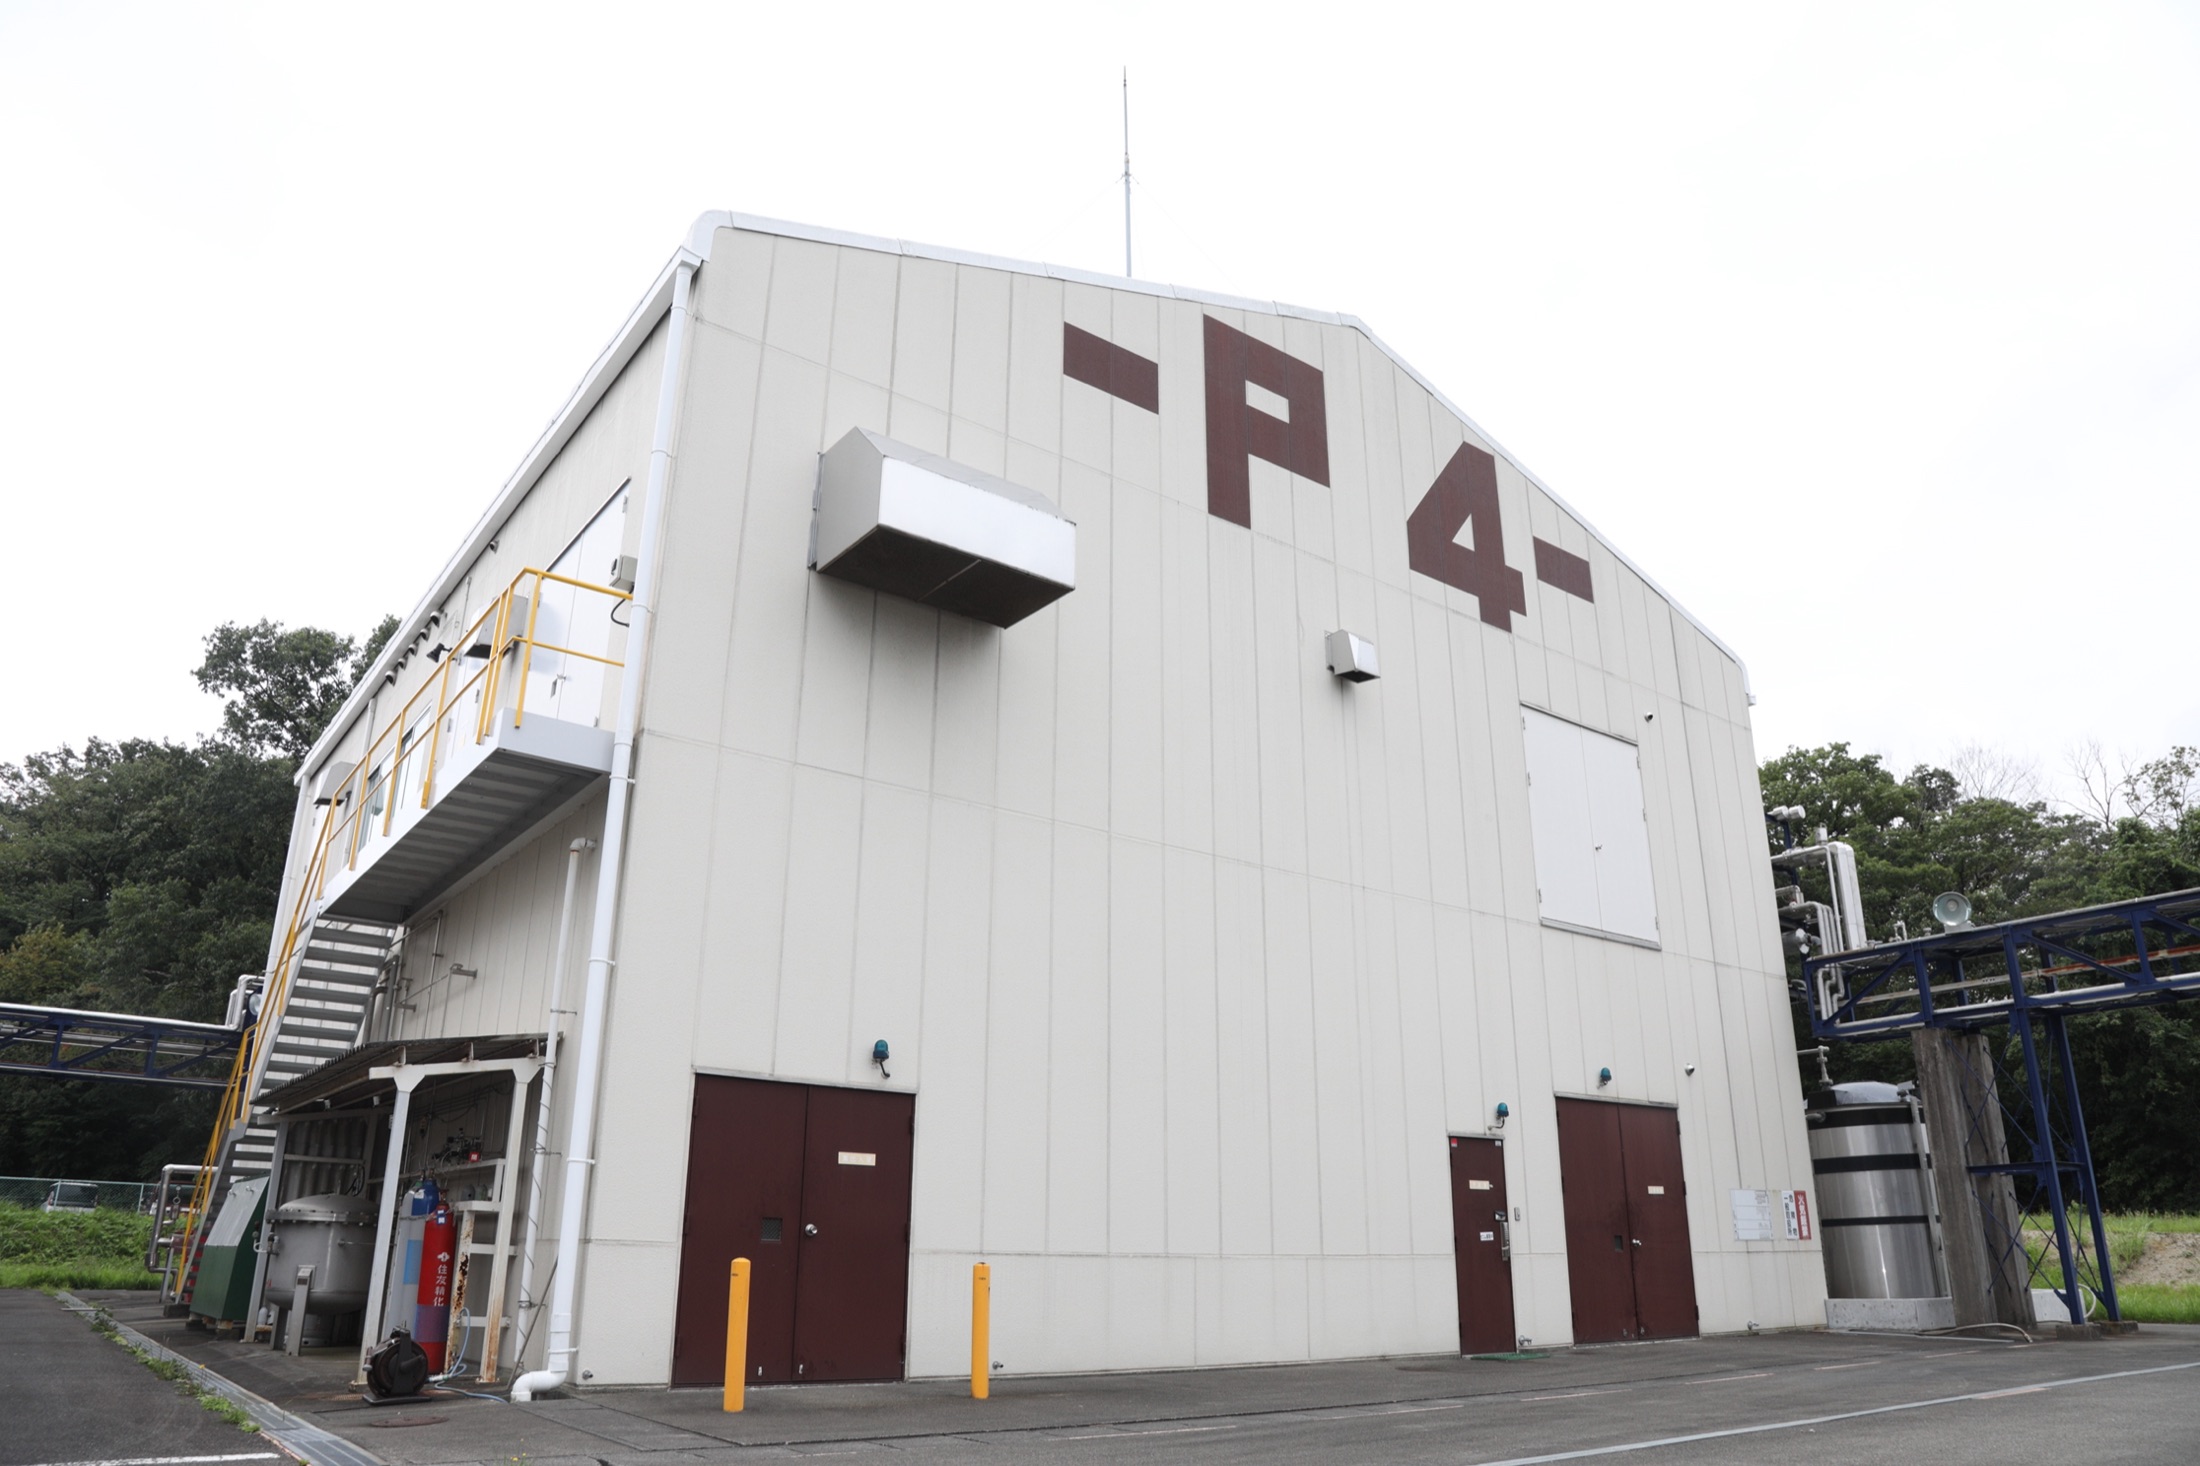
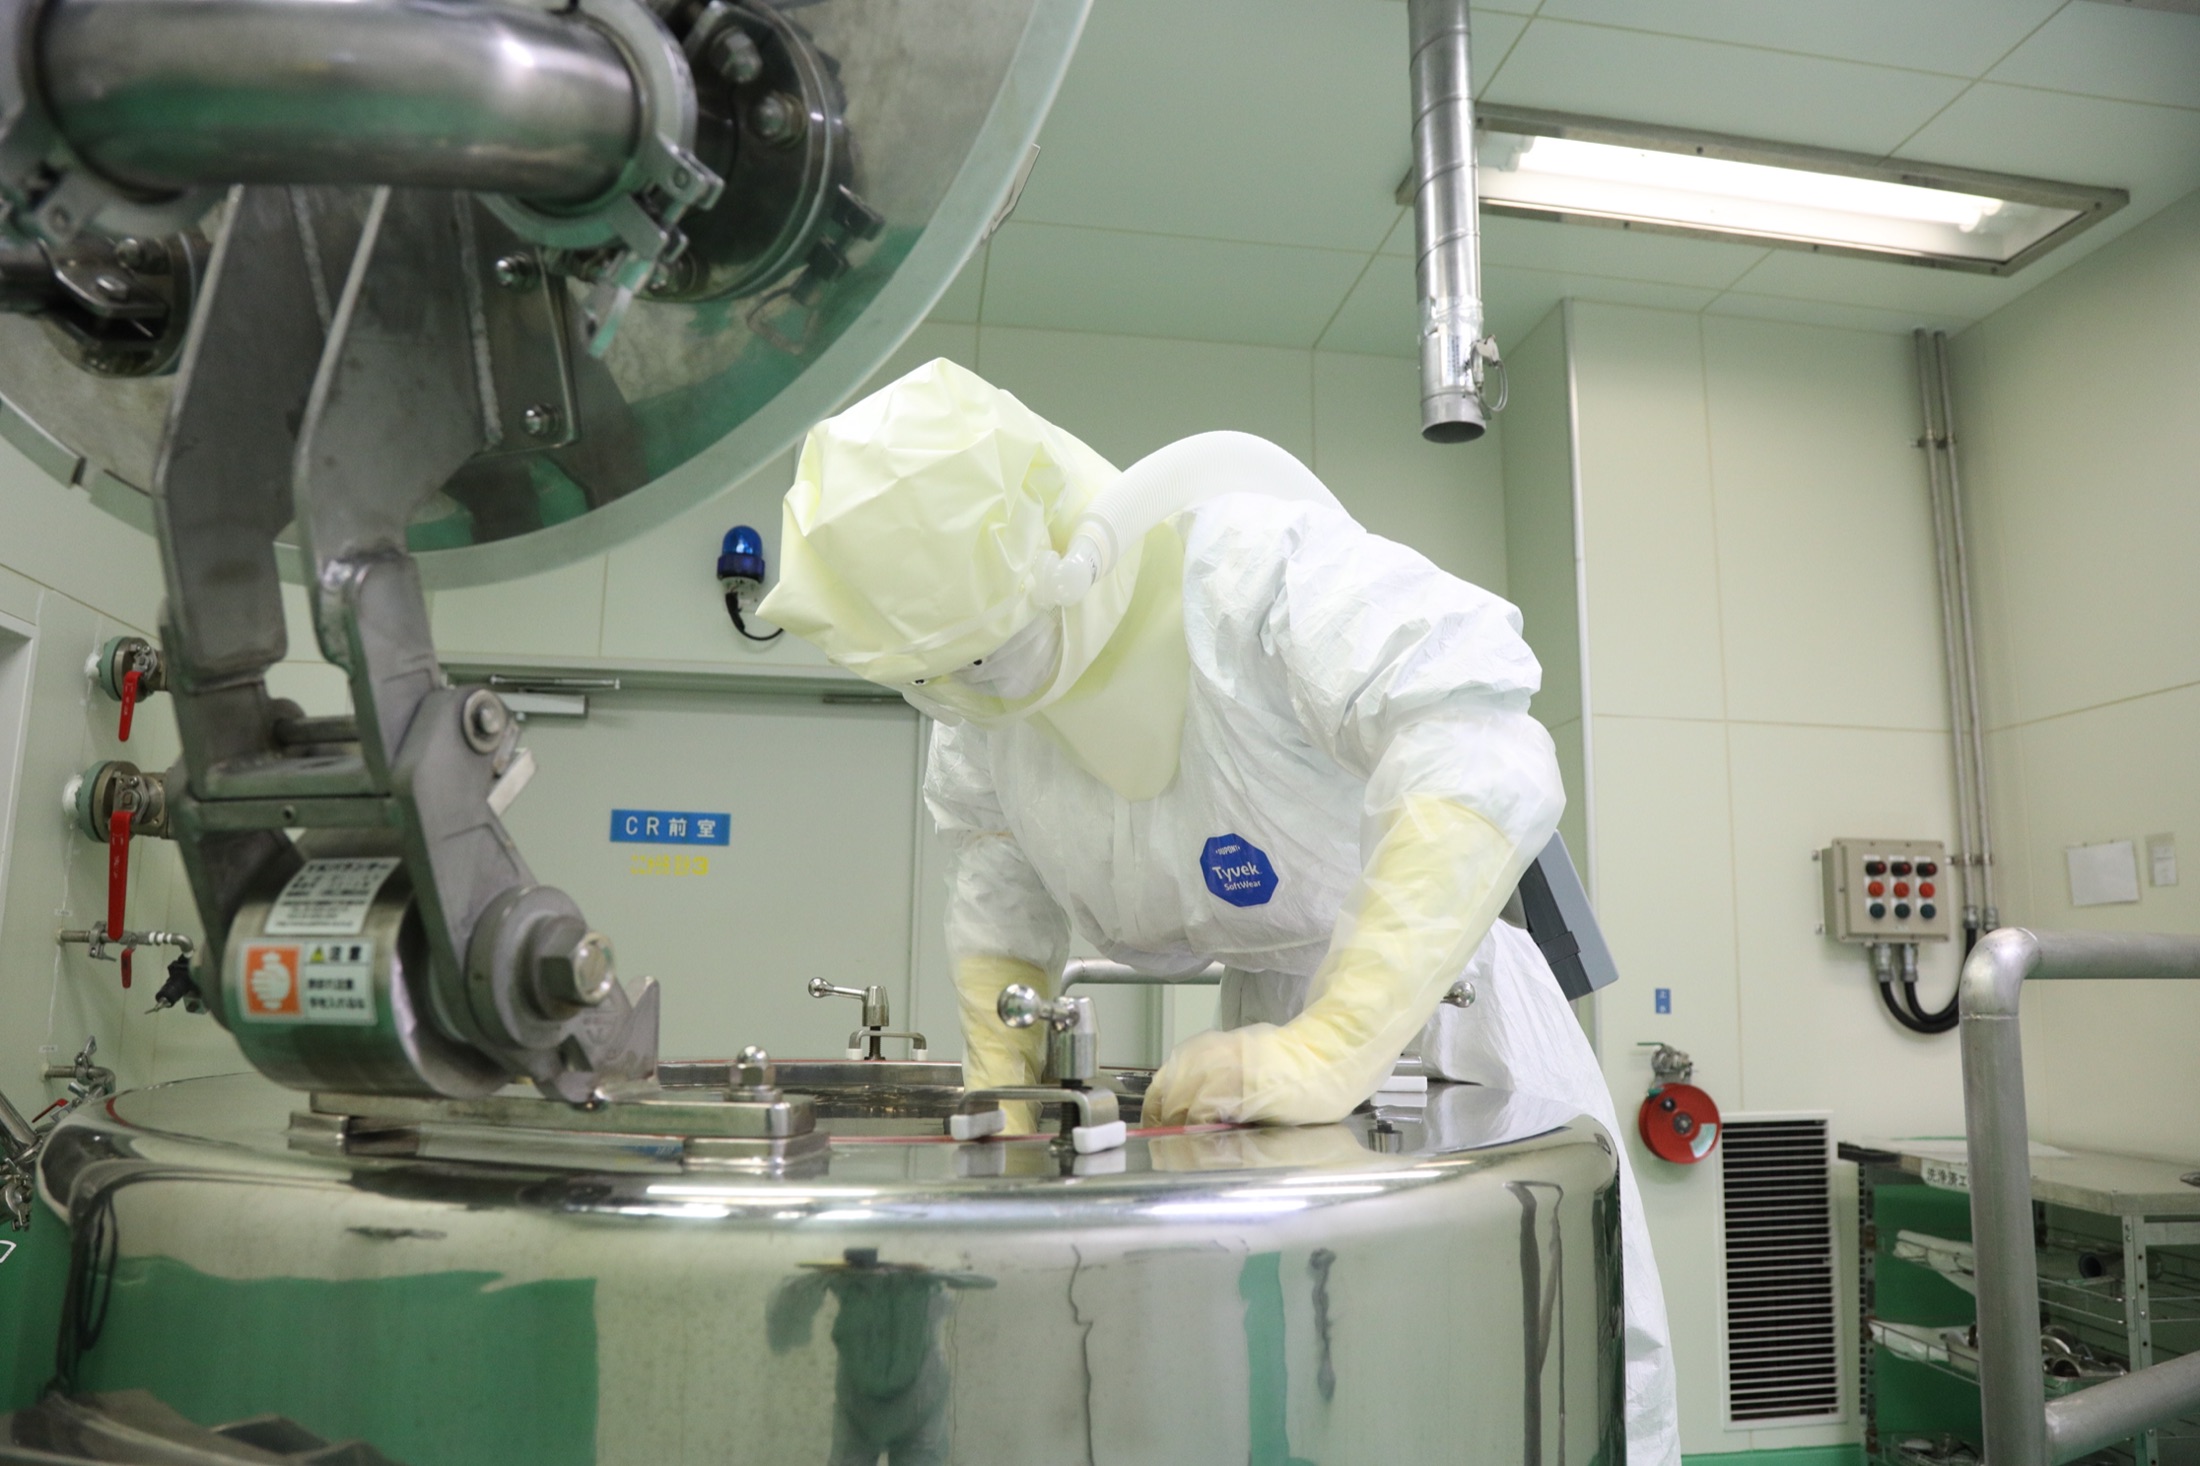
Photoreactions are utilized on an industrial scale to realize structures that are difficult to achieve through conventional synthesis and shorten processing times. We possess a 600-liter GL reactor (with a 10 kW light source) and have compiled a track record in applications involving chemicals and pharmaceutical intermediates.
Photoreaction units (Fukuoka Plant)
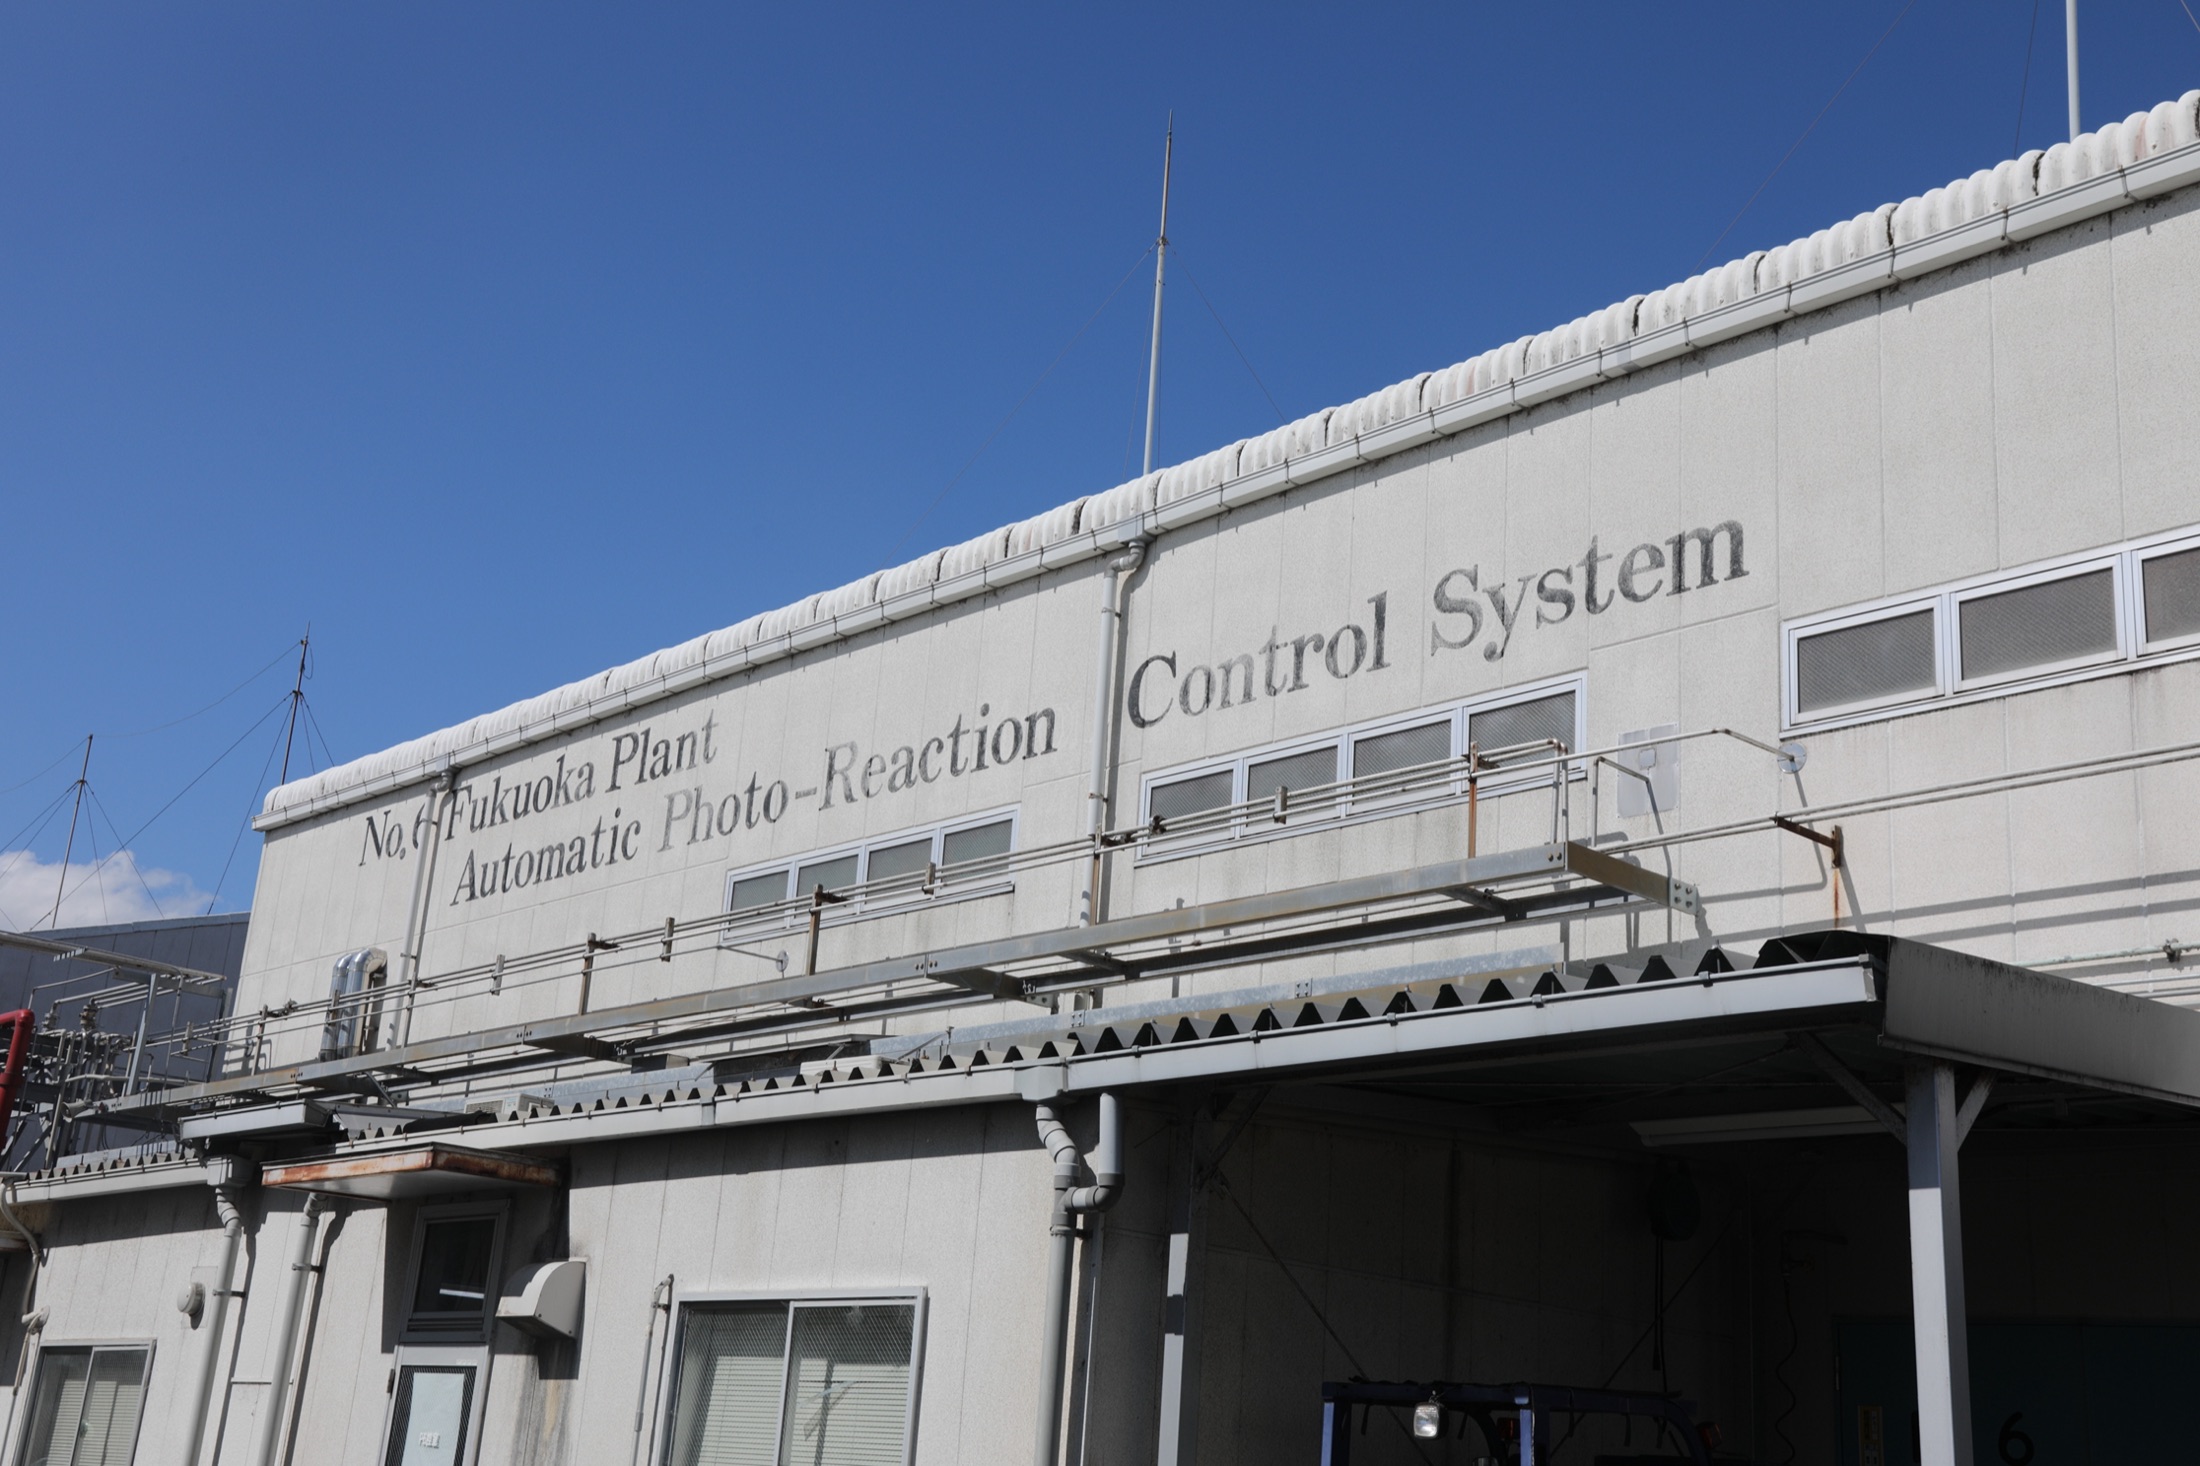
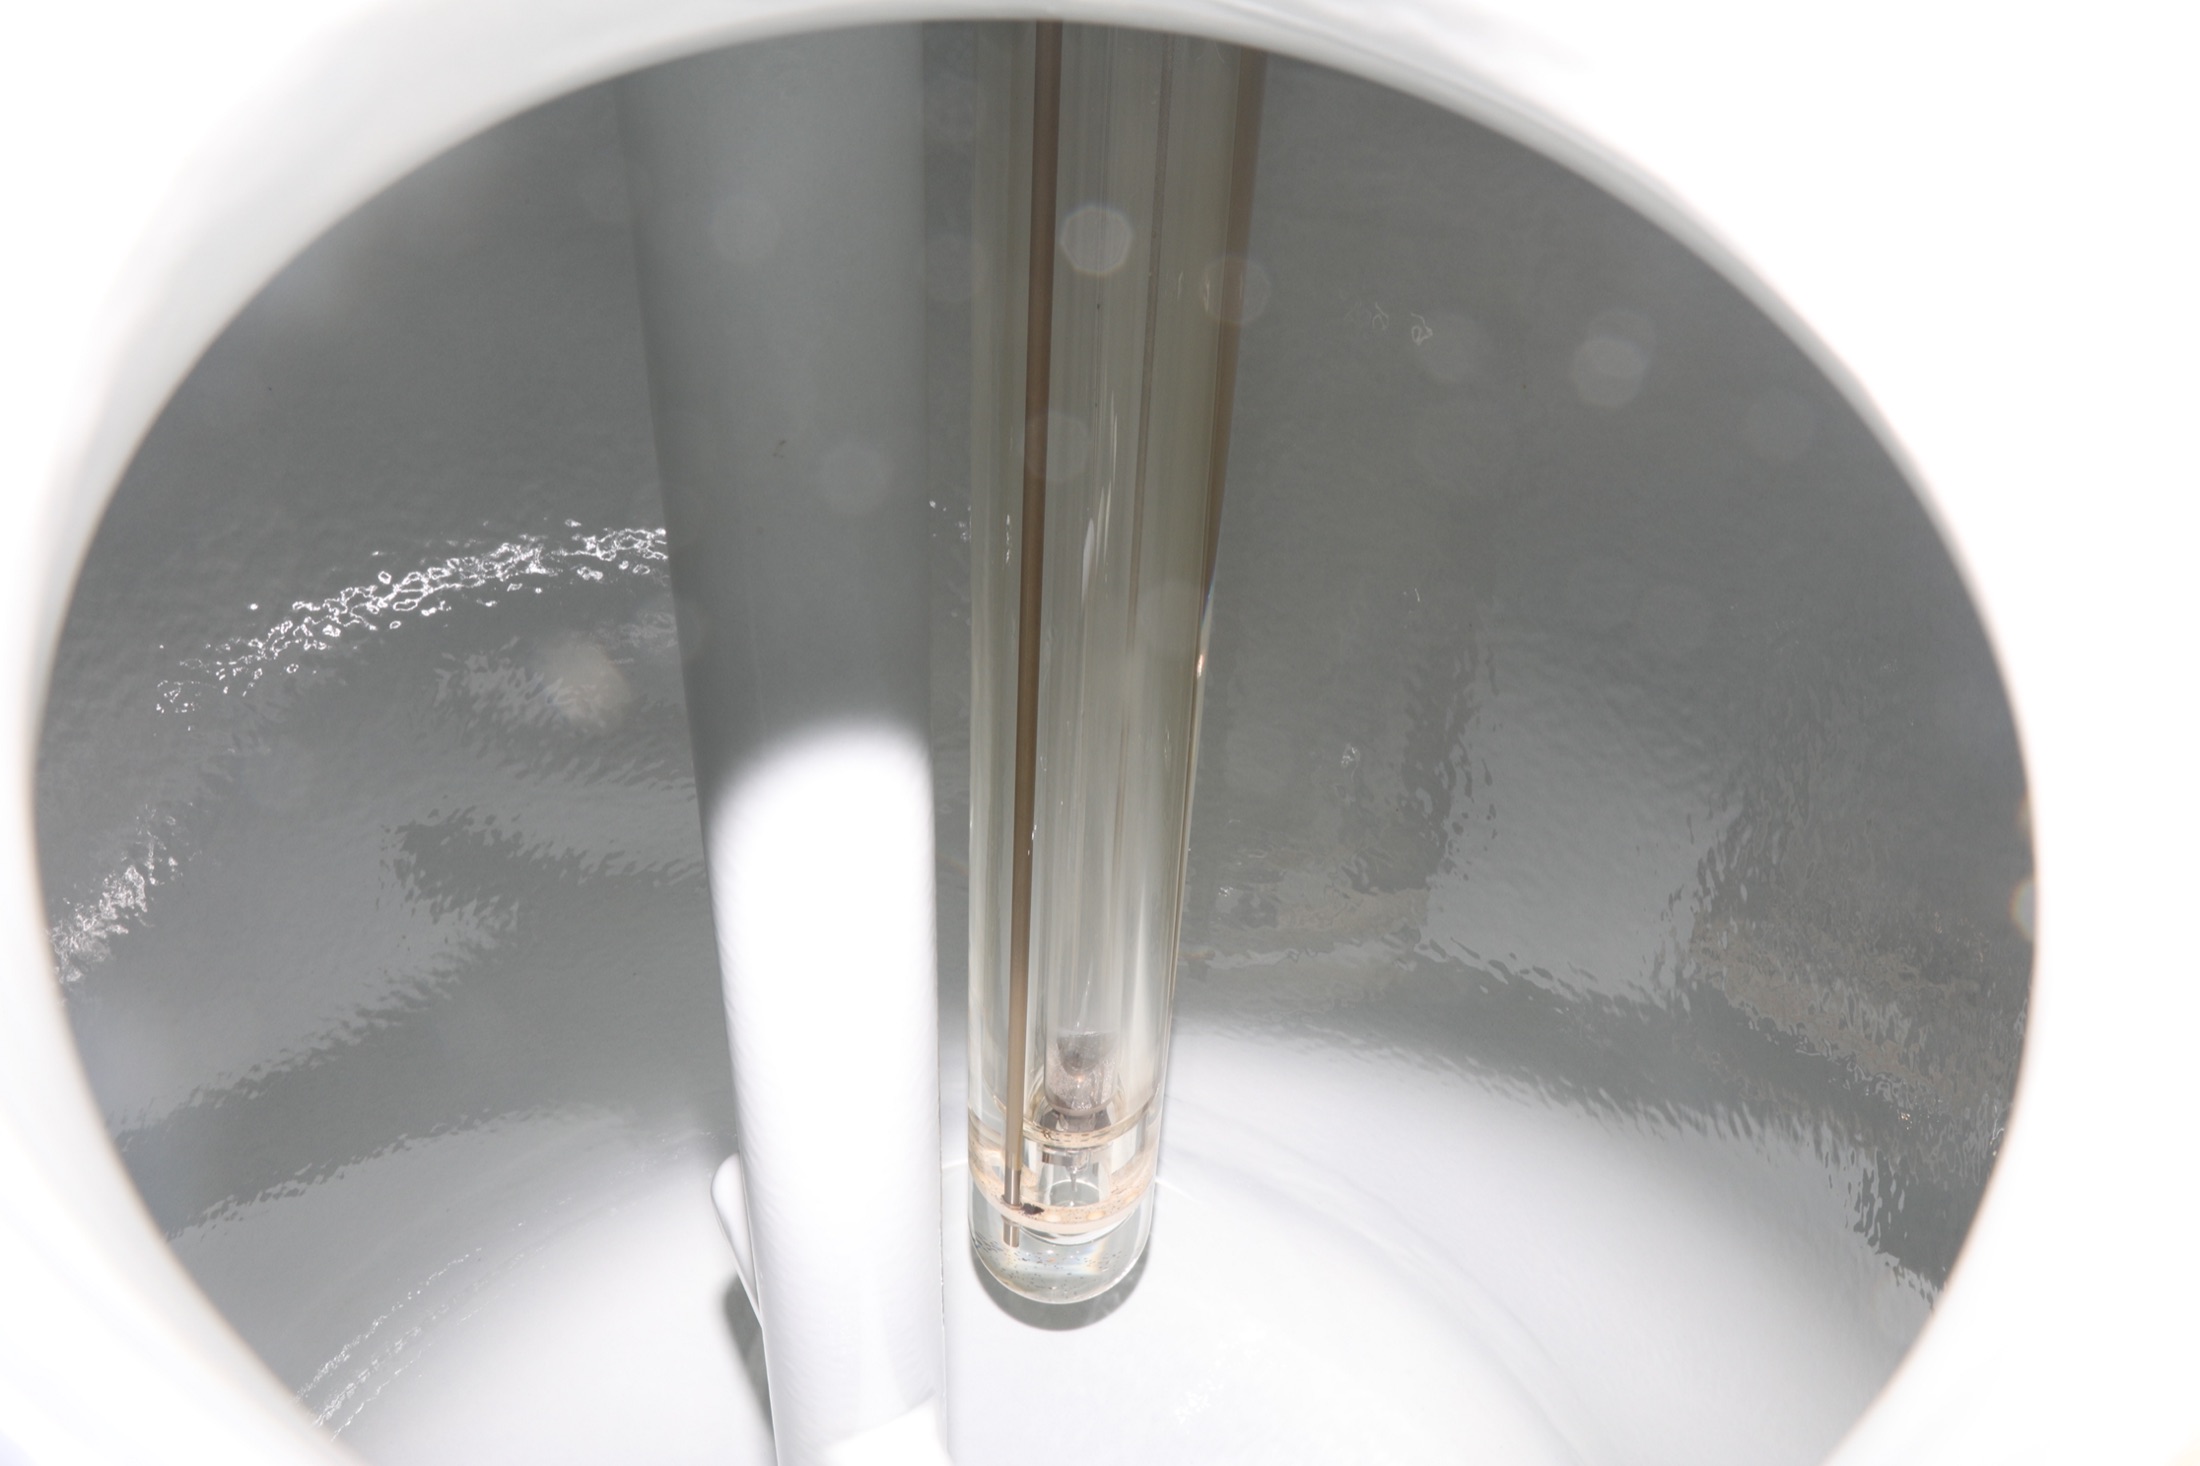
Resin purification
We possess resin columns ranging in size from 150 to 1800 liters, which are quite rare in Japan. These are used to separate water-soluble compounds and remove ionic impurities.
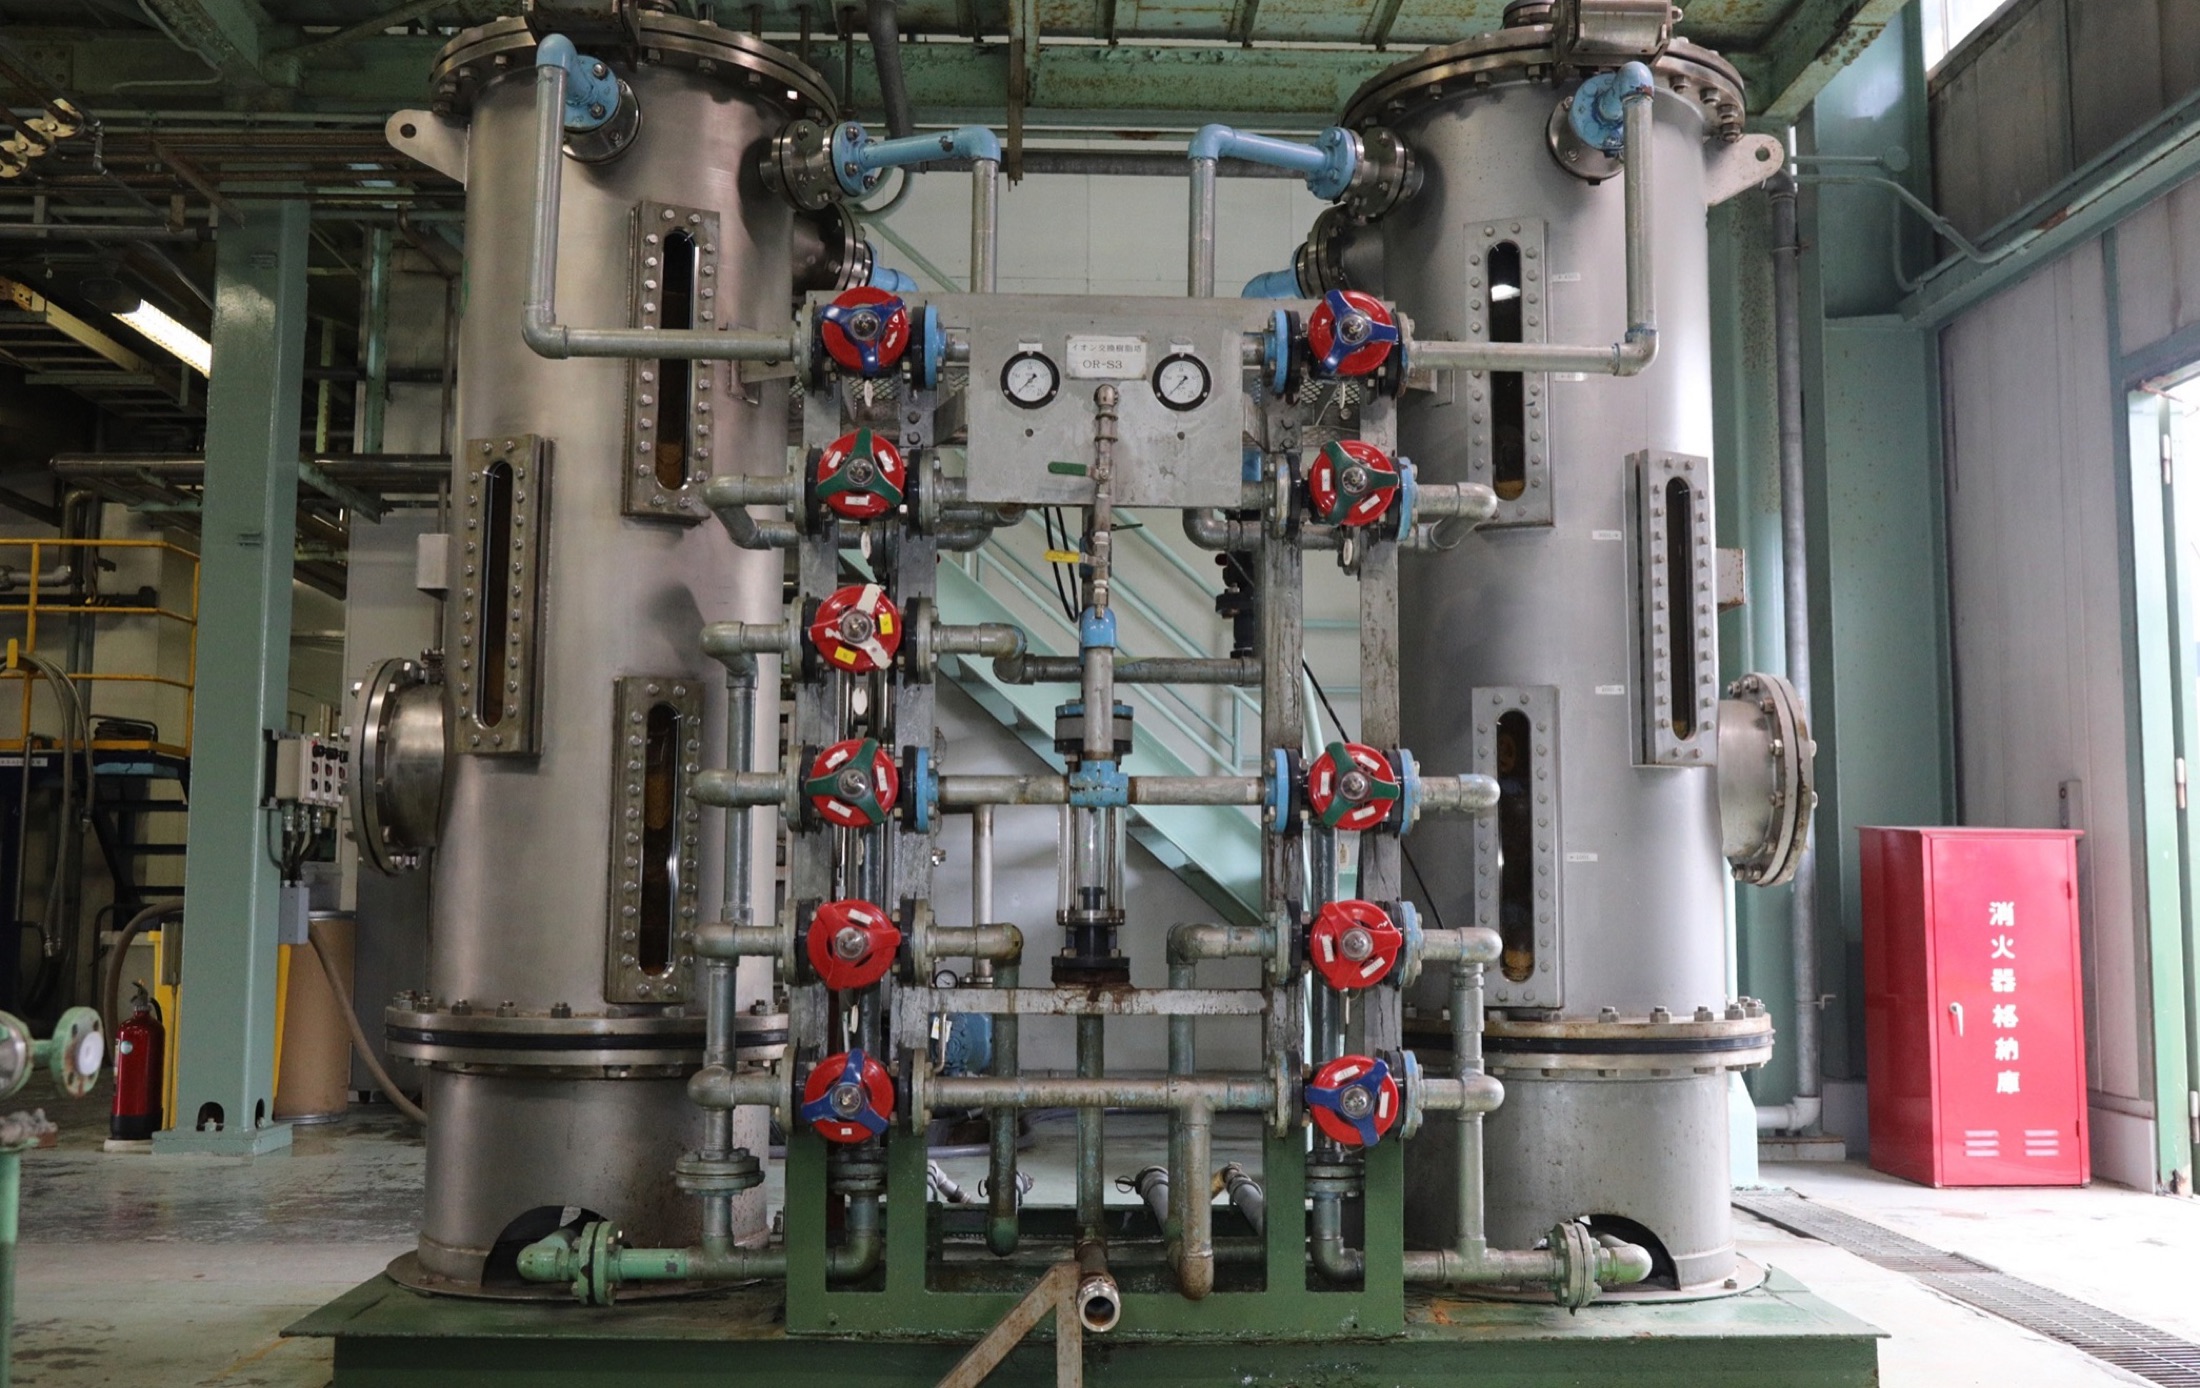
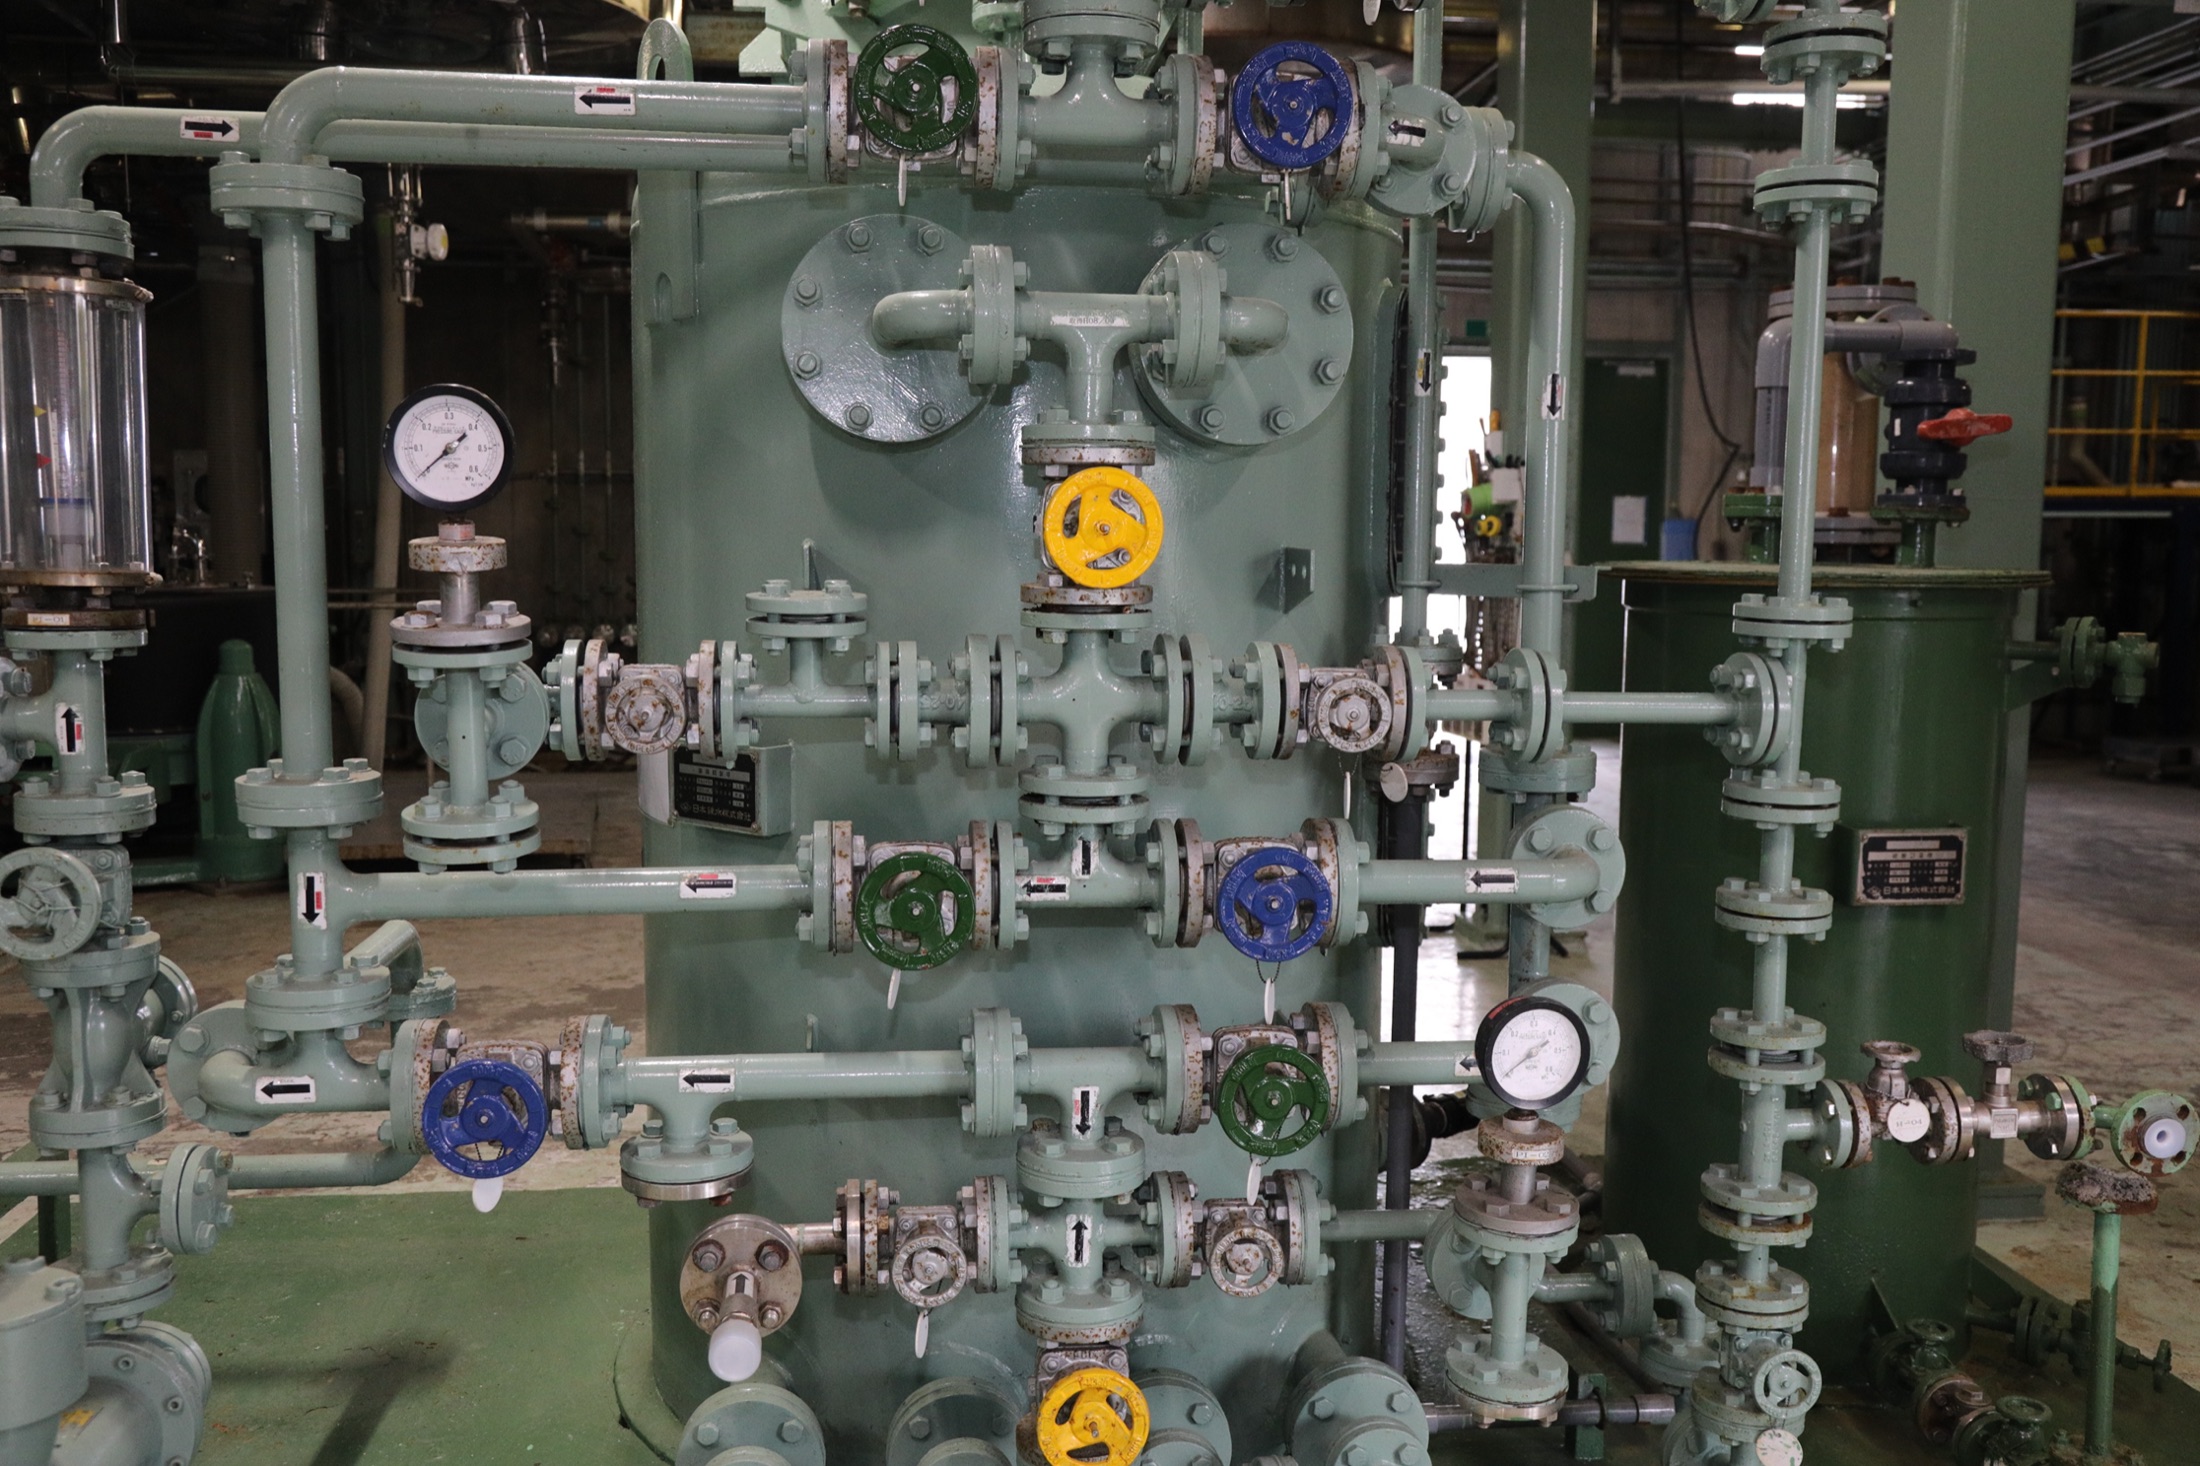
Column purification
We have carried out a substantial amount of column purification actions through the manufacture of electronic materials over many years and are confident that we can draw on our many years of experience to remove trace amounts of impurities.
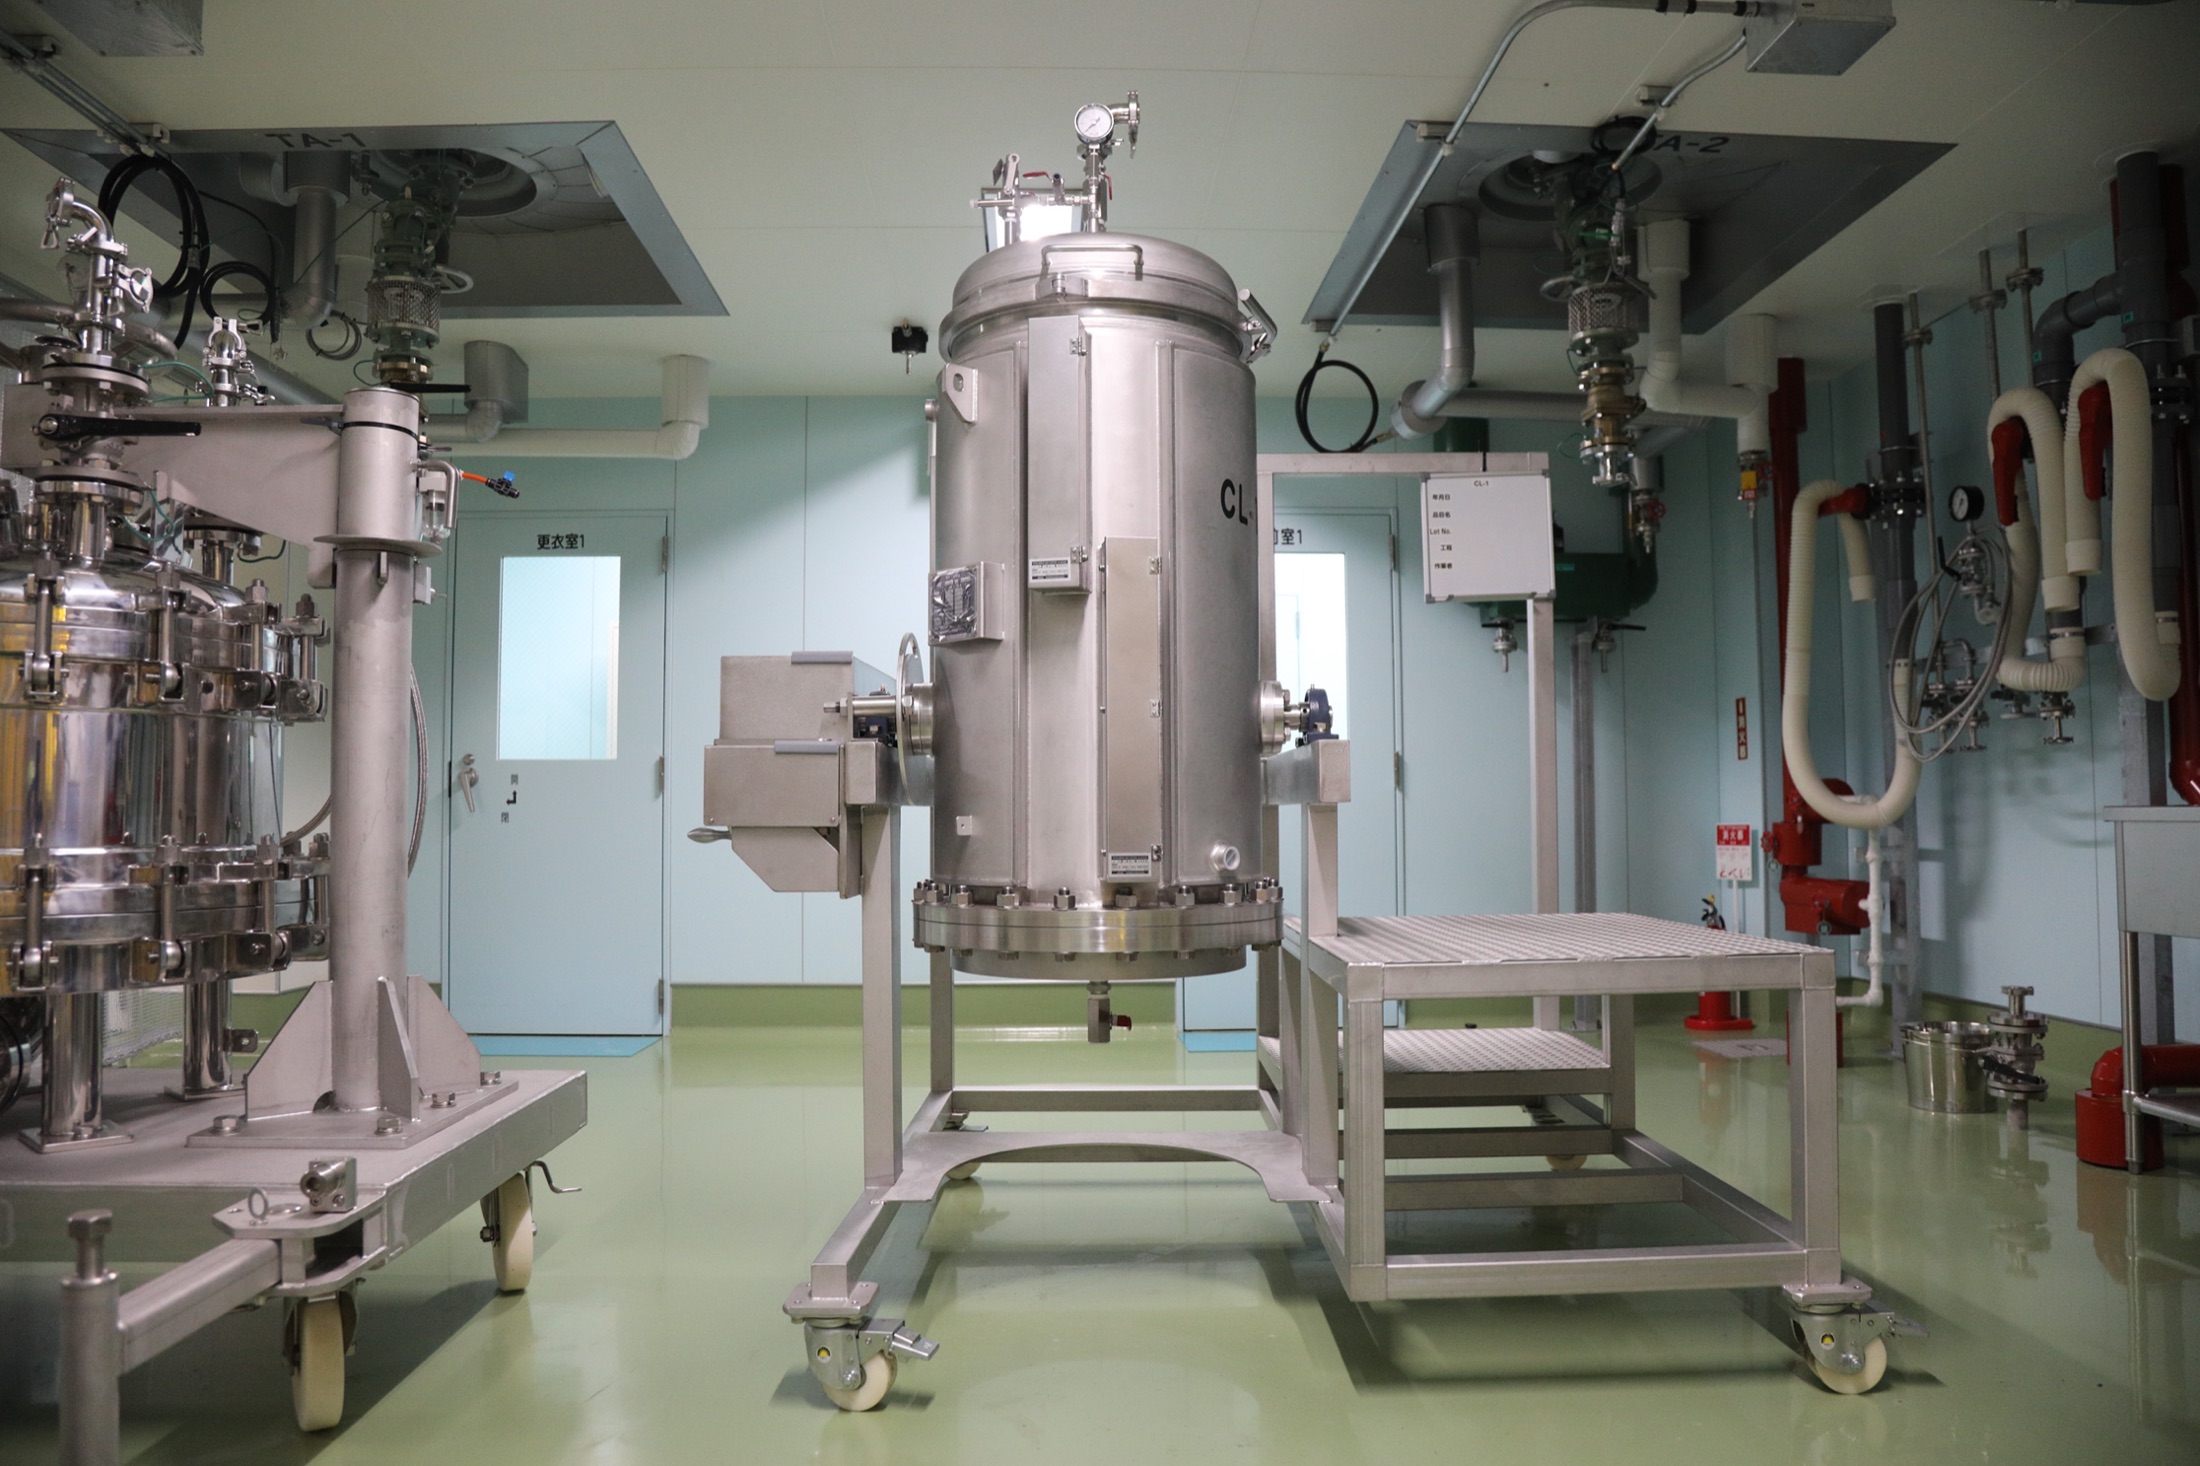
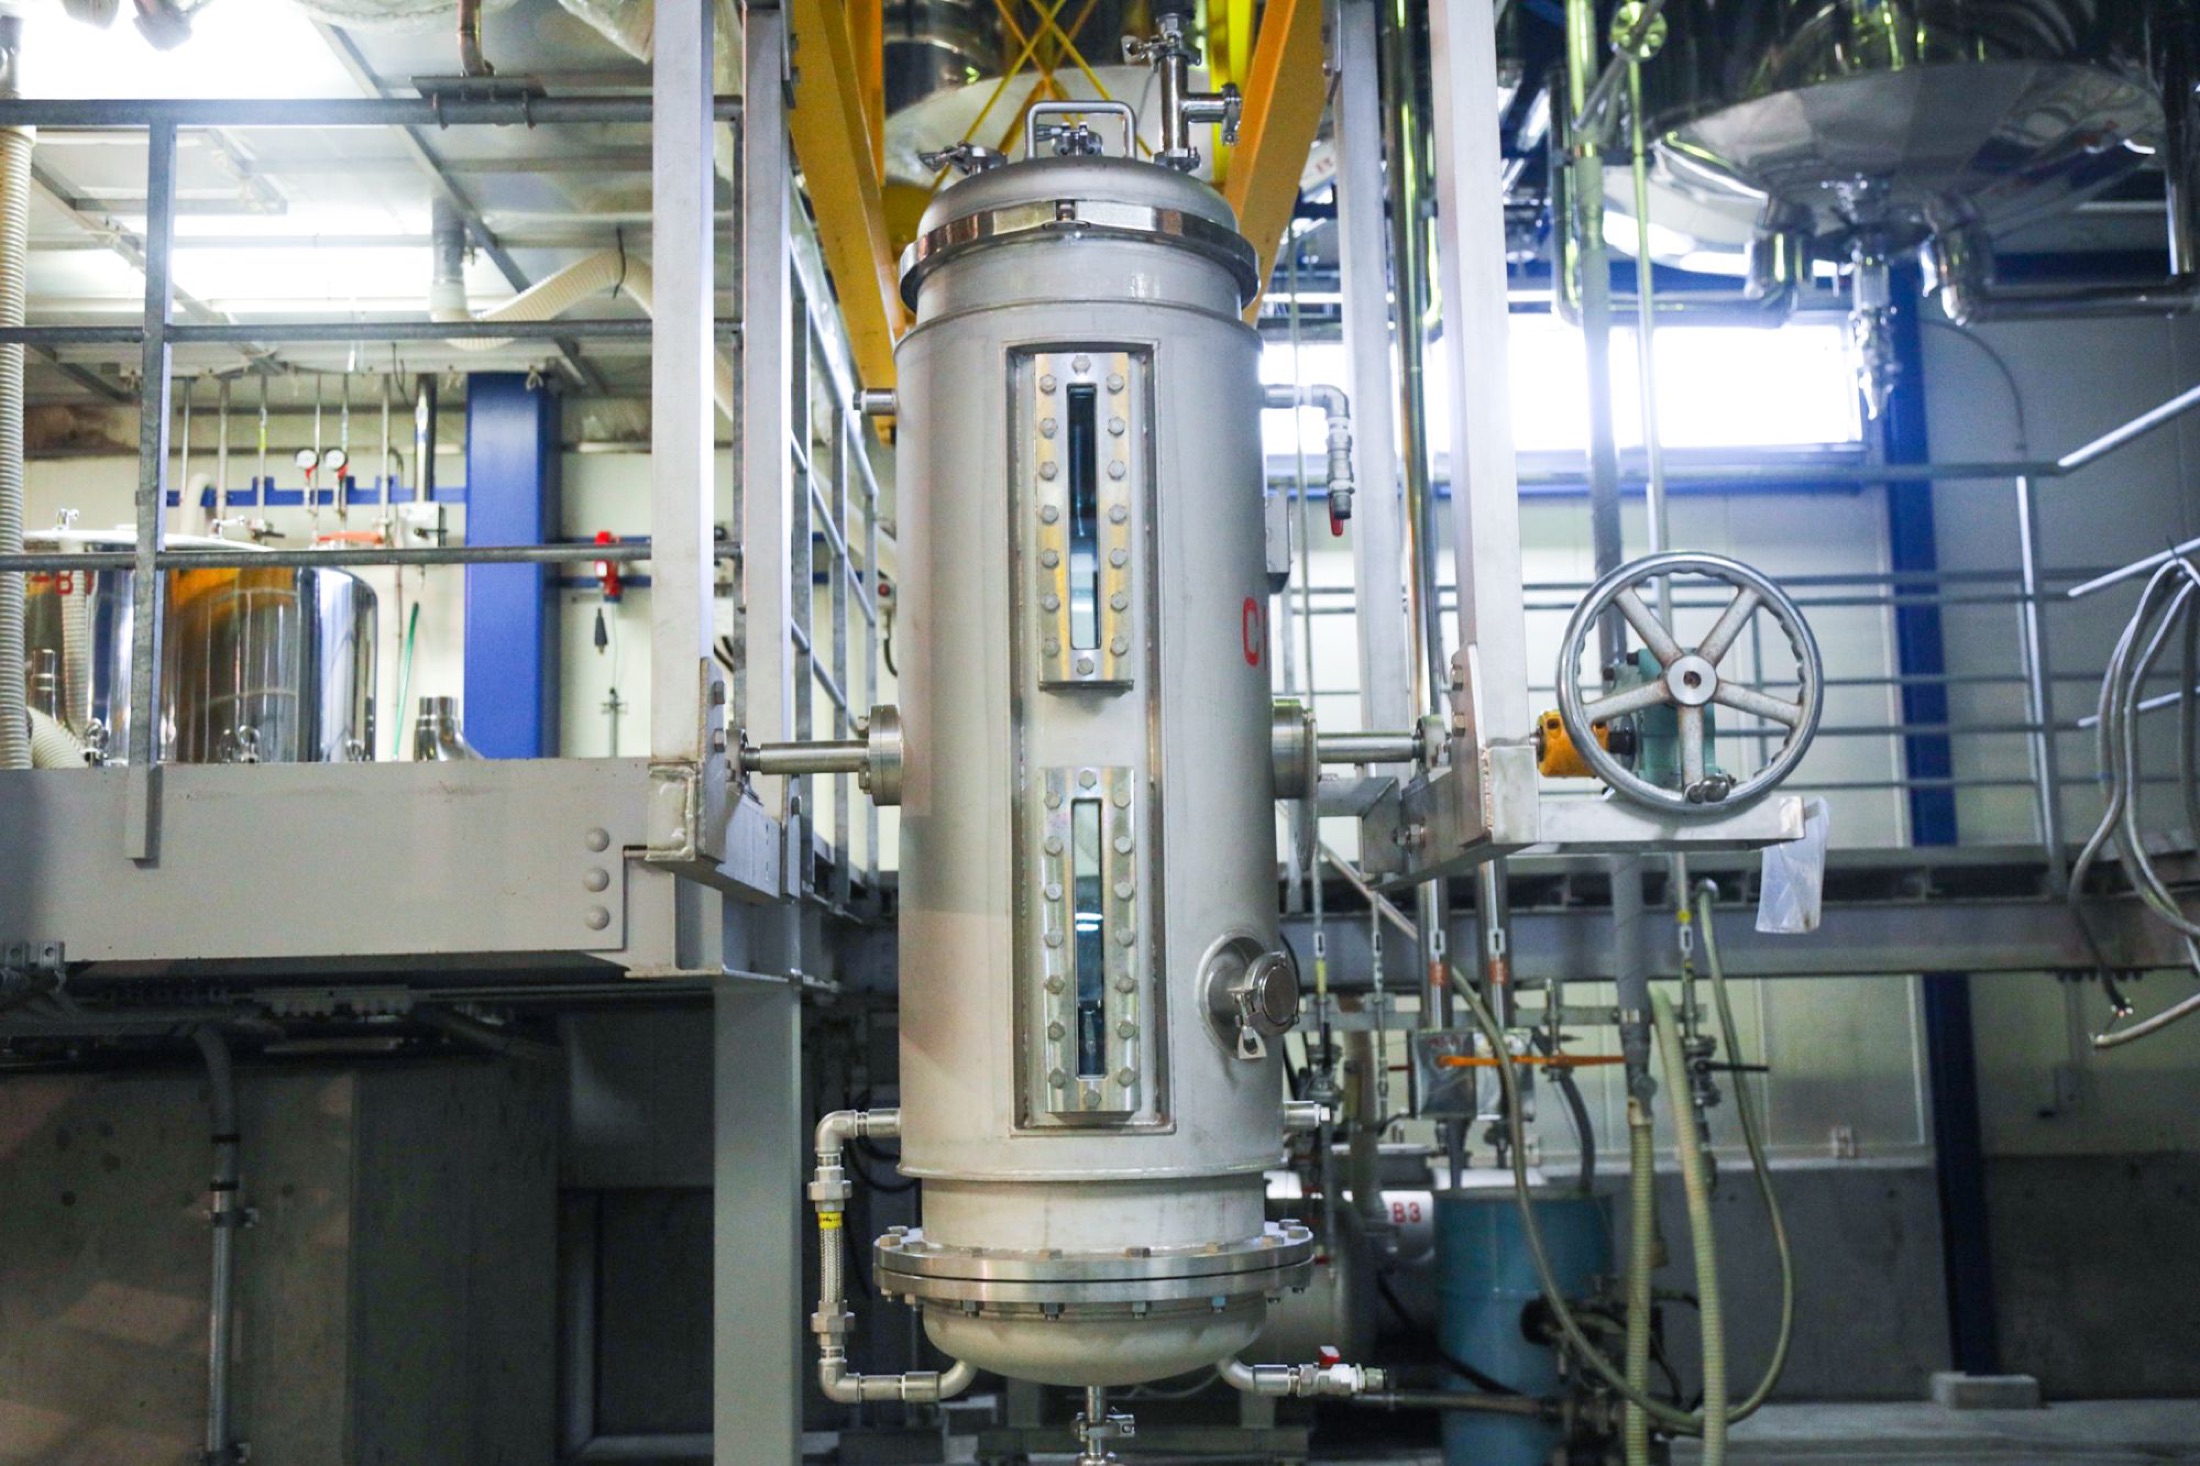
Fukuoka factory
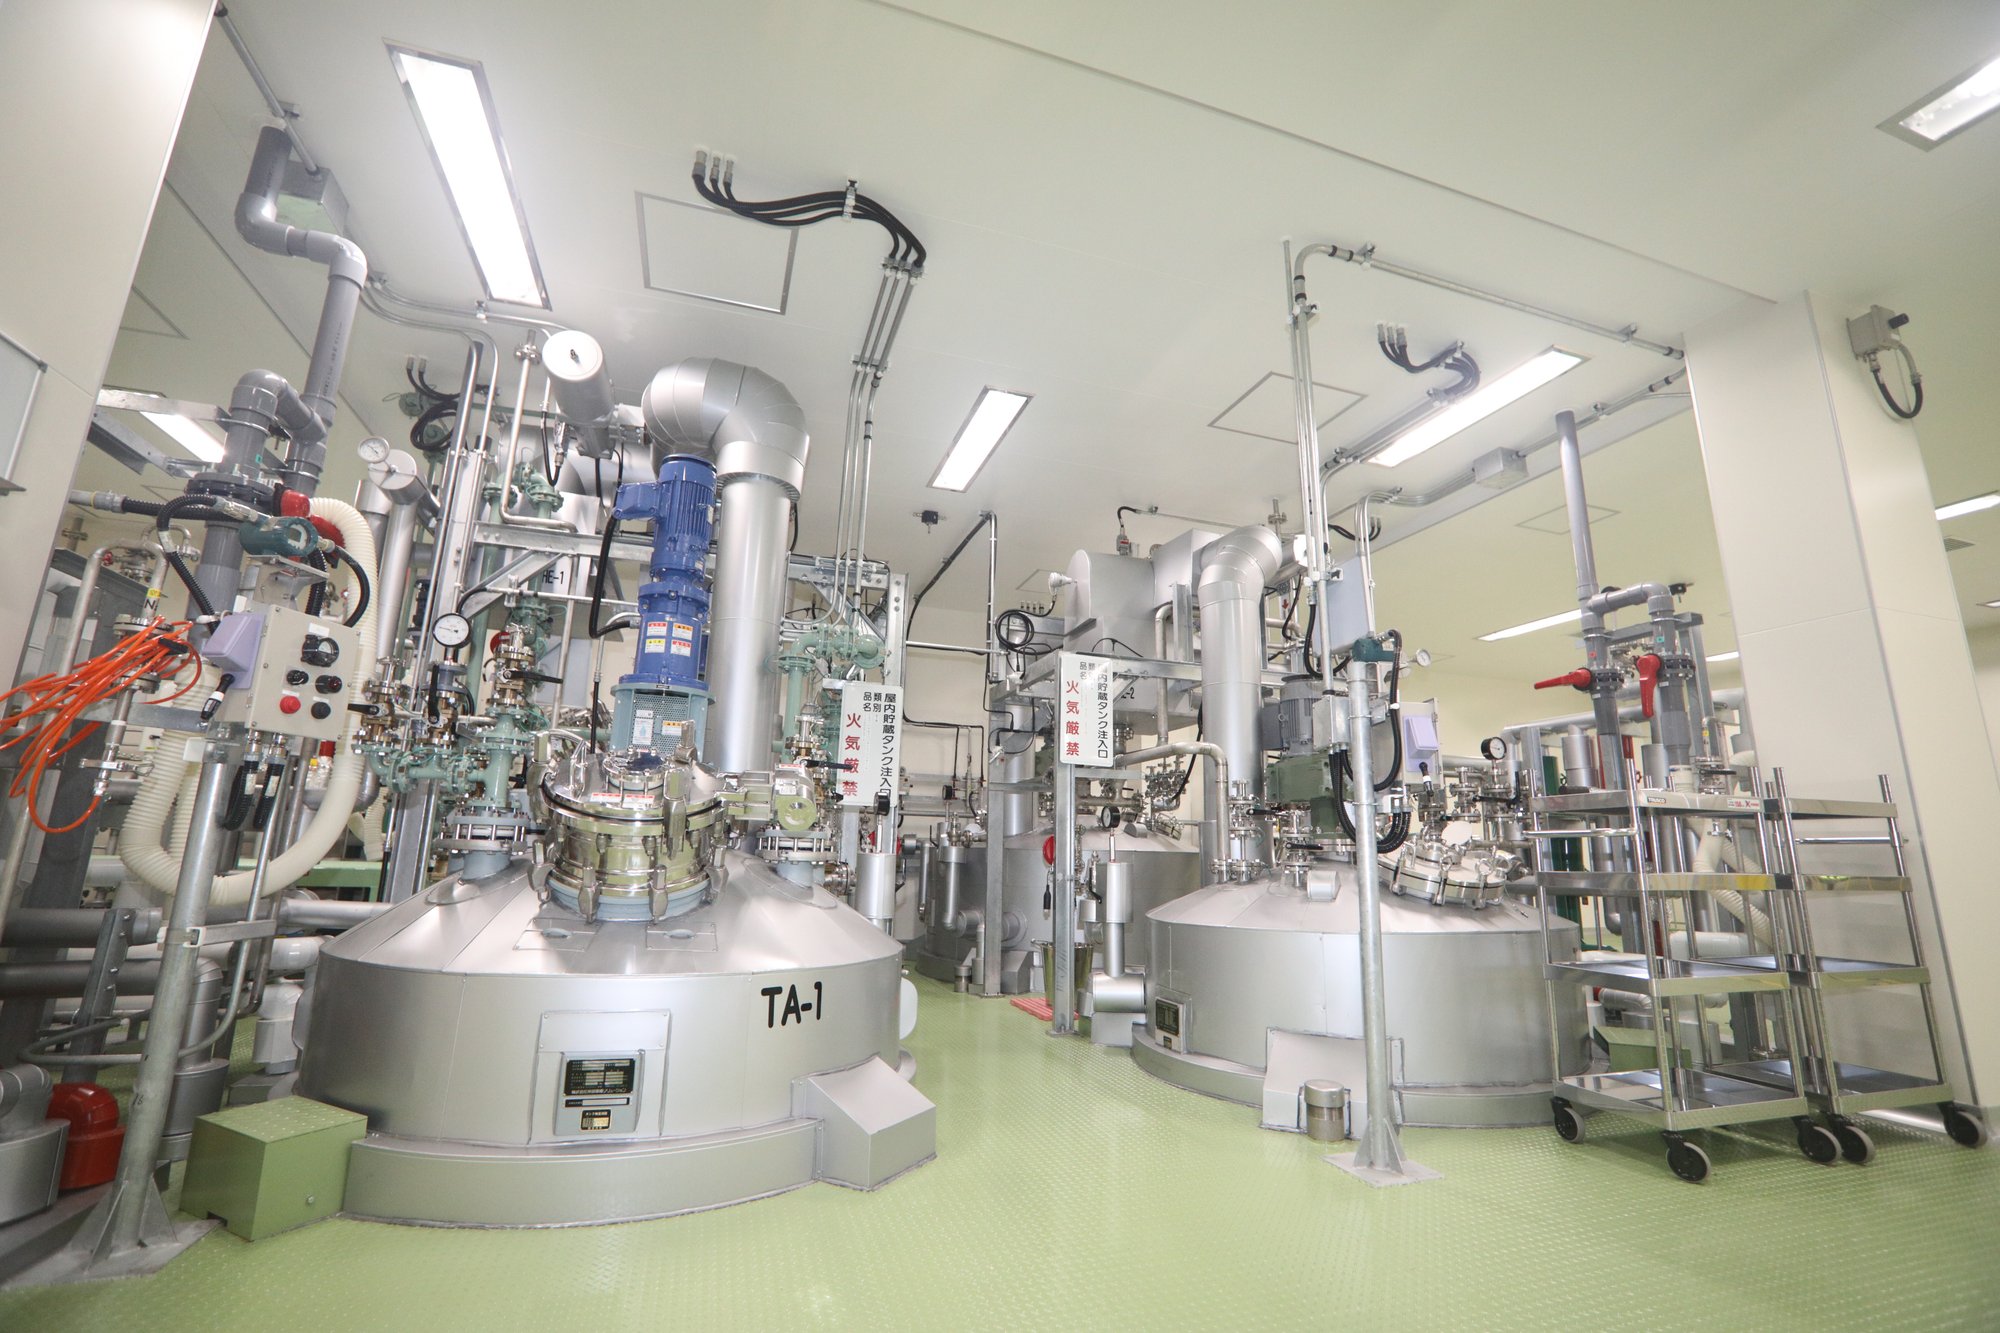
| Reactors | 200 L to 4,000 L GL reactors (49 units, of which 28 are dedicated to pharmaceutical applications), 200 L to 4,000 L SUS reactors (19 units, of which 12 are dedicated to pharmaceutical applications) |
|---|---|
| Specialized reaction apparatuses | 600 L GL photoreactor (1 unit), 200 L to 2,000 L GL oil-circulation reactors (5 units), 800 L and 2,000 L SUS oil-circulation reactors (2 units), 500 L SUS low-temperature reactor (1 unit) |
| Centrifuges | 36-inch Aflon-lined centrifuge (1 unit; 1 unit dedicated to pharmaceutical applications), 24-inch and 36-inch SUS centrifuges (3 units; 3 units dedicated to pharmaceutical applications), 36-inch Hastelloy-lined centrifuges (4 units; 1 unit dedicated to pharmaceutical applications), 42-inch rubber-lined centrifuge (1 unit; 1 unit dedicated to pharmaceutical applications) |
| Dryers | 1000 L to 2,000 L GL conical units (5 units; 4 units dedicated to pharmaceutical applications), 500 L SUS multi-tiered units (10 units; 4 units dedicated to pharmaceutical applications) |
| Purifiers | 100 L and 200 L column units (4 units), 150 L and 300 L ion-exchange resin towers (2 units), pressure filter units (7 units) |
| Others | Thin-film distillation units, sieving machines, micronizers, evaporators, QVF |
Iwaki Factory
| Reactors | 100 L to 4,000 L GL units (78 units, of which 58 are dedicated to pharmaceutical applications), 500 L to 2,000 L SUS units (27 units, of which 22 are dedicated to pharmaceutical applications) |
|---|---|
| Specialized reaction apparatuses | 100 L to 3,000 L GL oil-circulation reactors (5 units), 500 L SUS low-temperature reactor (1 unit) |
| Centrifuges | 36-inch and 42-inch Aflon-lined centrifuge (6 units; 5 units dedicated to pharmaceutical applications), 36-inch and 42-inch SUS centrifuges (7 units; 6 units dedicated to pharmaceutical applications), 36-inch and 42-inch Hastelloy-lined centrifuges (2 units; 2 units dedicated to pharmaceutical applications), 42-inch titanium-lined centrifuge (1 unit) |
| Dryers | 300 L to 2,000 L GL conical units (11 units; 11 units dedicated to pharmaceutical applications), 200 L SUS conical unit (1 unit; 1 unit dedicated to pharmaceutical applications), 1,000 L SUS vibrating unit (1 unit, 1 unit dedicated to pharmaceutical applications) |
| Purifiers | 70 L and 150 L column units (6 units); 600 L, 1,600 L, and 1,800 L ion-exchange resin towers (3 units); pressure filter units (4 units) |
| Others | Sieving machines, micronizers, evaporators, QVF |
Expanding the possibilities inherent in chemistry through technology.
We are engaged in everything from research and development work to manufacturing for a wide range of fine chemicals, including active pharmaceutical ingredients and intermediates, functional cosmetic ingredients, and advanced chemicals, by building on a foundation of organic synthesis technologies cultivated over many years.
Reduction Reactions
Oxidation Reactions
Carbon–Carbon Bond Formation Reactions
Others
The above examples are provided for illustrative purposes; other types of synthesizing jobs can also be accommodated. Contact the Marketing Department for more information.
We can remove trace amounts of specific impurities found in products by using our proprietary purification technology. Higher levels of purity and quality are achieved by leveraging our advanced purification technology and extensive experience.
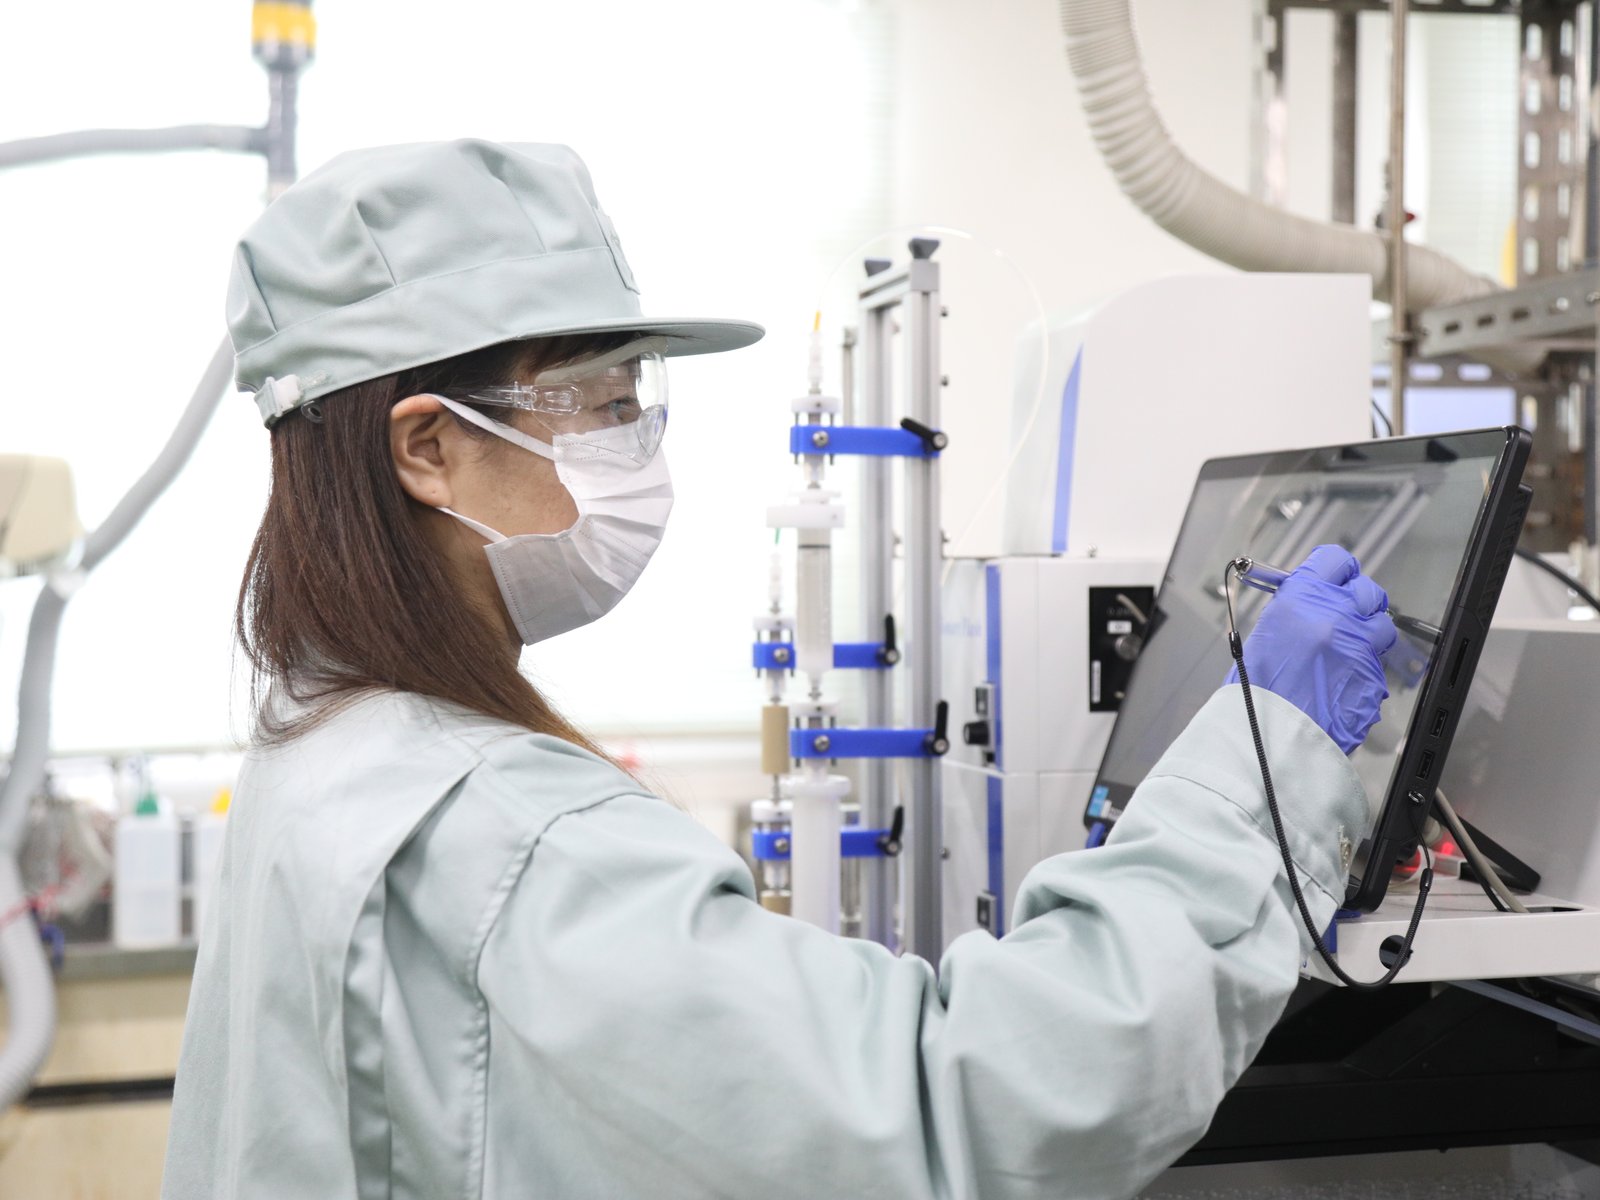
Even ingredients that are generally difficult to handle and specialized ingredients that tend to be avoided can be used and manufactured by leveraging our extensive experience and skills.
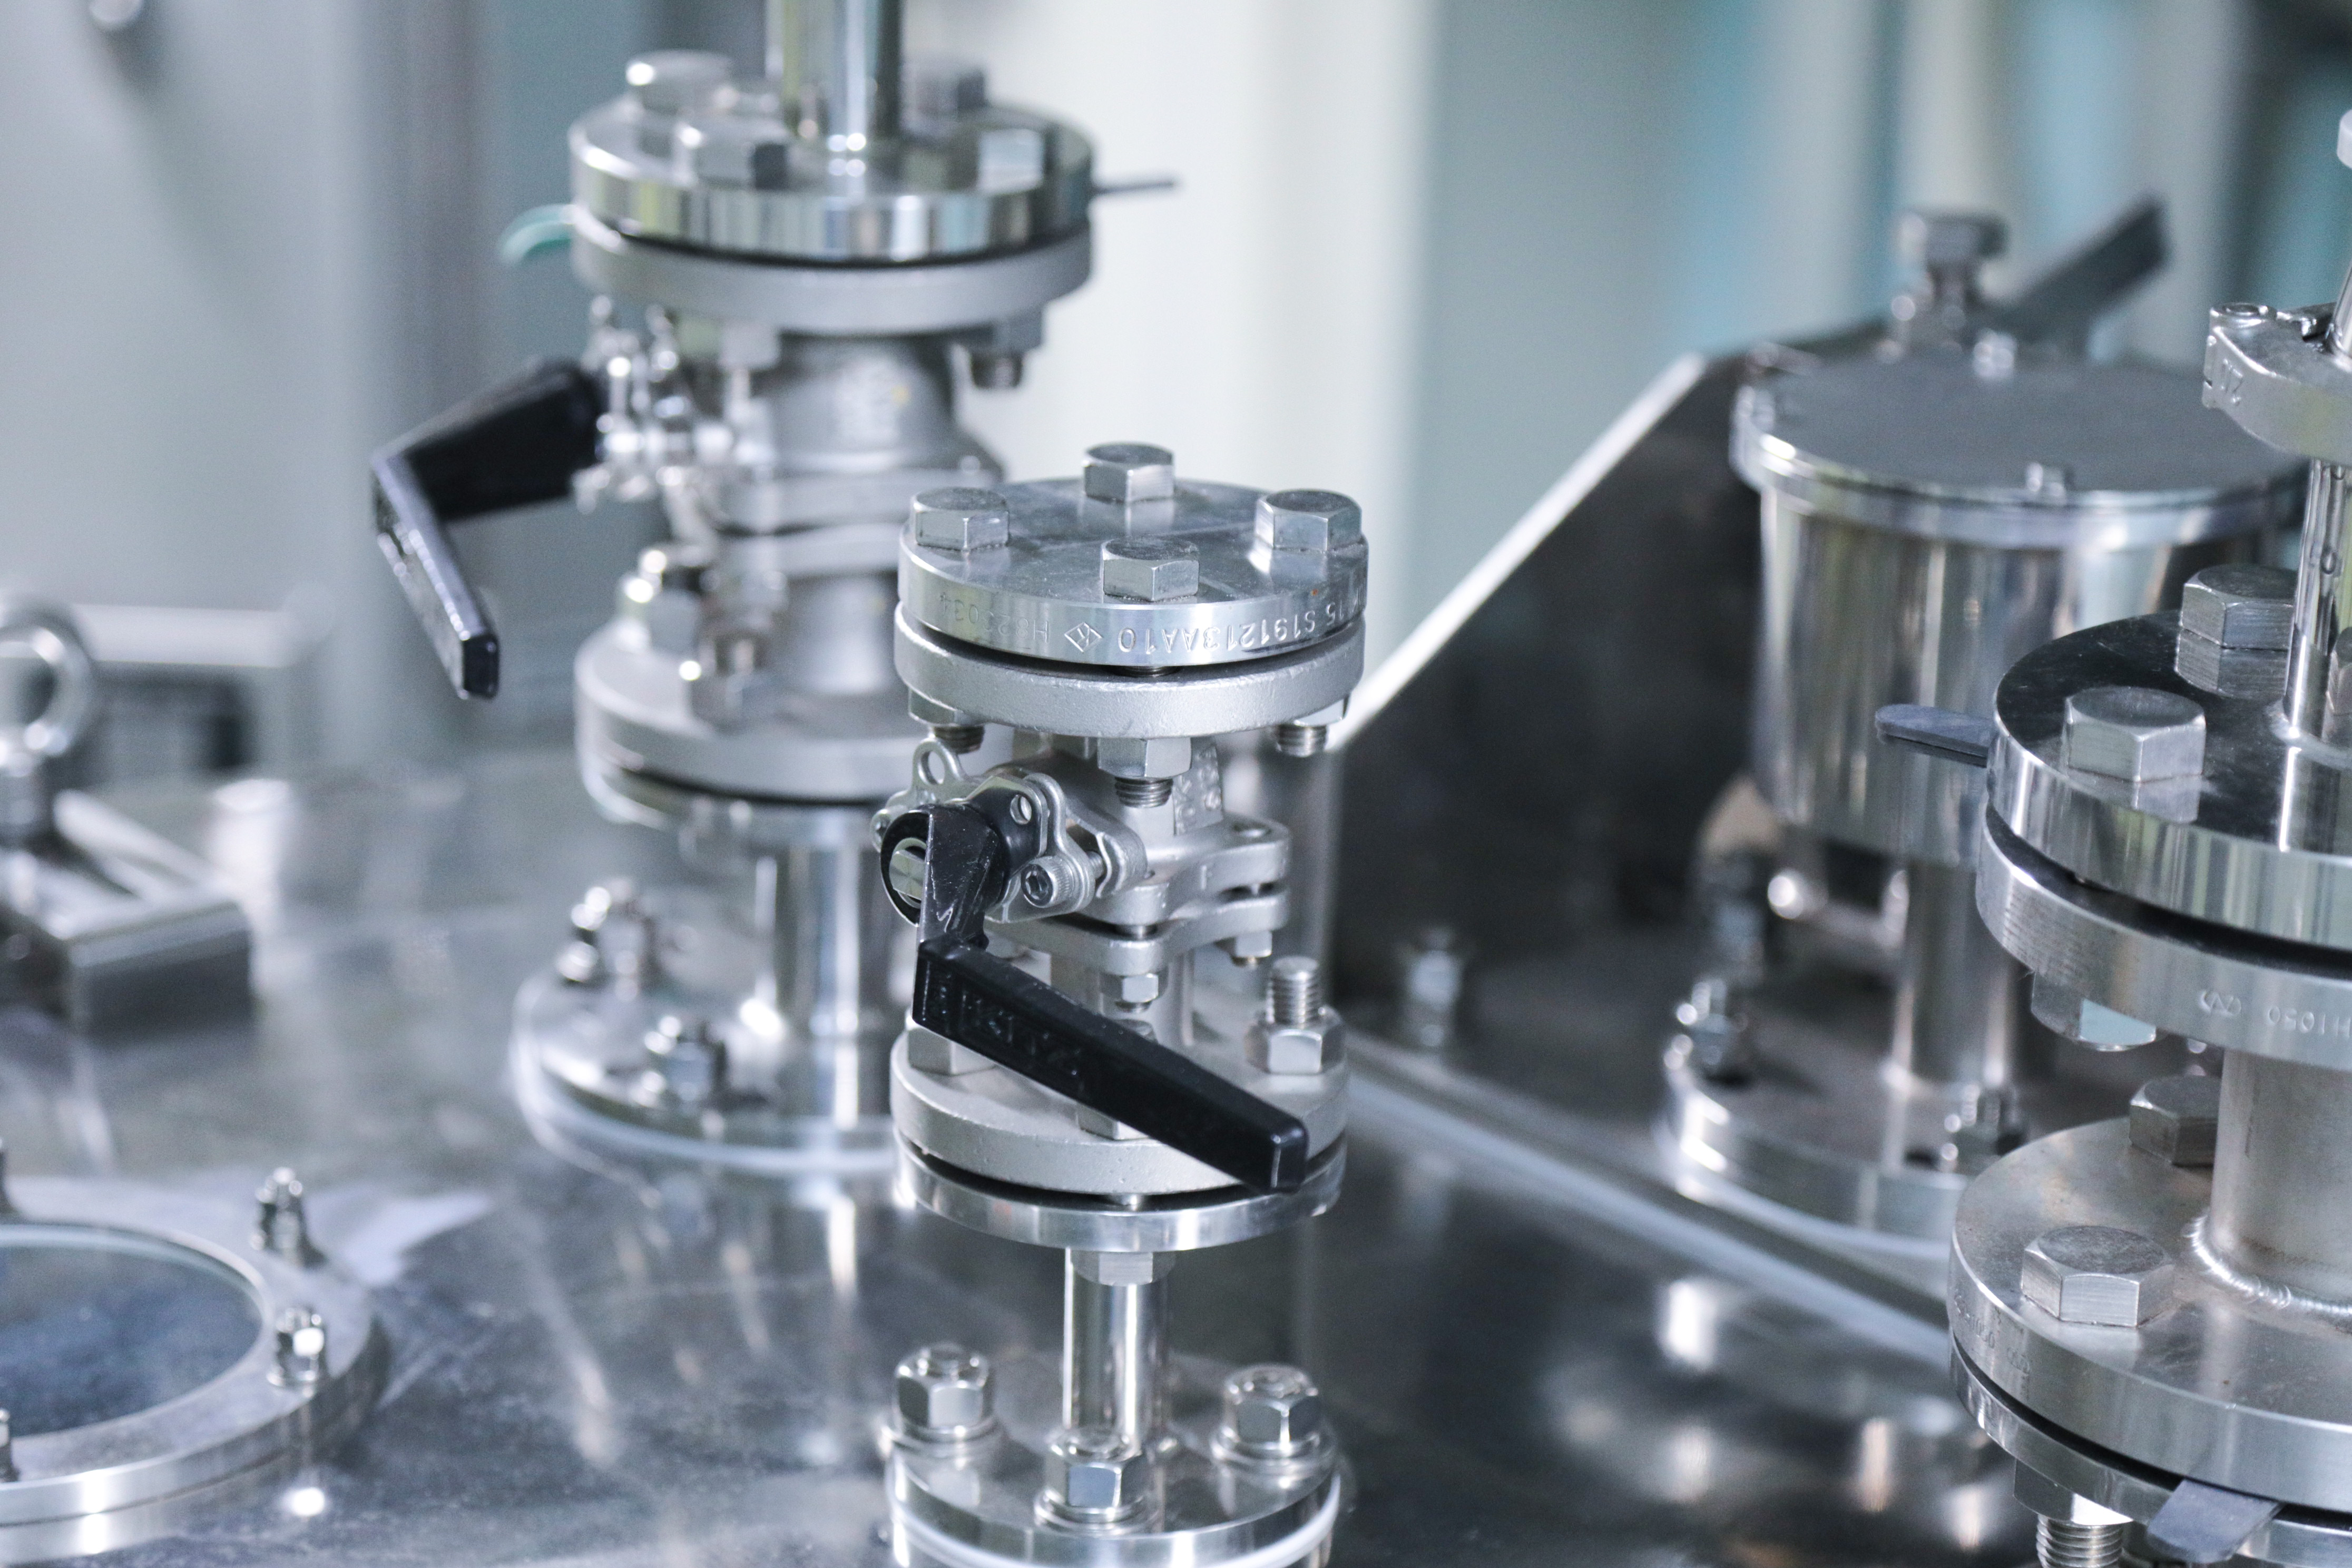
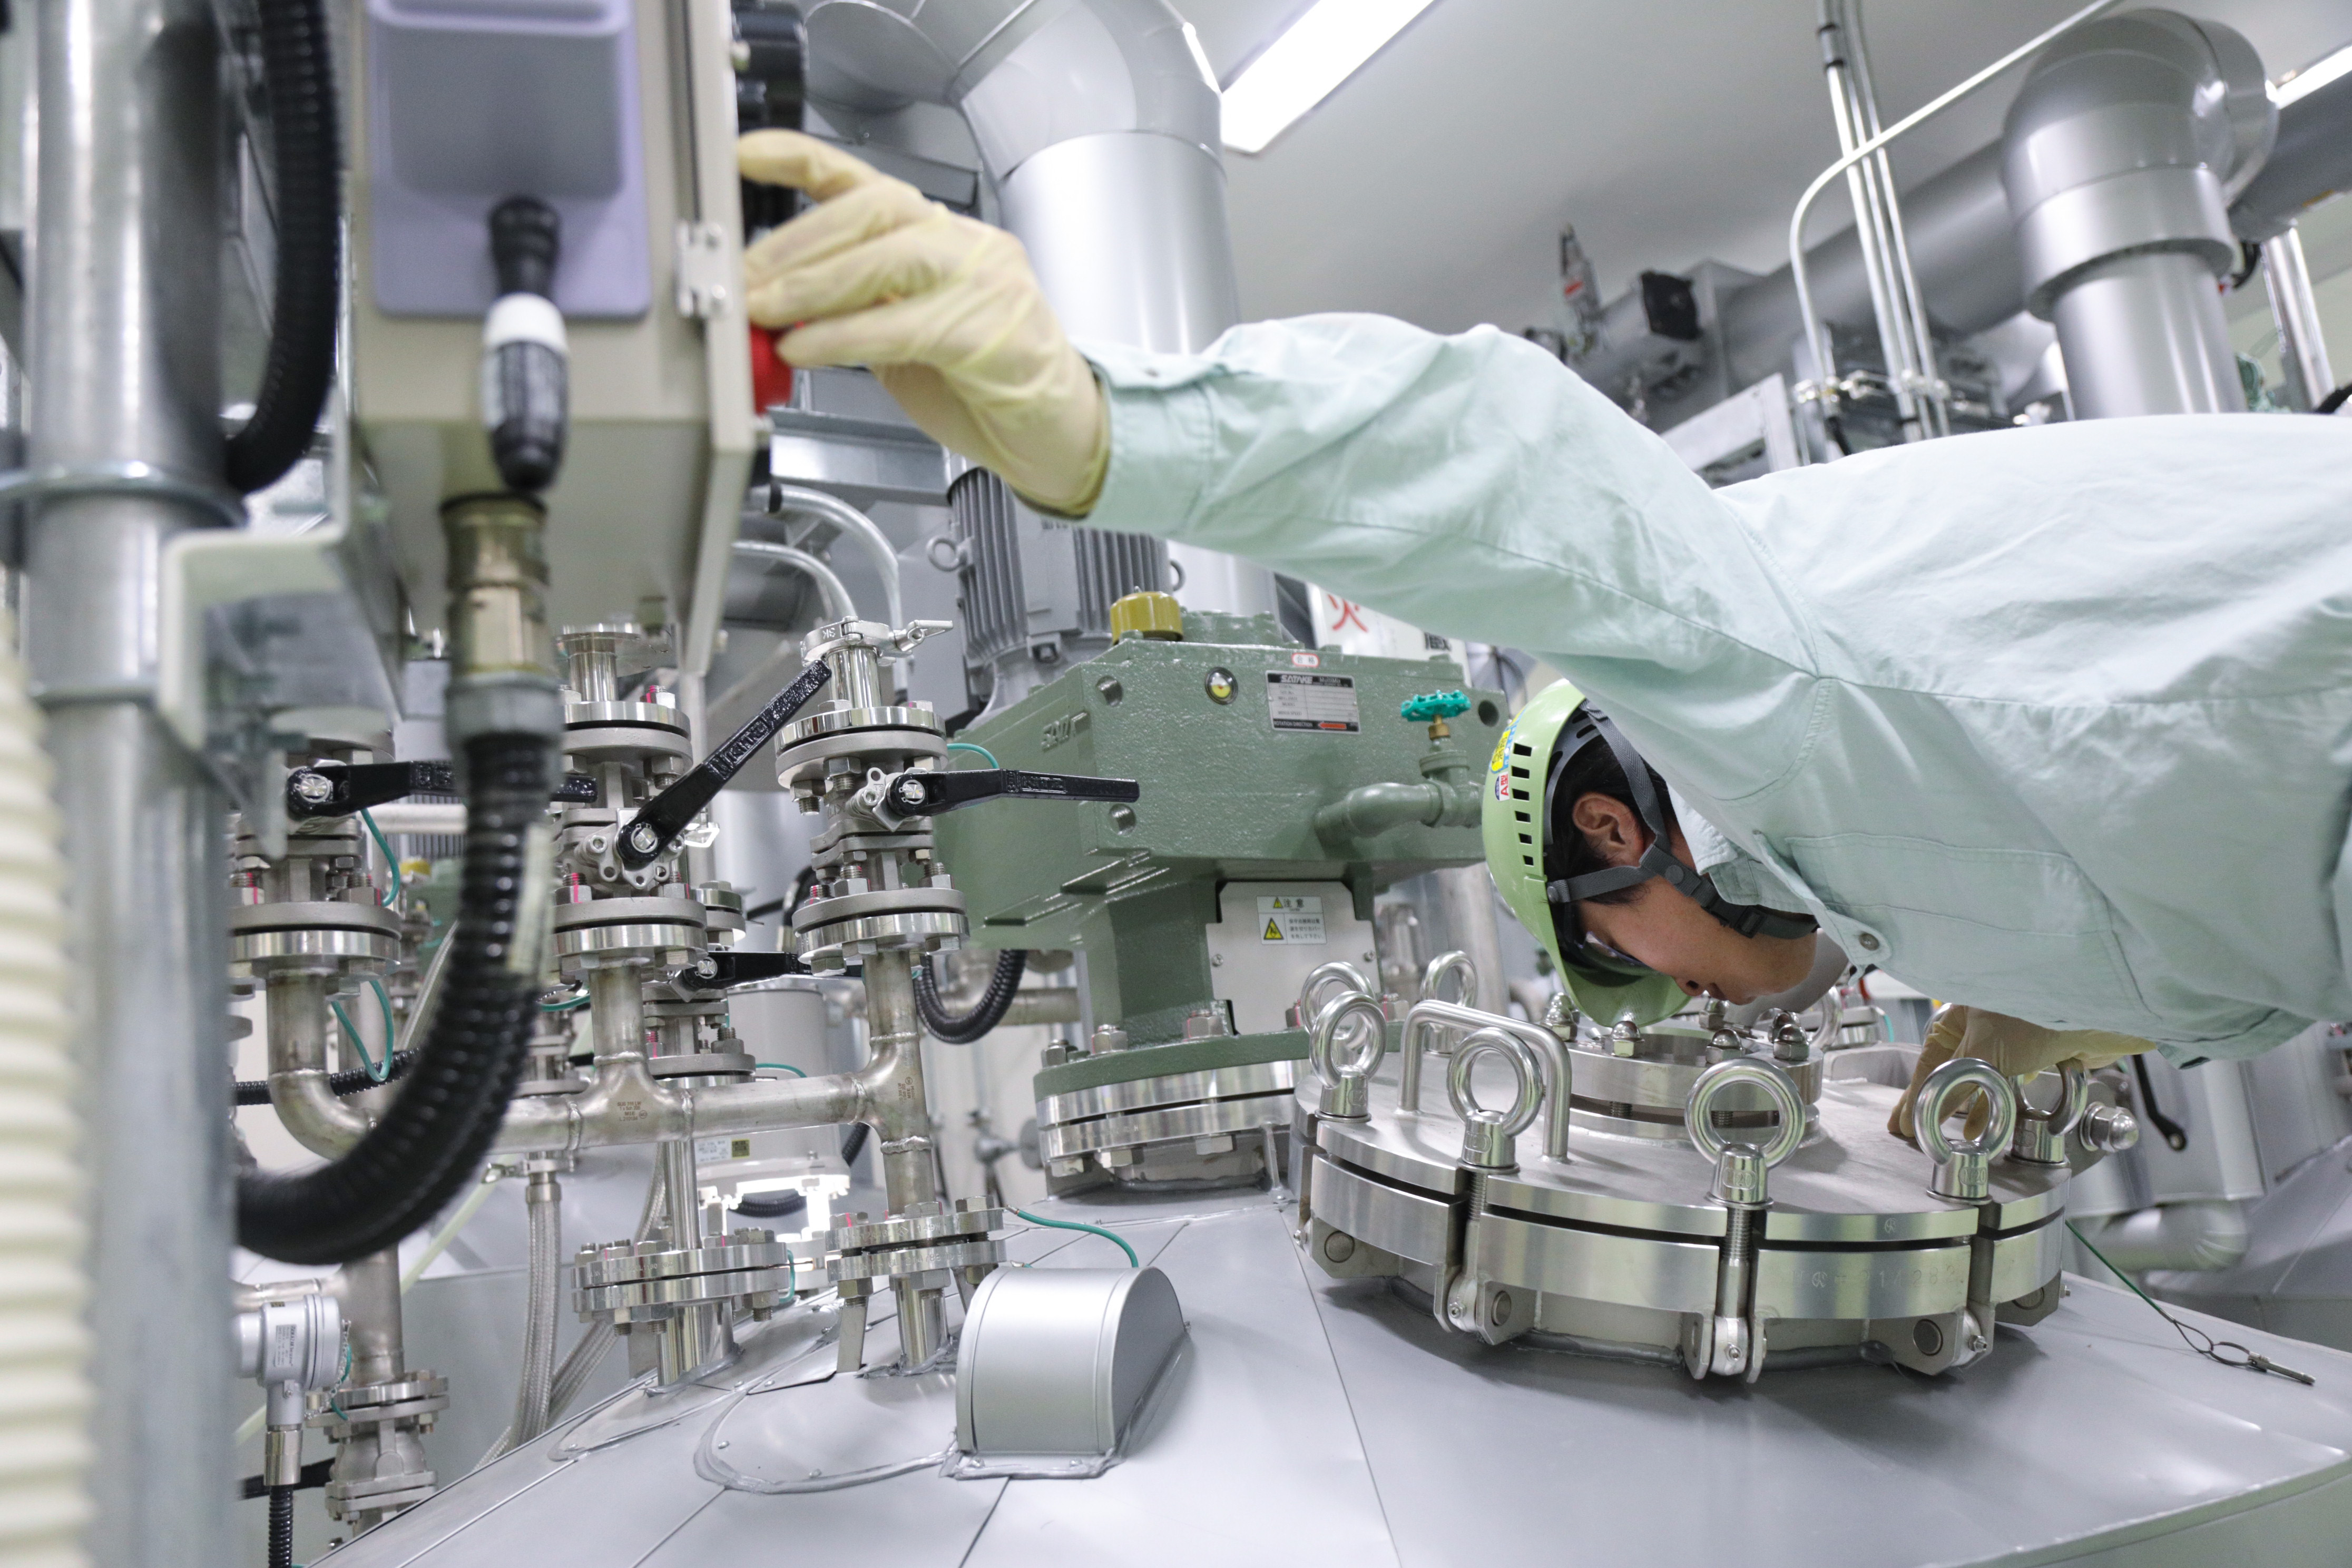
In addition to manufacturing on a contracted basis, we also engage in research and development work for the future by drawing on synthesis technologies that we have spent many long years cultivating.
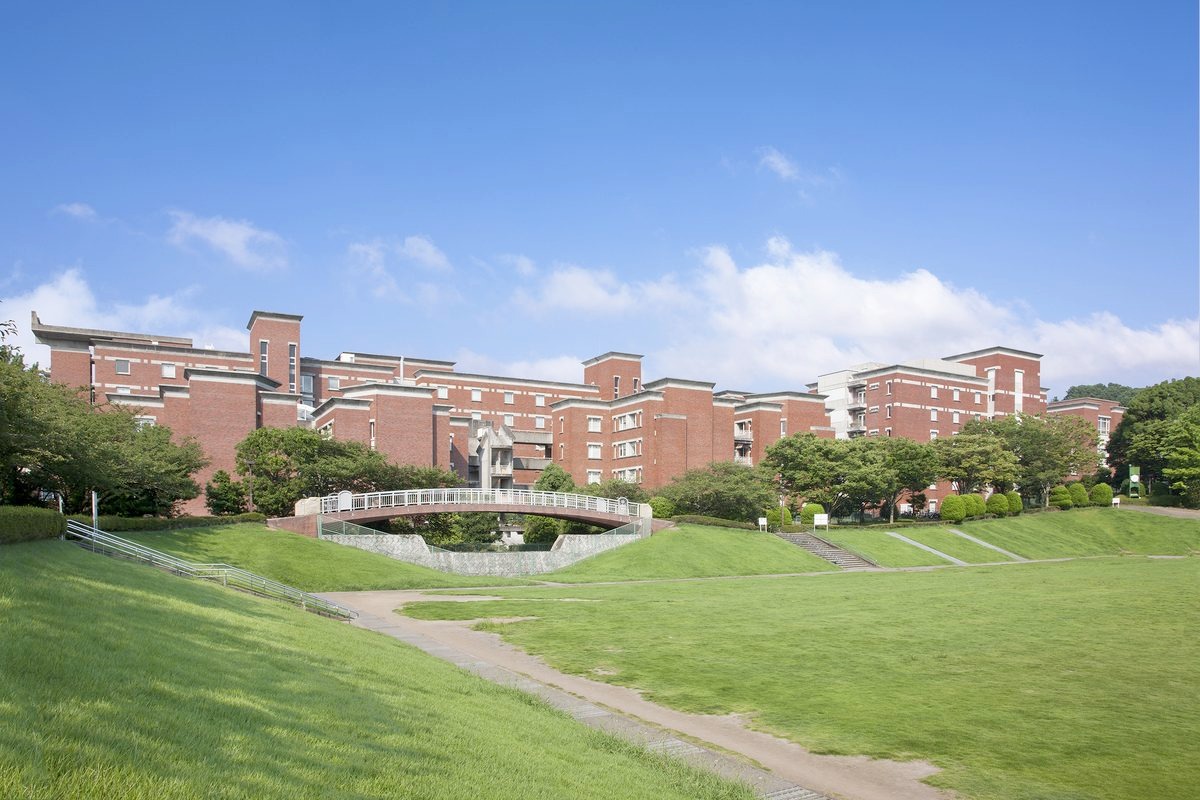
We are engaged in the joint research of drug delivery systems (DDS) with the School of Pharmaceutical Sciences at the University of Shizuoka and have taken on the challenge of figuring out how to bring oligonucleotide therapeutics, mRNA vaccines, and other new modalities to market together with other universities, hospitals, pharmaceutical companies, and venture enterprises.
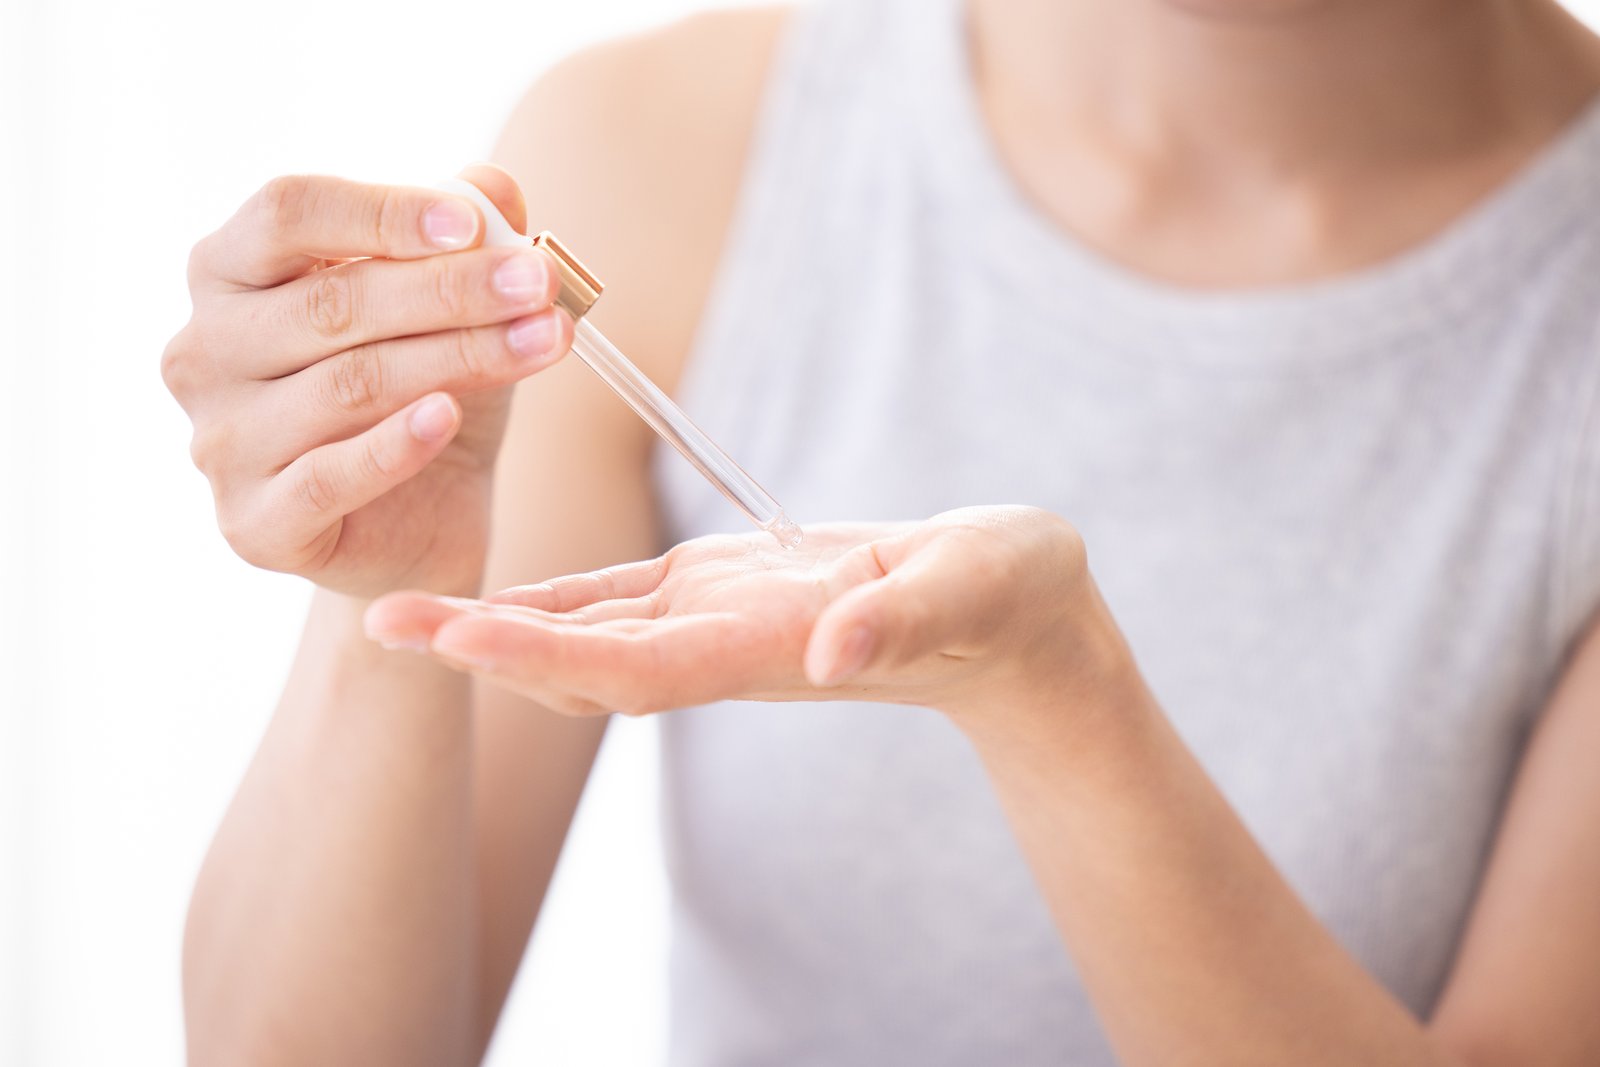
We have developed proprietary ingredients, such as skin-brightening agent Calcium D-Pantetheine-S-sulfonate70 and anti-aging agents Thiotaurine and Hypotaurine, and are selling them to domestic and overseas cosmetics companies. We will continue to try developing ingredients consisting of unique bioactive components.
Addressing our clients’ challenges and pursuing better manufacturing methods
Contract manufacturing gives rise to a wide range of challenges, such as “The manufacturing conditions have not been established,” “It works in the lab, but scaling up is difficult,” and “We want to further improve yield and quality.”
To address these challenges, we verify manufacturing conditions and processes one by one and consider improvements from the standpoints of both quality and productivity.
Drawing on the experience and technologies we have cultivated through our manufacturing operations, we share challenges with our clients and work toward more stable manufacturing methods and higher productivity. We believe that this is our role in contract manufacturing.
Here we introduce examples of improvements that we have actually worked on together with our clients.
Company A (a chemical materials manufacturer) had synthesized samples on a scale of several tens of grams, which were being evaluated by the end user, when adoption was suddenly decided. Evaluation of product manufactured using actual production facilities was urgently required, making it necessary to quickly produce batches of several tens of kilograms. In addition, production on a commercial scale in batches of several hundred kilograms had to be anticipated within six months.
After receiving the project, we conducted small-scale experiments and, following about one month of study, carried out small-scale production using actual production facilities. Through multiple small lots and repeated improvements and refinements, we established the manufacturing method. As a result, we manufactured 100 kg of the product according to the schedule requested by the client, with no issues in either yield or quality.
Company B (a pharmaceutical company) requested the manufacture of a new API candidate prior to clinical trials. With the synthesis method disclosed to us, many impurities formed in each reaction, and the handling of intermediates and the purification yield were not stable. In addition, the manufacturing process was based on laboratory study and had not been designed with future industrial-scale production in mind, making it difficult to manufacture production using actual production facilities.
By identifying the causes of impurity formation in each reaction, optimizing reaction conditions and catalyst amounts to suppress impurities, and establishing appropriate storage conditions, we stabilized product quality and achieved excellent product quality. At the same time, we reviewed the operations of each process step, achieving significant cost reductions. Furthermore, by addressing scale-up challenges through laboratory studies, we established reaction conditions and process operations suitable for production using actual production facilities, thereby developing a reliable manufacturing process.
In the manufacturing flow developed by Company C (a chemical materials manufacturer), heat generation during the reaction was difficult to control, and sudden exotherms posed a safety problem. In addition, large amounts of insoluble impurities formed during the reaction, requiring a filtration step after the reaction to remove them, which was a challenge for scale-up.
Changing the reaction catalyst made stable reaction control possible and dramatically improved safety. By-product impurities were also suppressed, and the simplified filtration step enabled a substantial increase in lot scale, greatly contributing to cost reduction.
The critical mission that we must fulfill is to reliably provide client-trusted products through the manufacture and contract manufacturing of active pharmaceutical ingredients, intermediates, and investigational drugs; advanced chemicals; functional cosmetic ingredients; and other products. In order to ensure the quality of our manufactured products, we have established a quality-assurance system based on cGMP concepts and appropriately manage all steps in the process, from the acceptance of raw materials to manufacturing, quality testing, storage, and delivery. We also work to achieve continuous improvements by having each and every employee feel a sense of responsibility for the quality of what we provide.
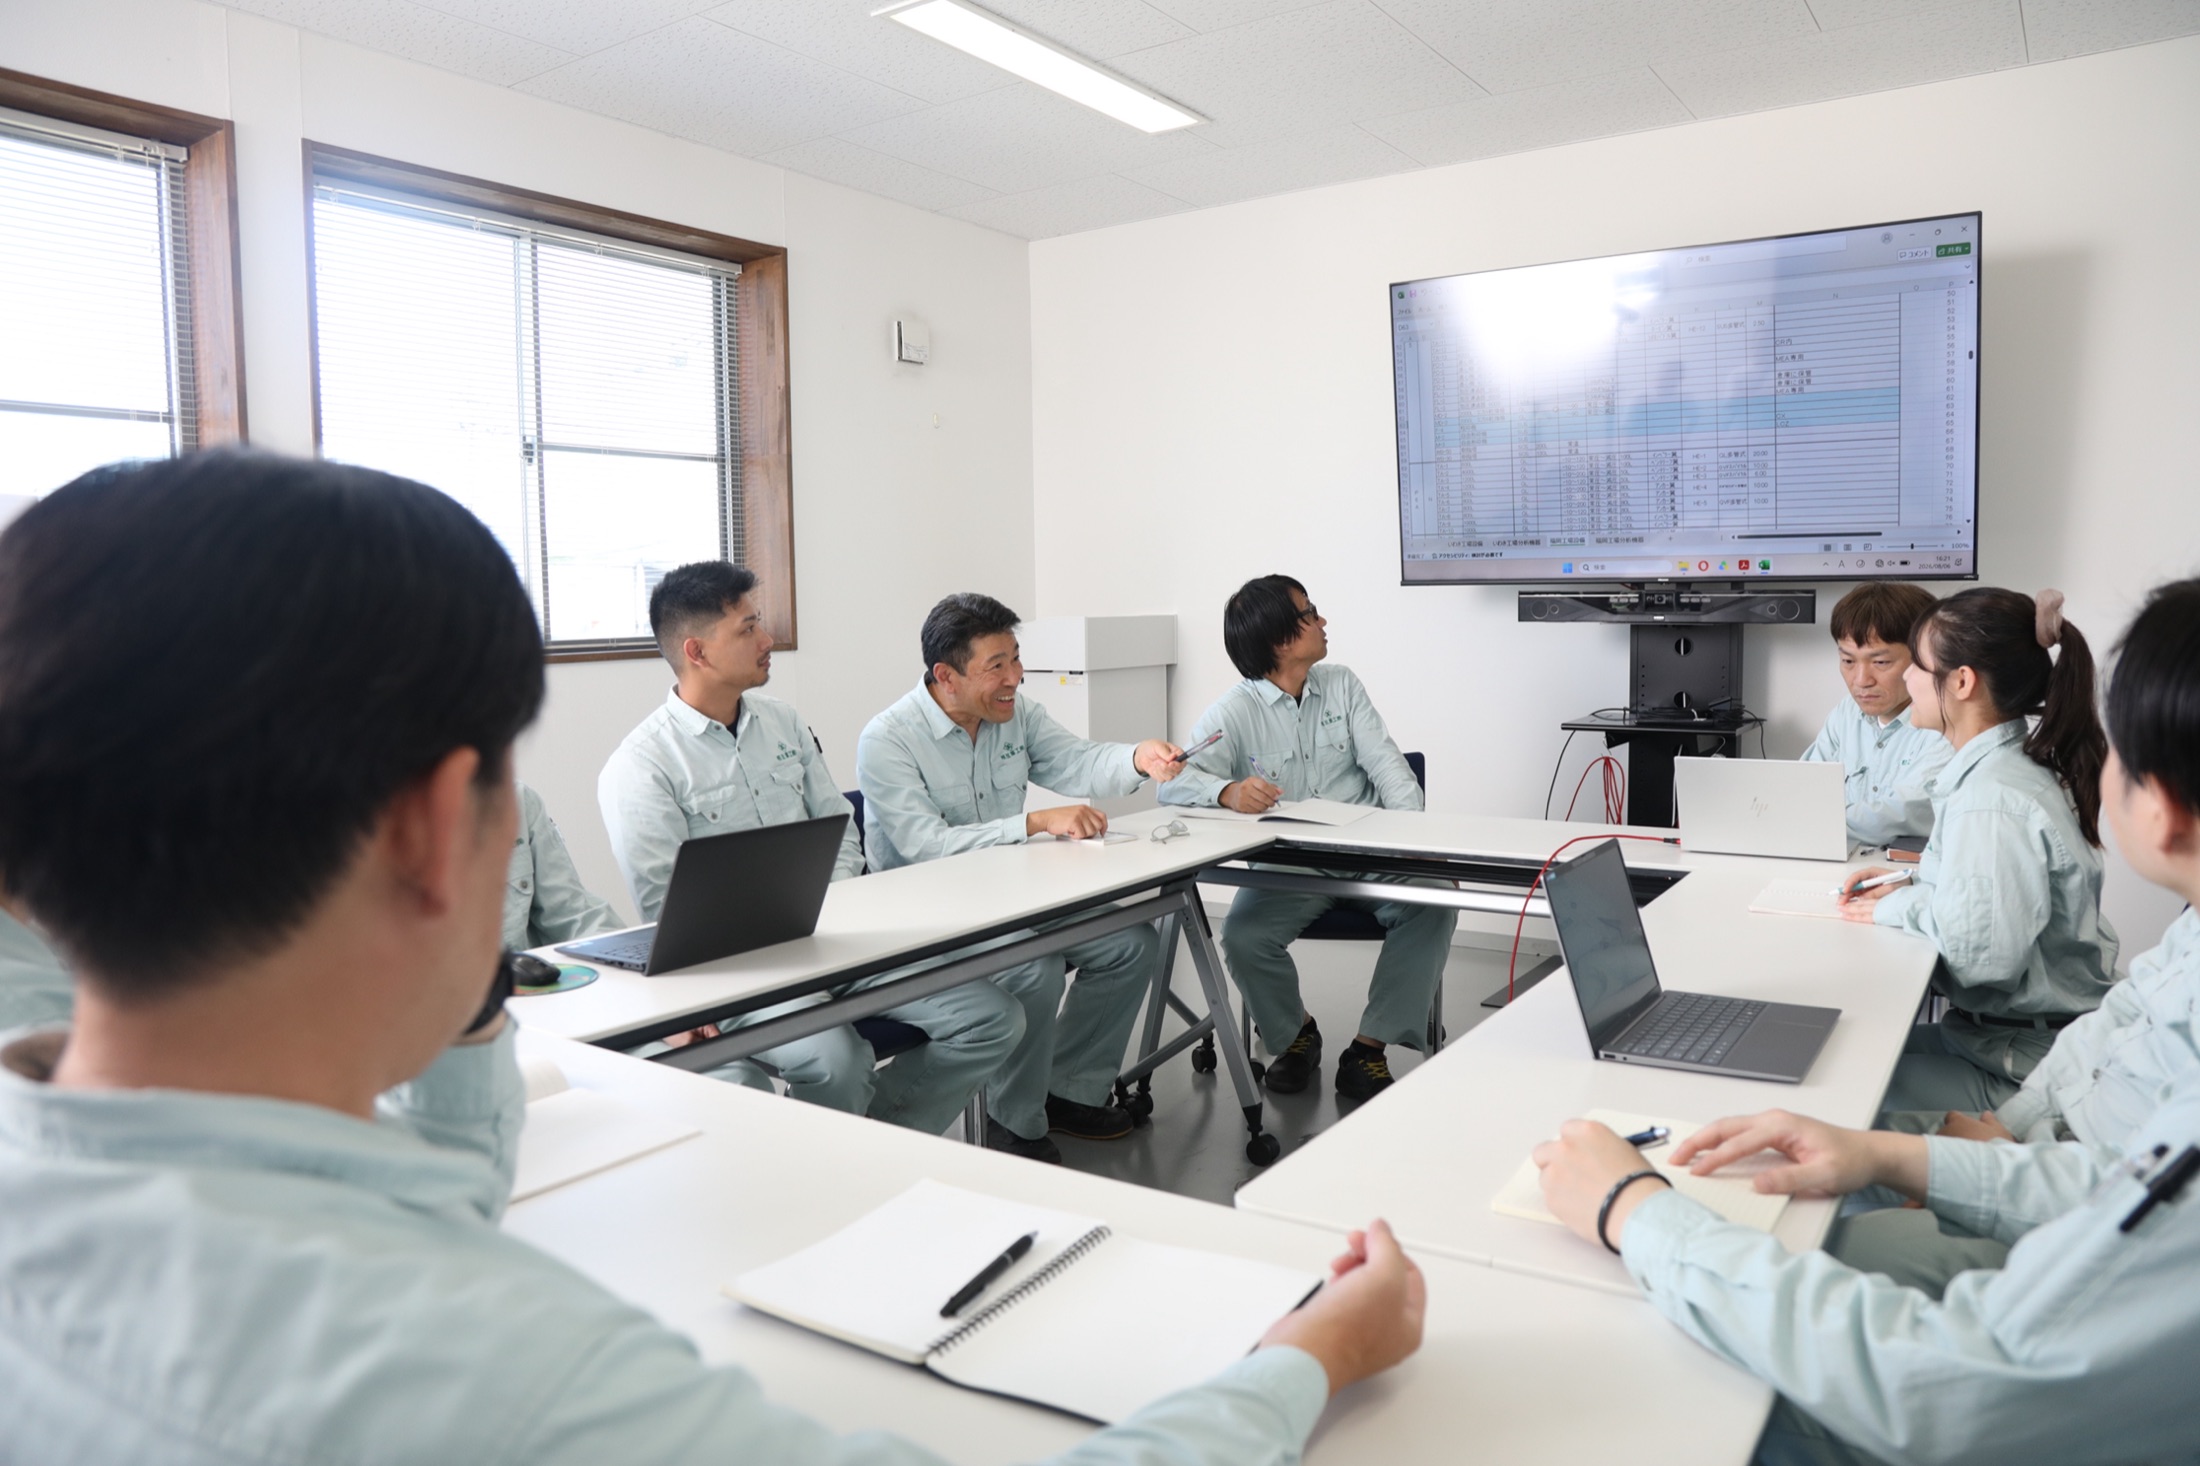
Based on cGMP concepts, the Manufacturing Department and Quality Department have clarified their respective responsibilities and roles and work to ensure product quality while collaborating with one another. We carry out a wide range of quality-assurance activities encompassing not just the appropriate management of everything from the acceptance of ingredients to product testing and delivery approval but also measures designed to ensure data integrity.
Receipt of Raw Materials
Supplier Qualification and Management / Receipt Inspection
Testing of Incoming Materials
Hygiene and Sanitation Control / Sampling / Testing
Storage and Issuance
Hygiene and Sanitation Control / Inventory Control
Manufacturing
Hygiene and Sanitation Control / Issuance of Production Batch Records / In-Process Control
Finished Product Testing
Hygiene and Sanitation Control / Sampling / Testing
Storage
Hygiene and Sanitation Control / Inventory Control
Shipment Authorization
Review of Production Batch Records and Analytical Records / Review of Deviations, Changes, Out-of-Specification (OOS) Results, etc.
Distribution of Finished Products
Only Quality-Assured Products Are Supplied to Customers
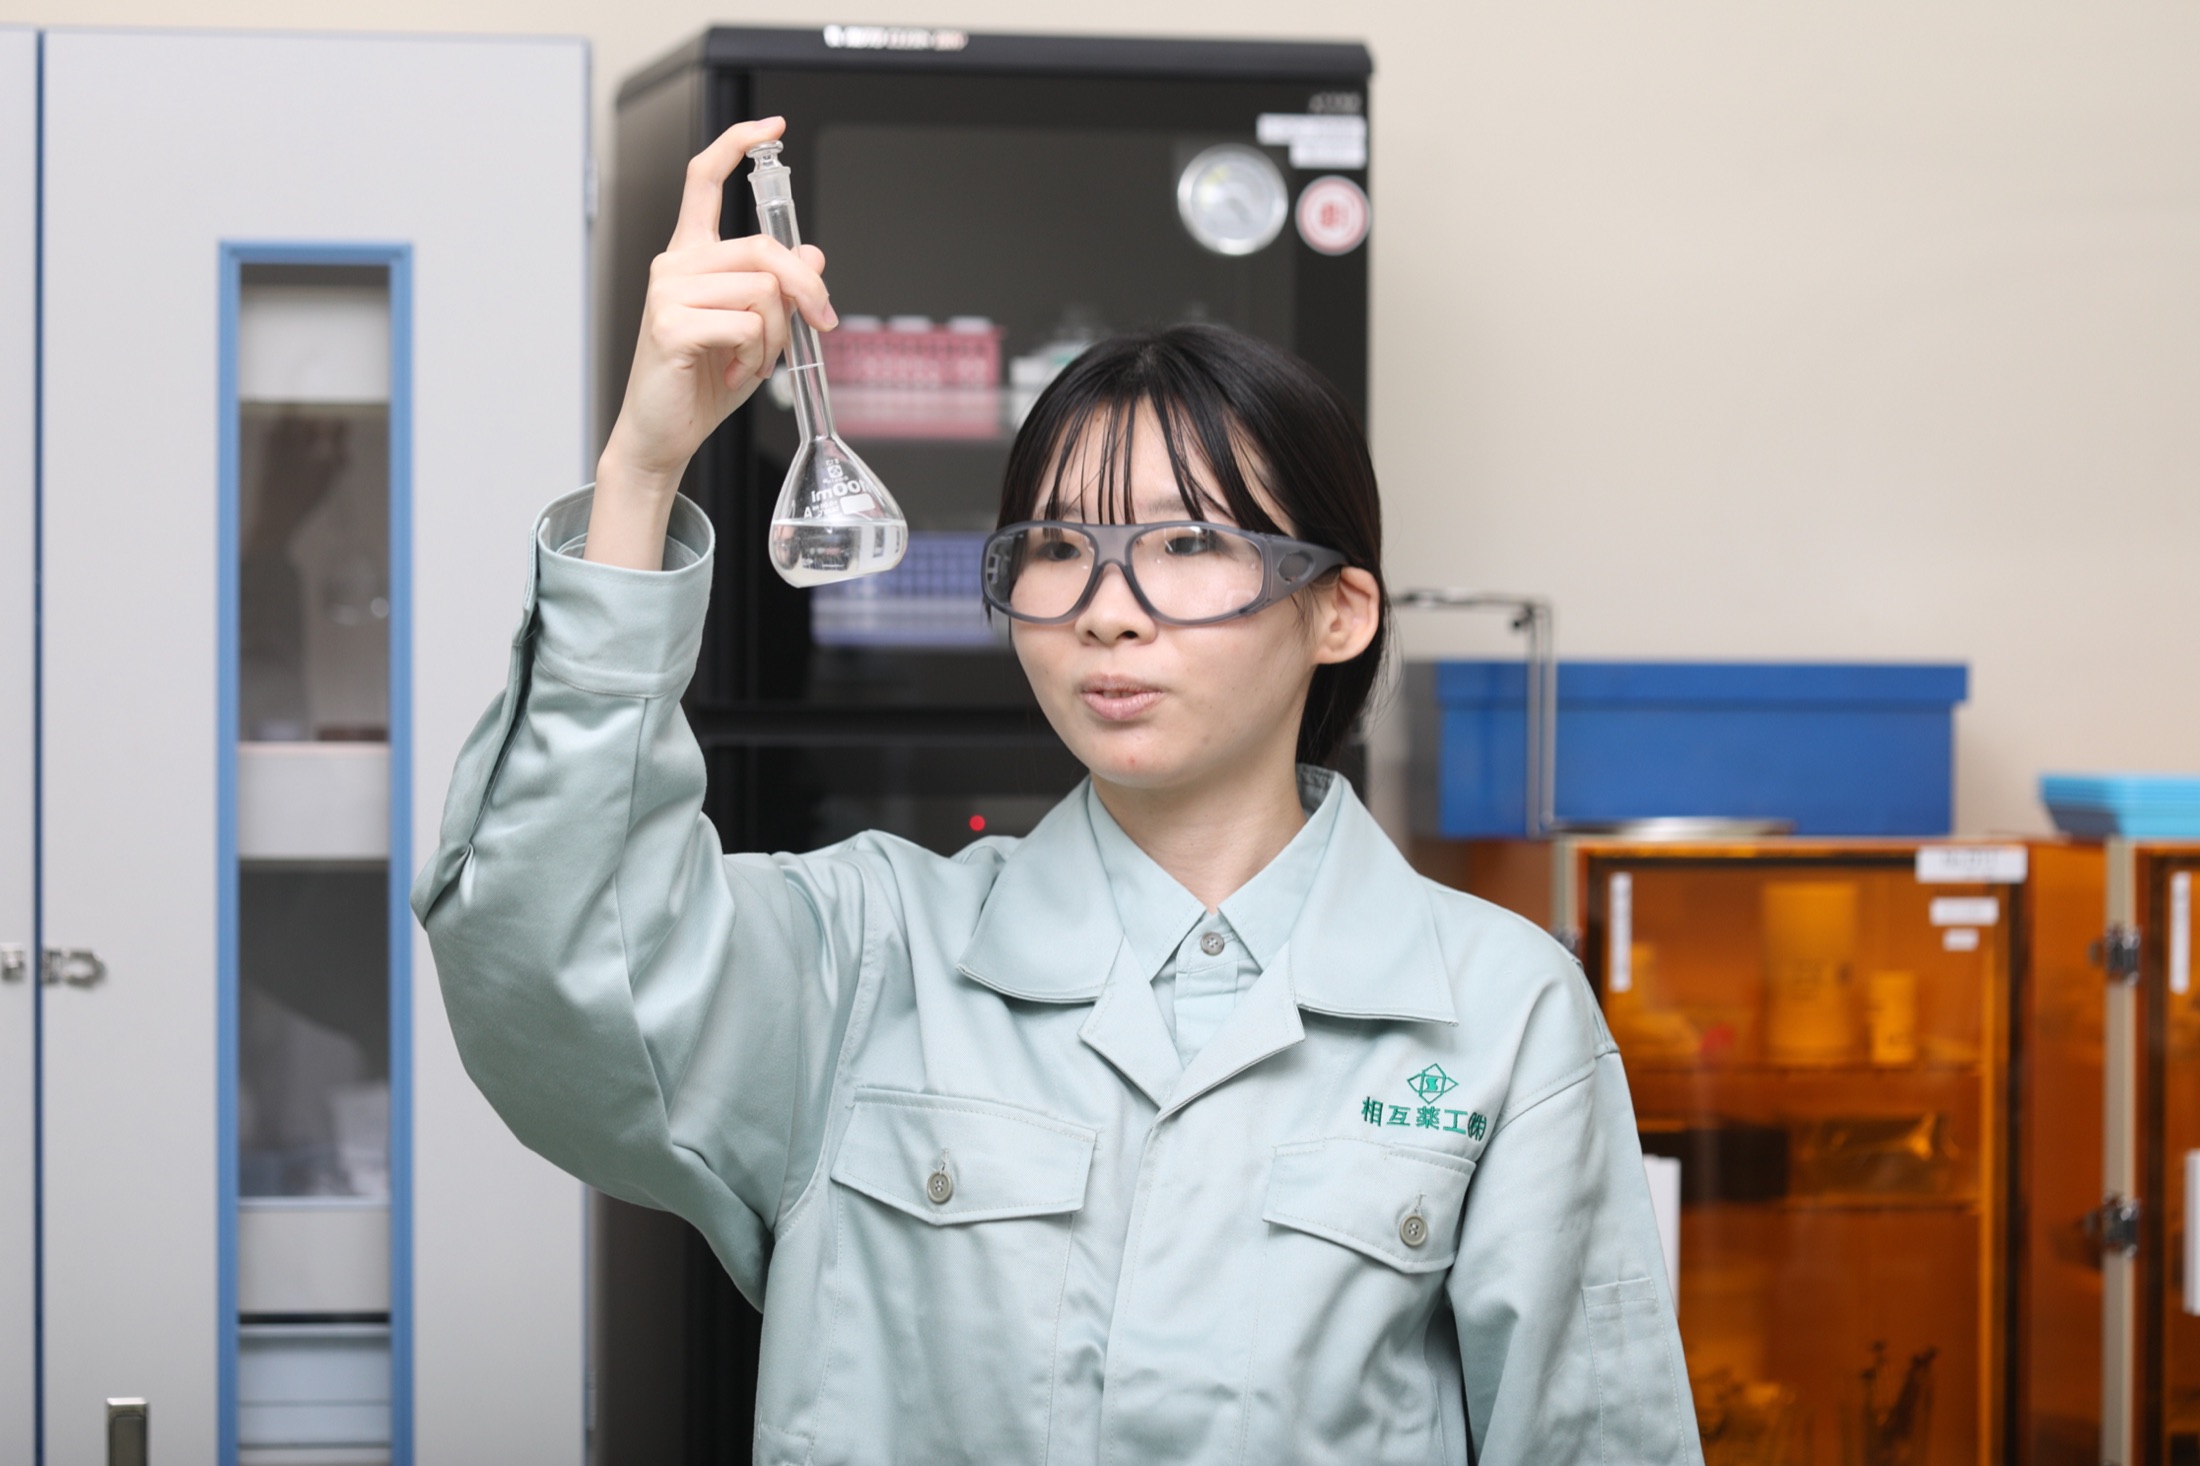
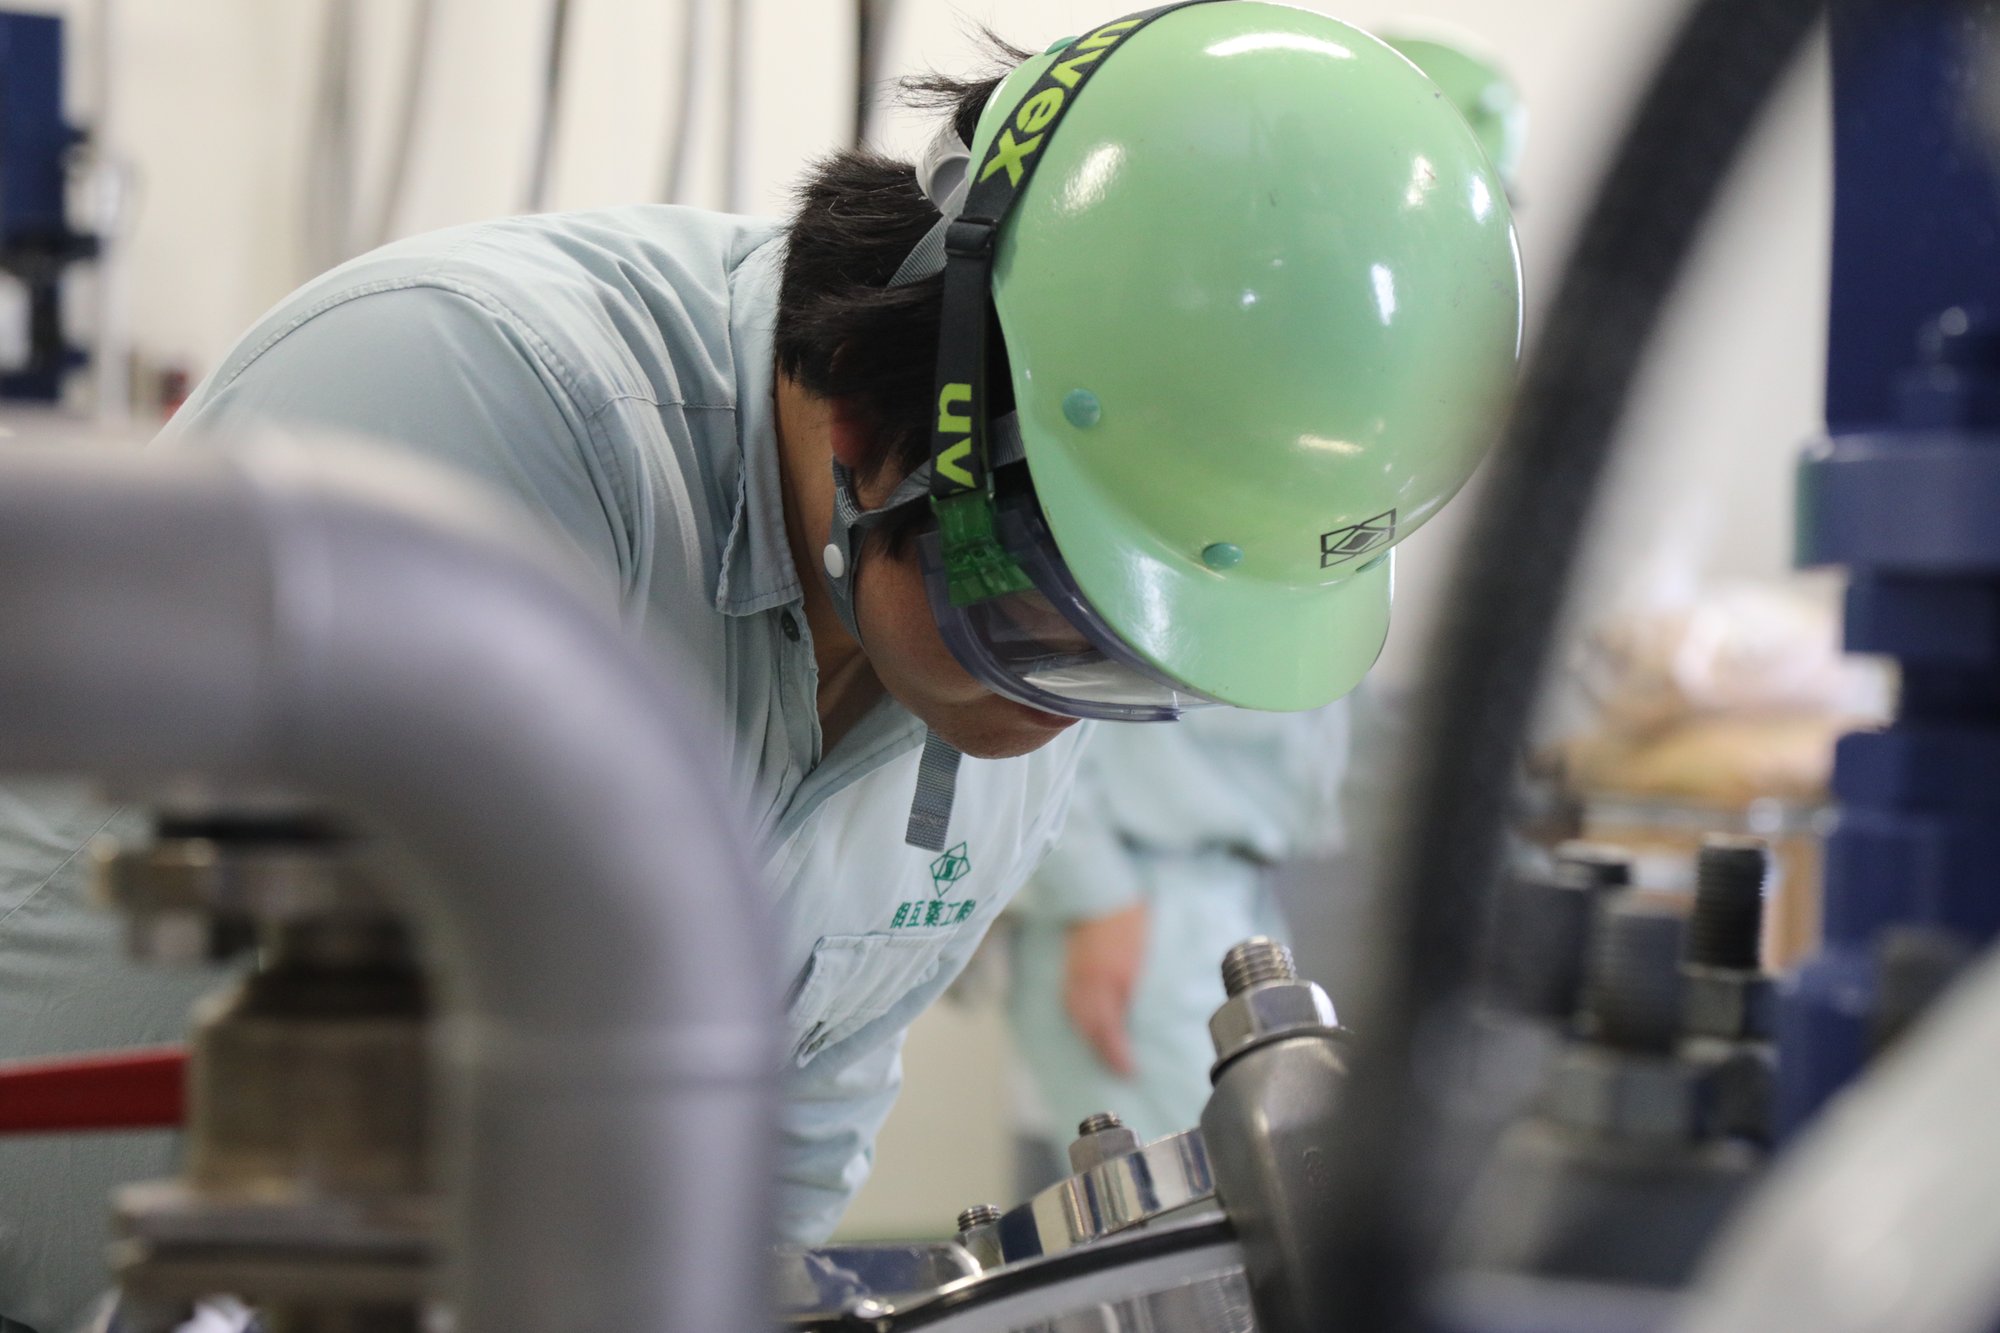
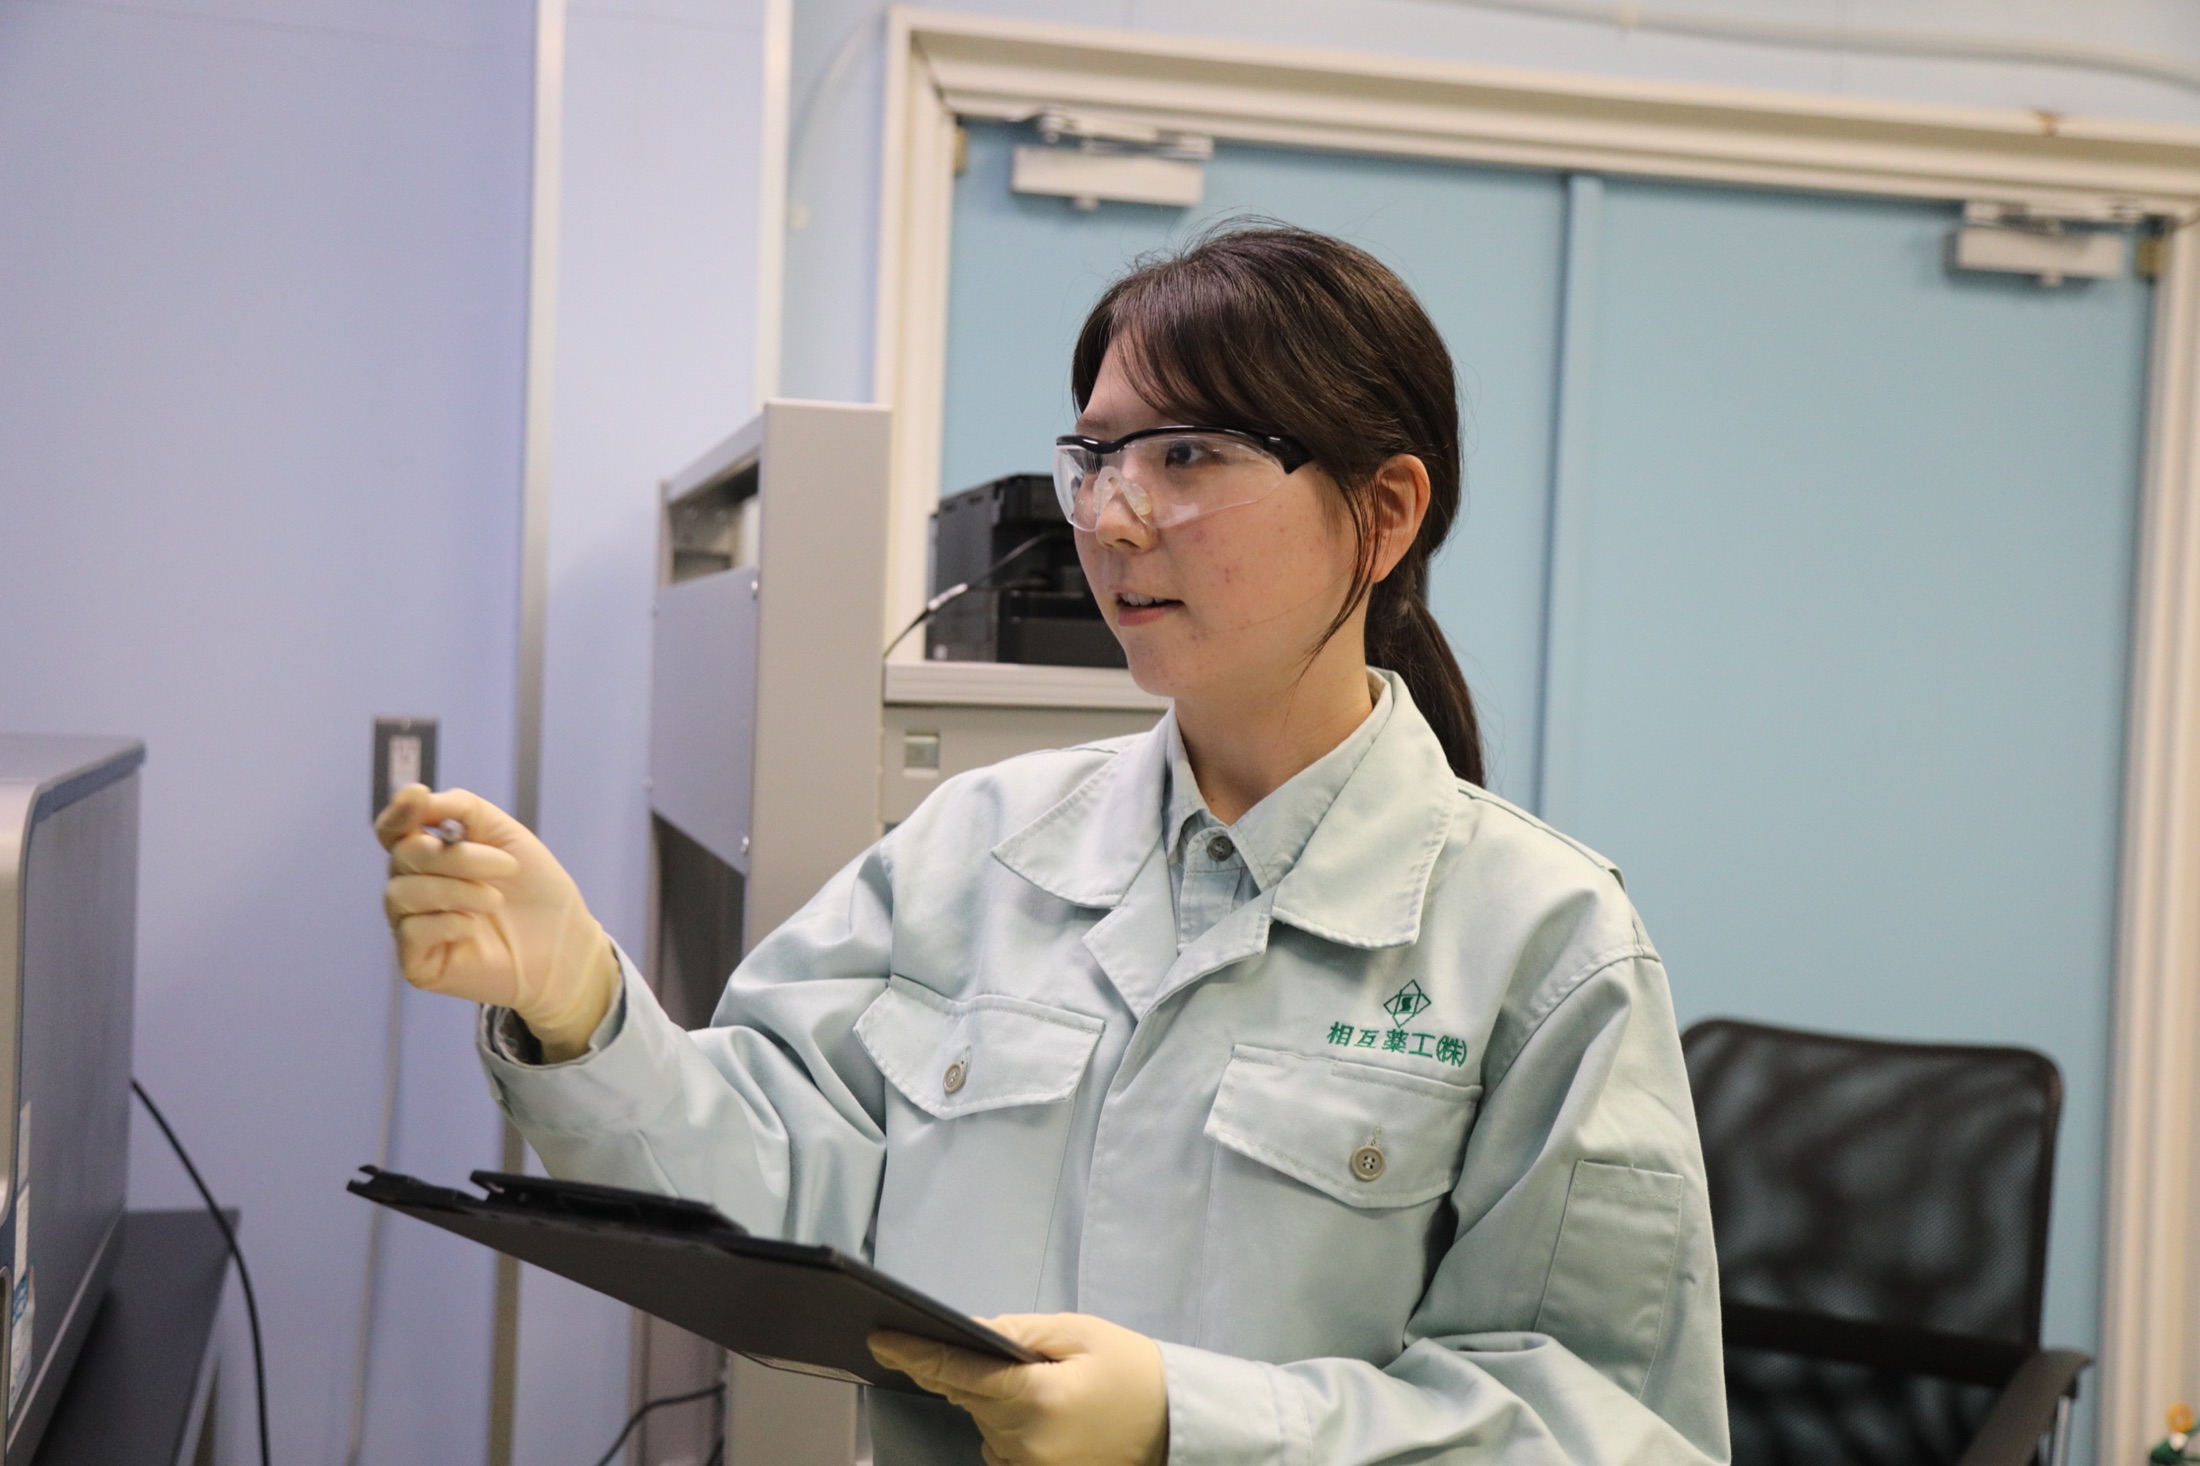
Reliable data as the foundation underpinning the assurance of quality
We regard data integrity (DI) as a critical element of quality assurance. Data generated and recorded in manufacturing, testing, quality assurance, and other operations constitute information that is important for guaranteeing product quality. For this reason, we stress the importance of ensuring the authenticity, legibility, and integrity of data; we have developed the required equipment and procedures; and we have been working to put in place an environment to allow data to be appropriately generated, recorded, and saved. We have also been striving to cultivate a corporate culture to deepen understanding of data integrity and ensure the appropriate handling of data through the provision of education and training to employees. Making a commitment to data integrity a core pillar of our quality-assurance activities facilitates the provision of highly reliable products.
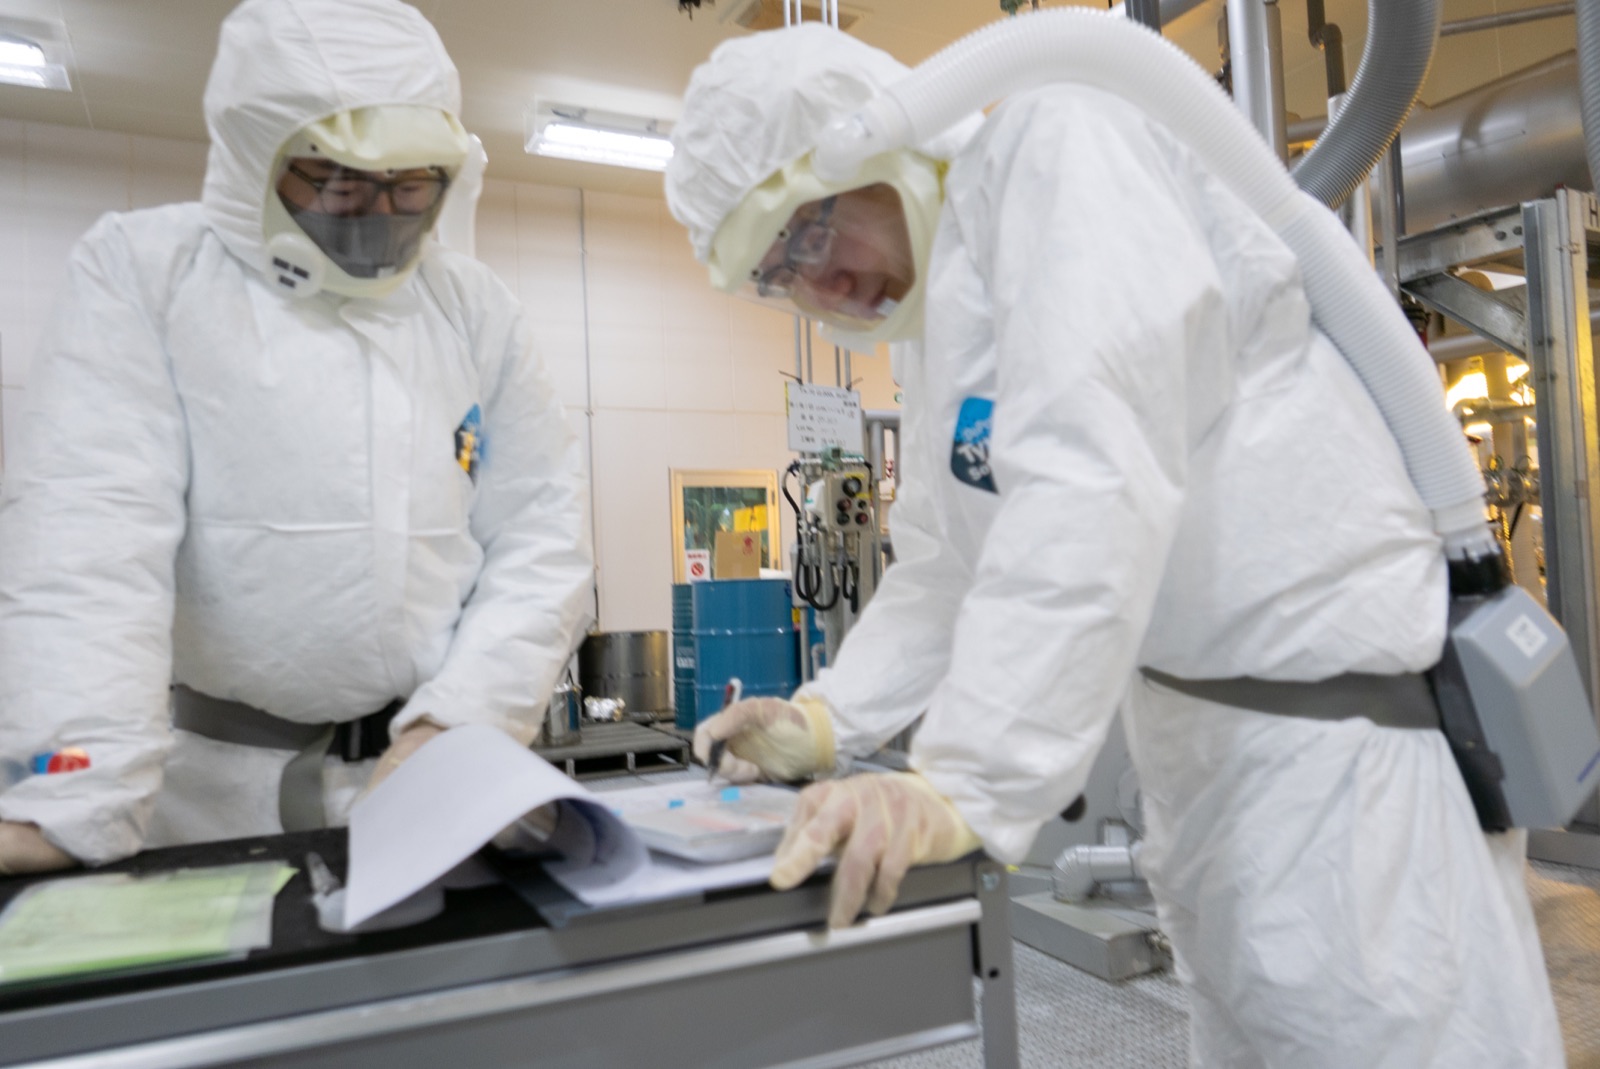
Rather than feel that our job is done once a quality-assurance system is put in place, we believe that it is vital to have such a system be continuously reviewed and improved. We engage in the following quality-assurance activities by using information obtained from our day-to-day manufacturing and quality-control activities.
Through these activities, we appropriately ascertain and manage quality-related risks and endeavor to continuously improve our quality-assurance system.
The products we handle, including active pharmaceutical ingredients, intermediates, and investigational drugs; advanced chemicals; and functional cosmetic ingredients, need to be maintained in a high-quality state and supplied on a consistent basis. When it comes to contract manufacturing in particular, it is important that we accurately understand the client’s requirements and link them to product quality. We regard quality as an important basis of corporate activities and are striving to develop a manufacturing environment in which our clients can confidently place their trust through our cGMP-based quality-assurance system, an appropriate approach to data management, instruction and training, and ongoing improvements. We will continue to pursue quality assurance that lives up to the trust of our clients and aim to become a company selected by clients as a long-term partner.
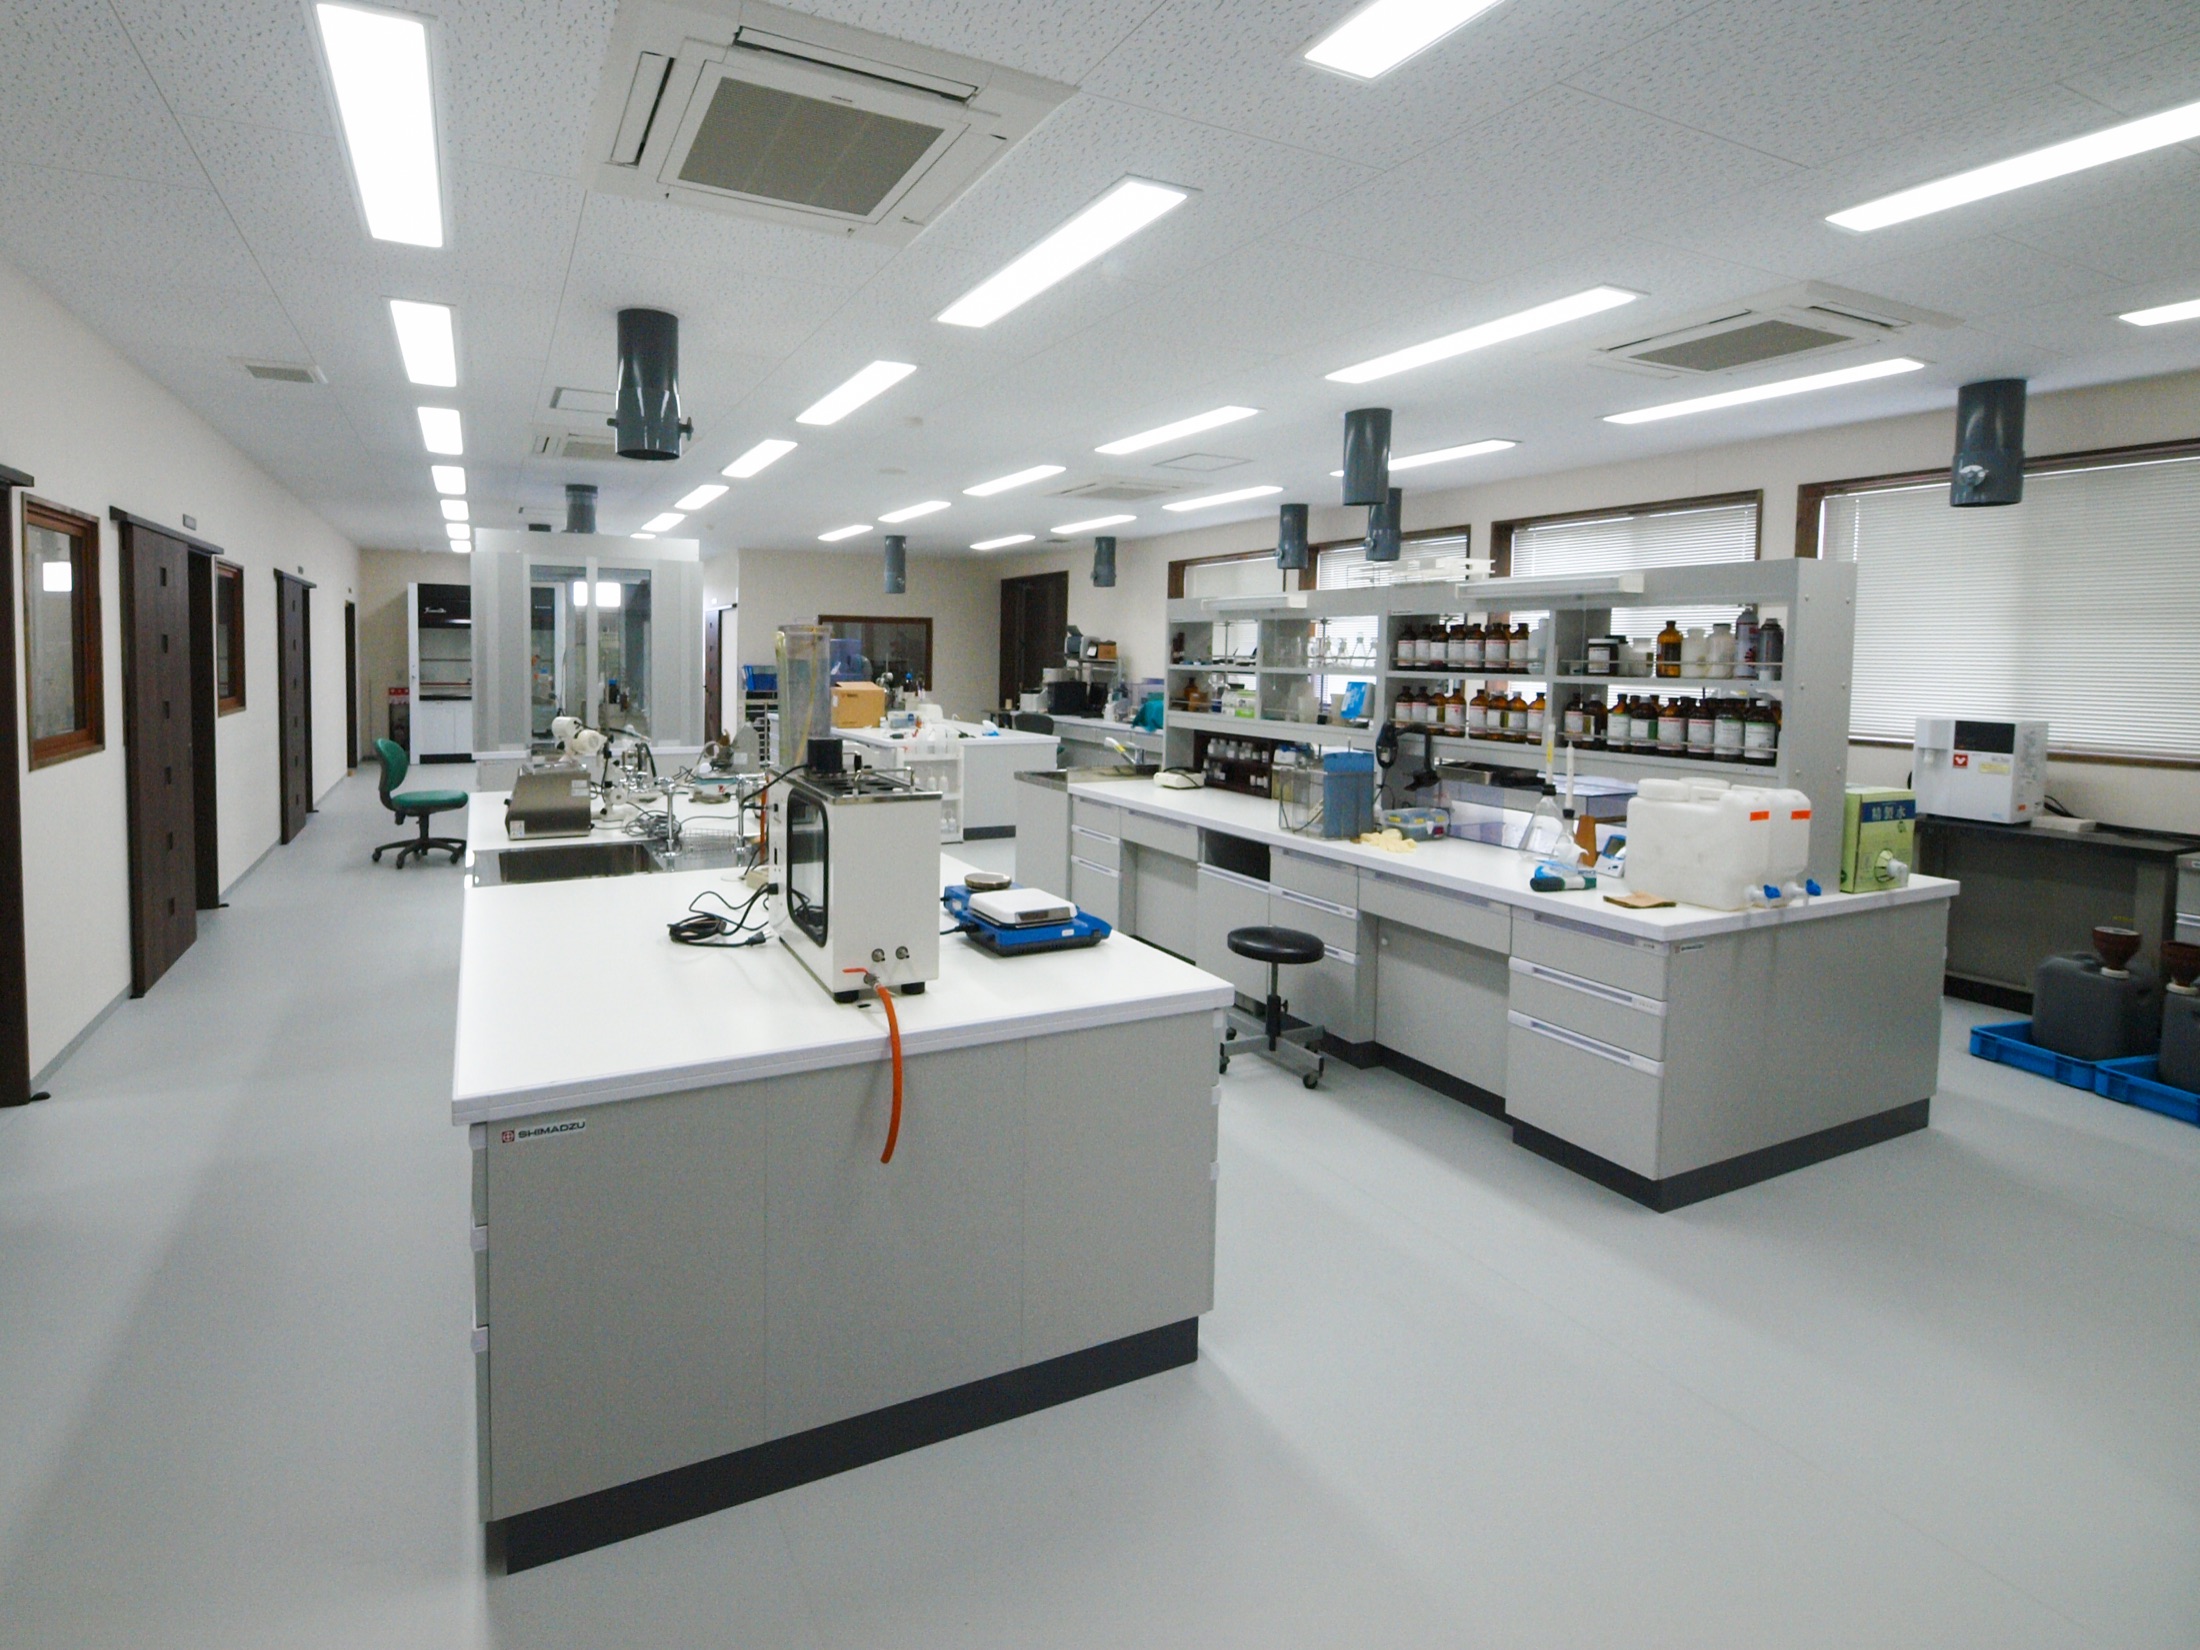
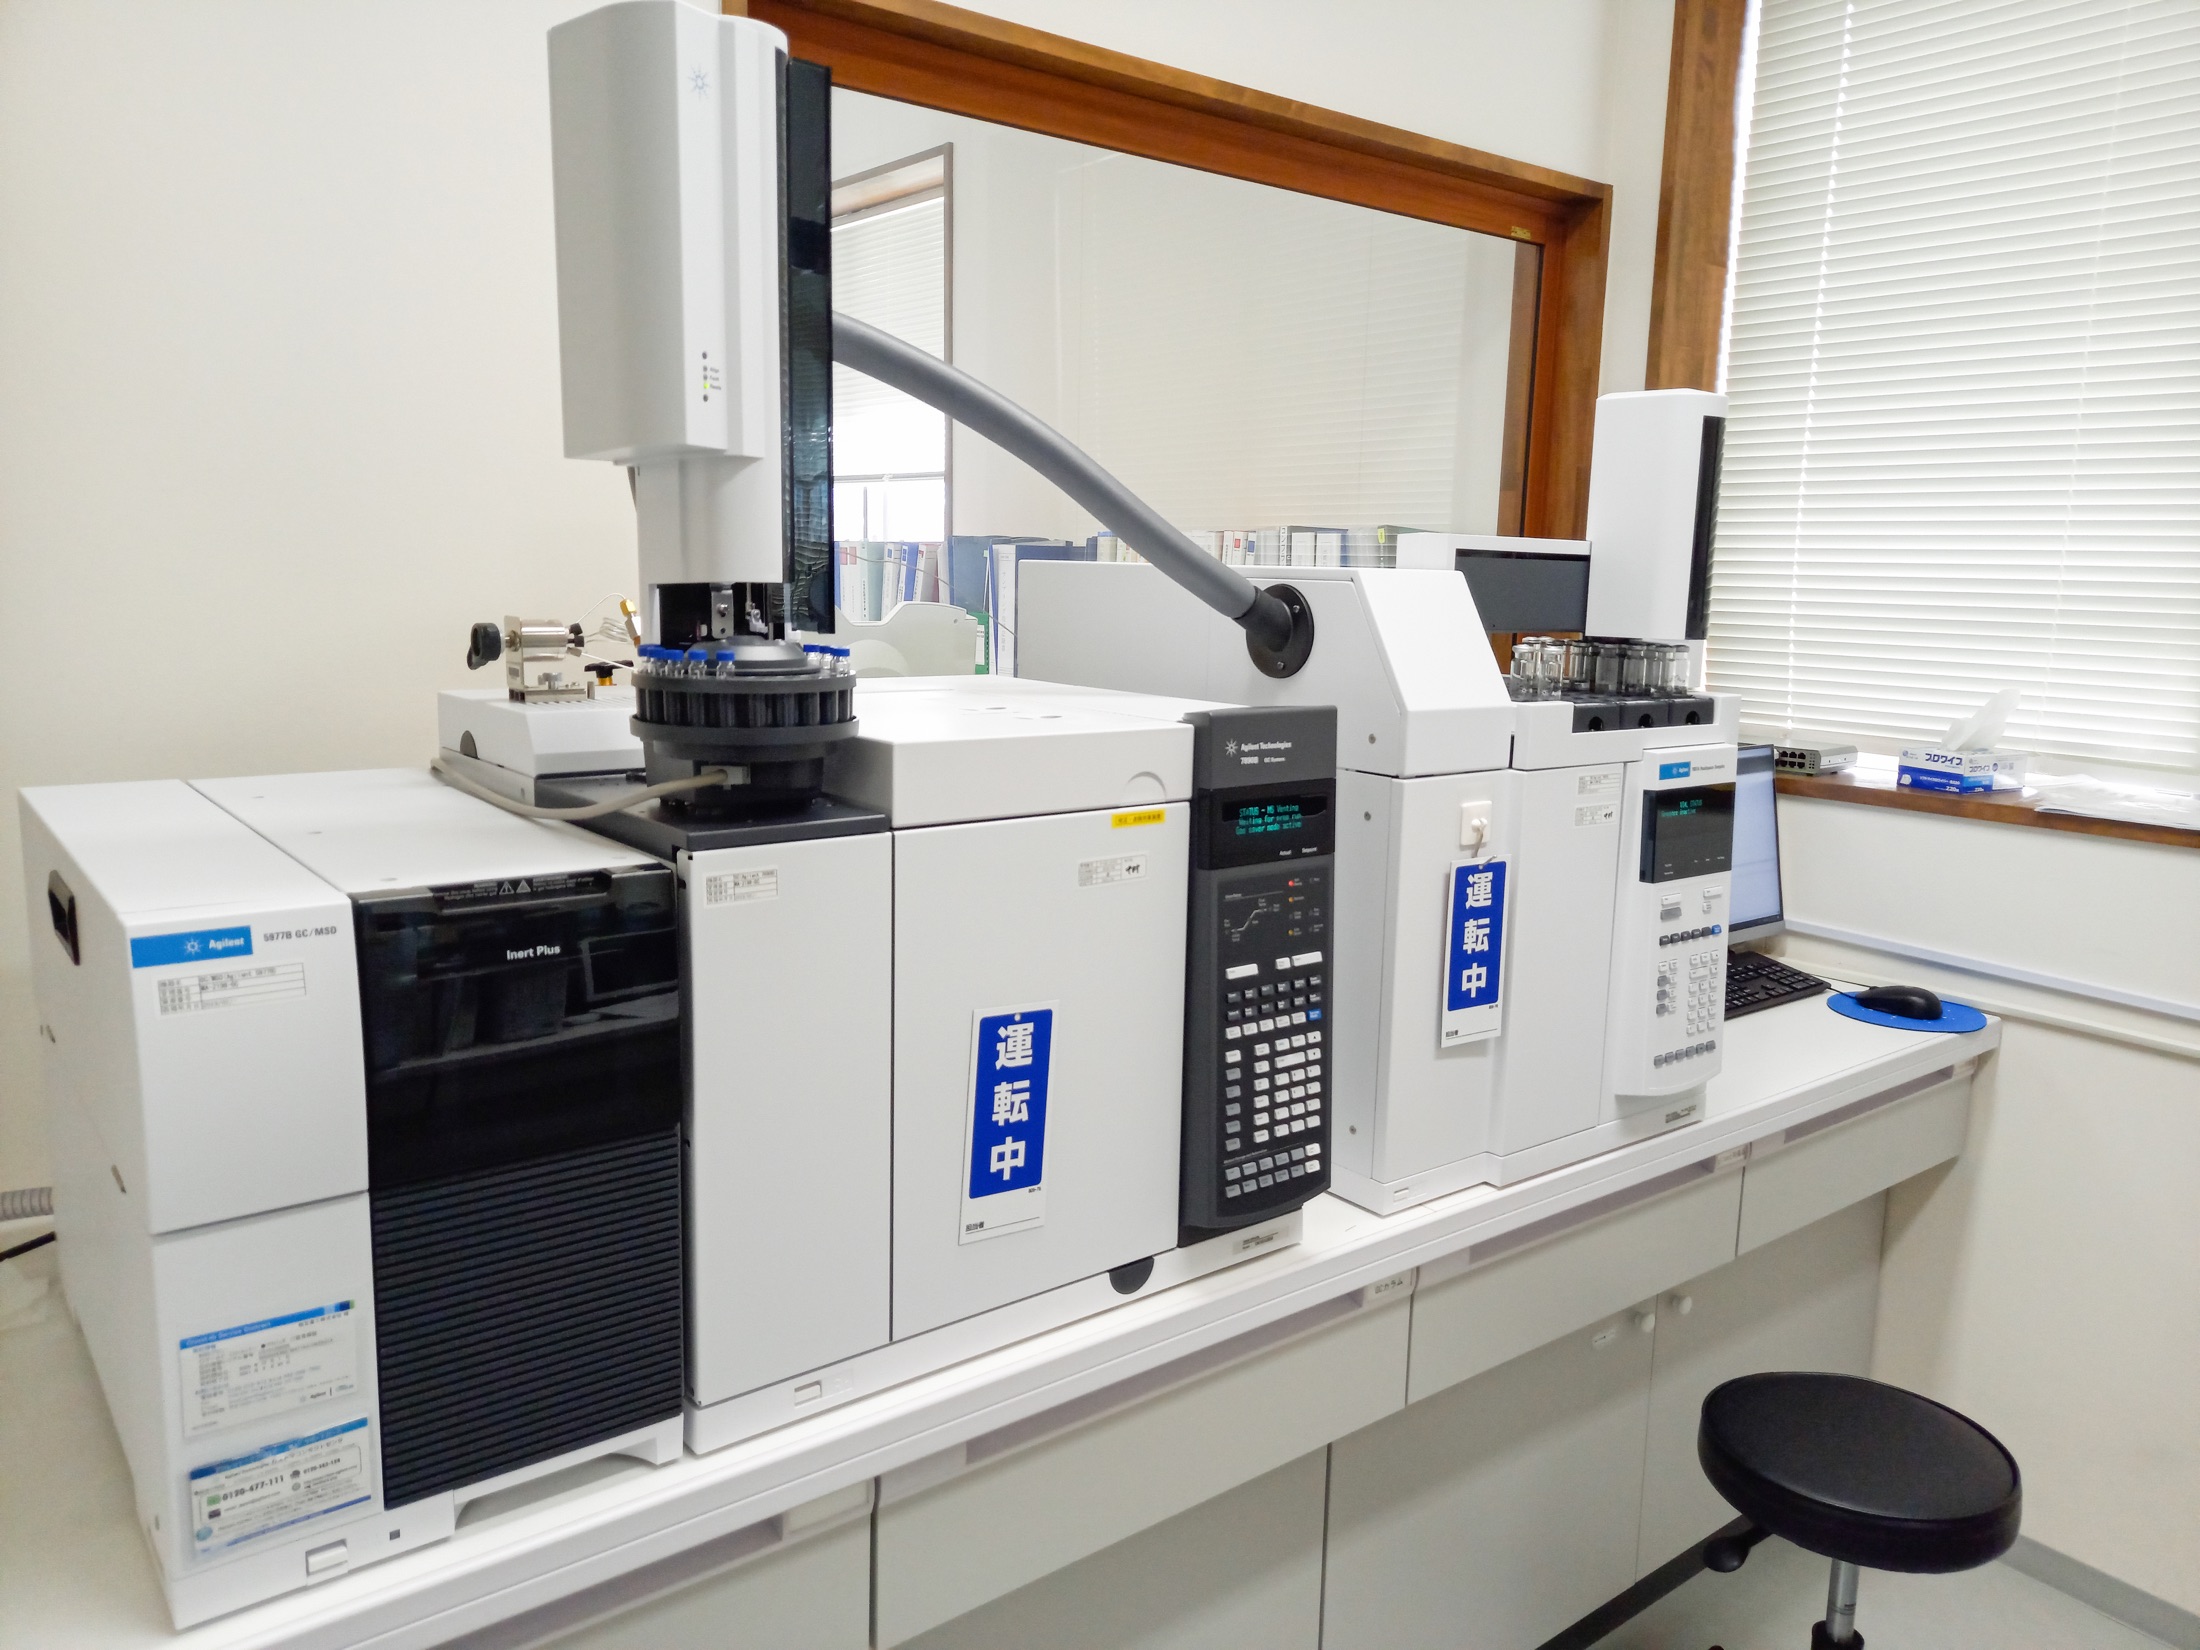
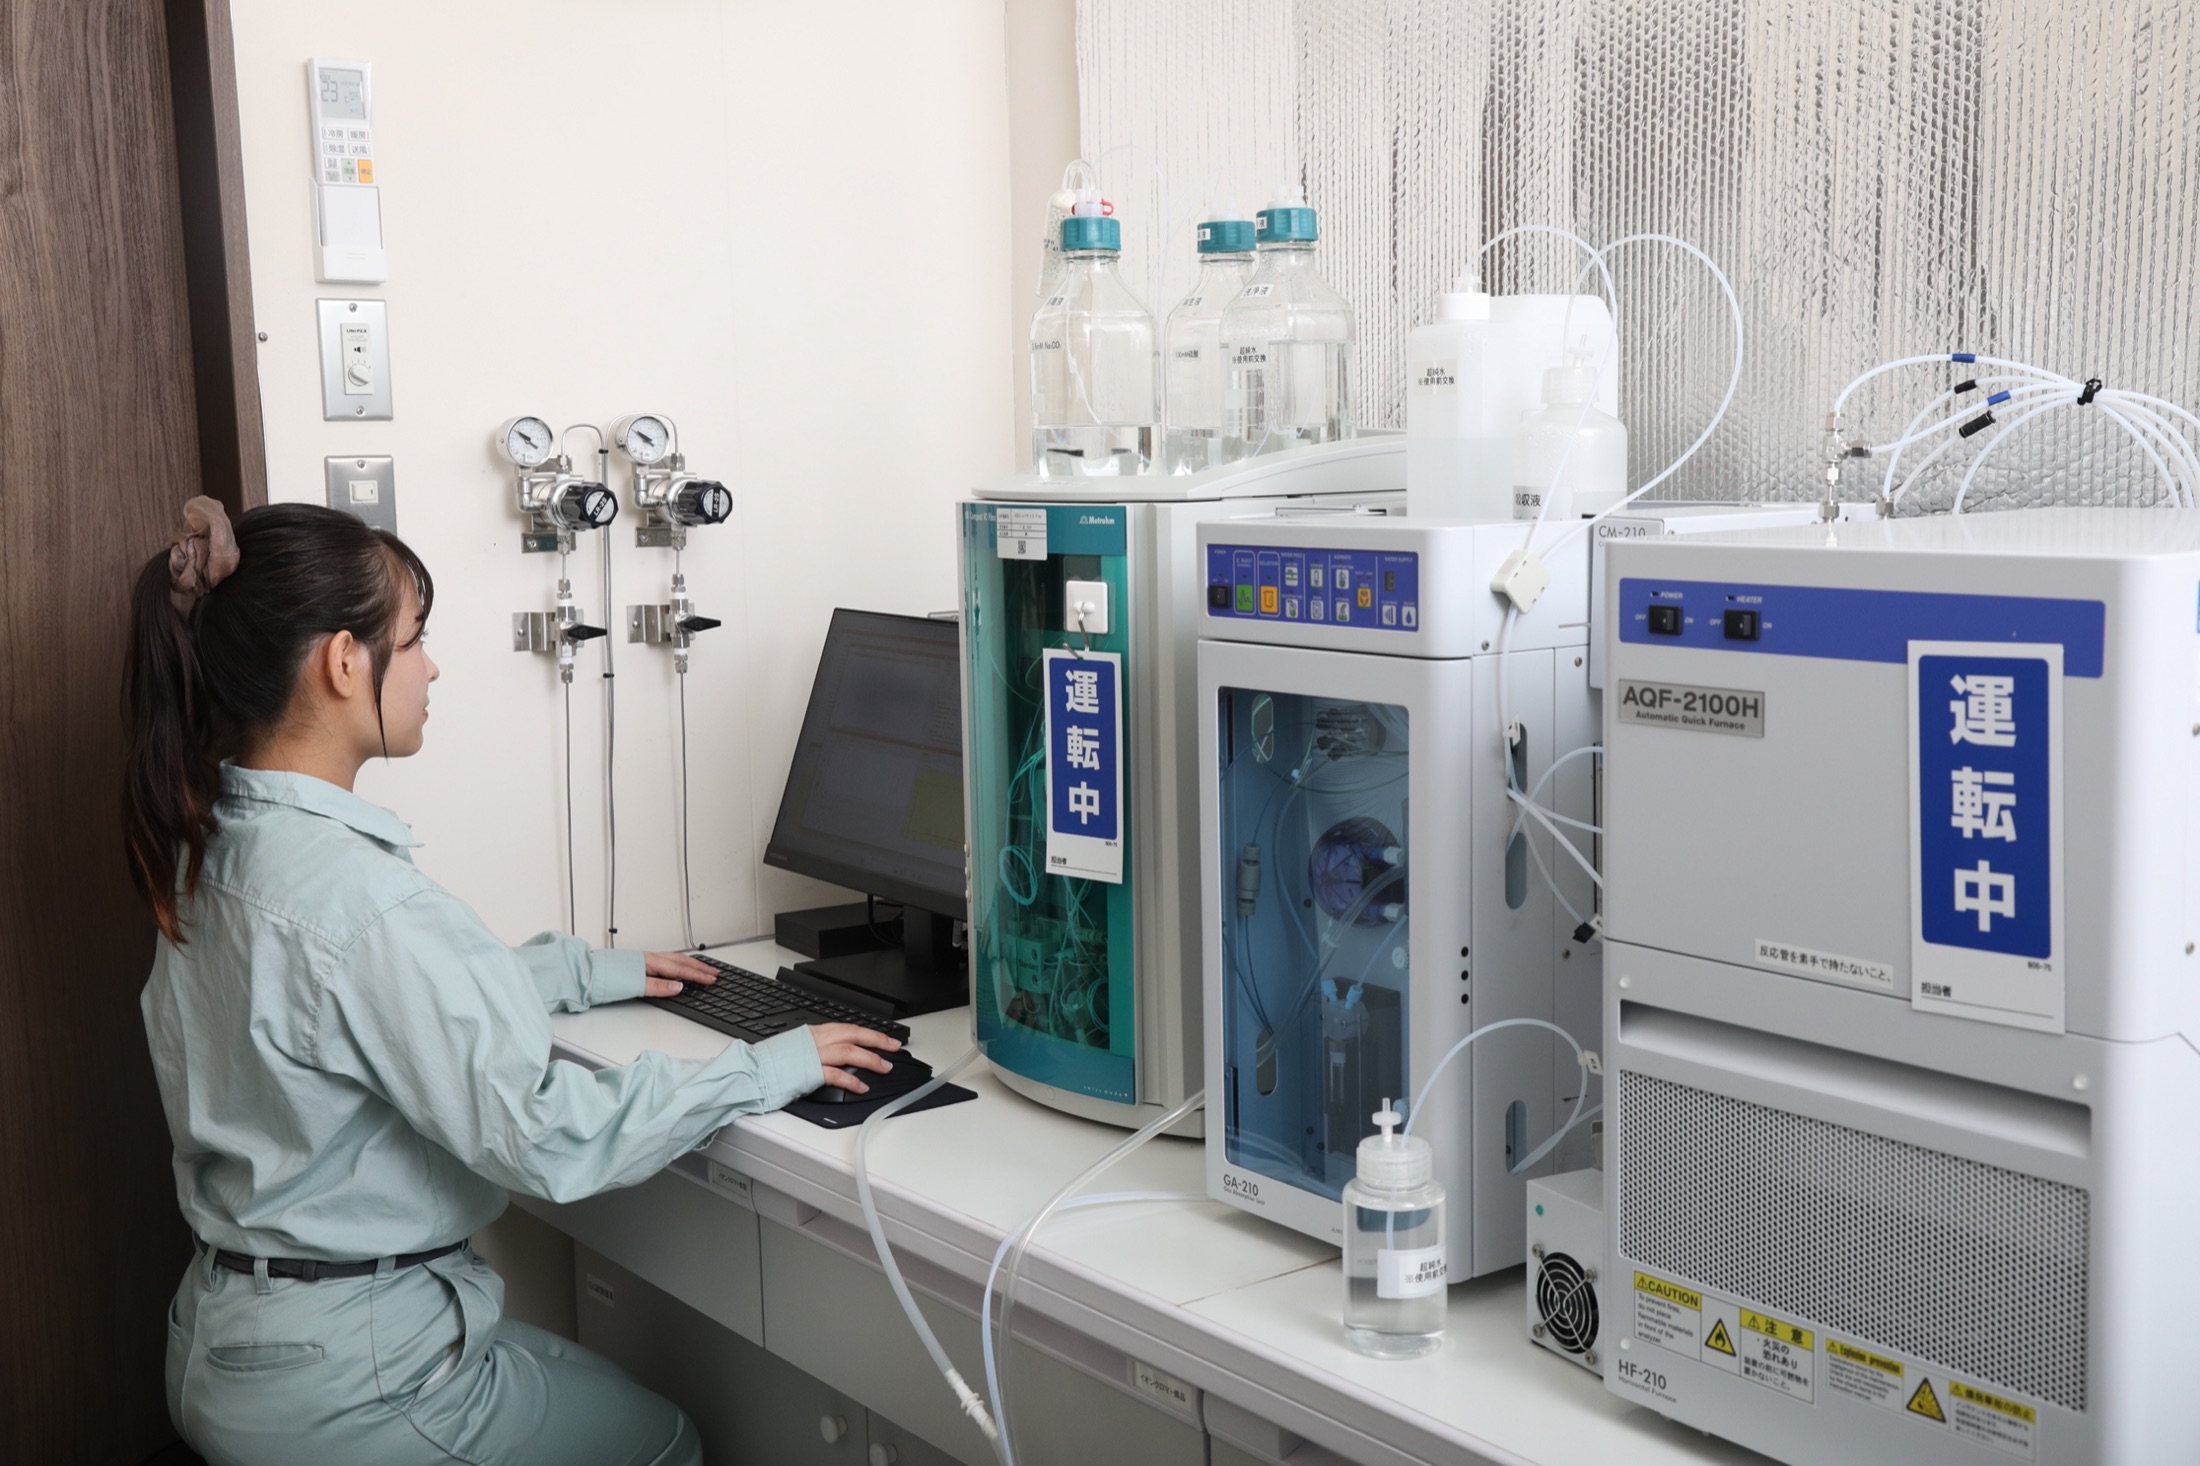
This is a list of the analytical instruments we possess. We maintain a wide variety of such instrument, enabling us to meet our customers' diverse needs. By rigorously evaluating and managing product quality, we ensure a stable supply of high-quality products that our customers can use with complete confidence.
Chromatograph and Mass Spectrometer
| Equipment | Specifications |
|---|---|
| High-Performance Liquid Chromatograph (HPLC) | UV, RI, PDA |
| Liquid Chromatograph Time-of-Flight Mass Spectrometer (LC-TOF/MS) | – |
| Ultra-Performance Liquid Chromatograph Tandem Mass Spectrometer (UPLC-MS/MS) | – |
| Gas Chromatograph (GC) | TCD, FID |
| Headspace Gas Chromatograph (HS-GC) | – |
| Gas Chromatograph Mass Spectrometer (GC-MS) | – |
| Ion Chromatograph (IC) | Combustion method |
Spectroscopy and Structural Analysis
| Equipment | Specifications |
|---|---|
| Nuclear Magnetic Resonance Spectrometer (NMR) | 400 MHz |
| Fourier Transform Infrared Spectrometer (FT-IR) | – |
| UV-Visible Spectrophotometer (UV-Vis) | – |
| Polarimeter | – |
| Microplate Reader | Absorbance, Luminescence, and Fluorescence |
Thermal Analysis and Physical Property Measurement
| Equipment | Specifications |
|---|---|
| Differential Scanning Calorimeter (DSC) | – |
| Thermogravimetric Analyzer (TGA) | – |
| Simultaneous Thermogravimetric and Differential Scanning Calorimeter (TG-DSC) | – |
| Reaction Calorimeter | For Automatic Synthesis System |
| Particle Size Analyzer | Wet and Dry method |
| Melting Point Apparatus | – |
| Colorimeter | – |
| Refractometer | – |
| Density and Specific Gravity Meter | – |
Chemical and Component Analysis
| Equipment | Specifications |
|---|---|
| Automatic Titrator | – |
| Karl Fischer Moisture Titrator | – |
| Total Organic Carbon Analyzer (TOC Analyzer) | – |
| pH Meter / Conductivity Meter | – |
| Endotoxin Analyzer | – |
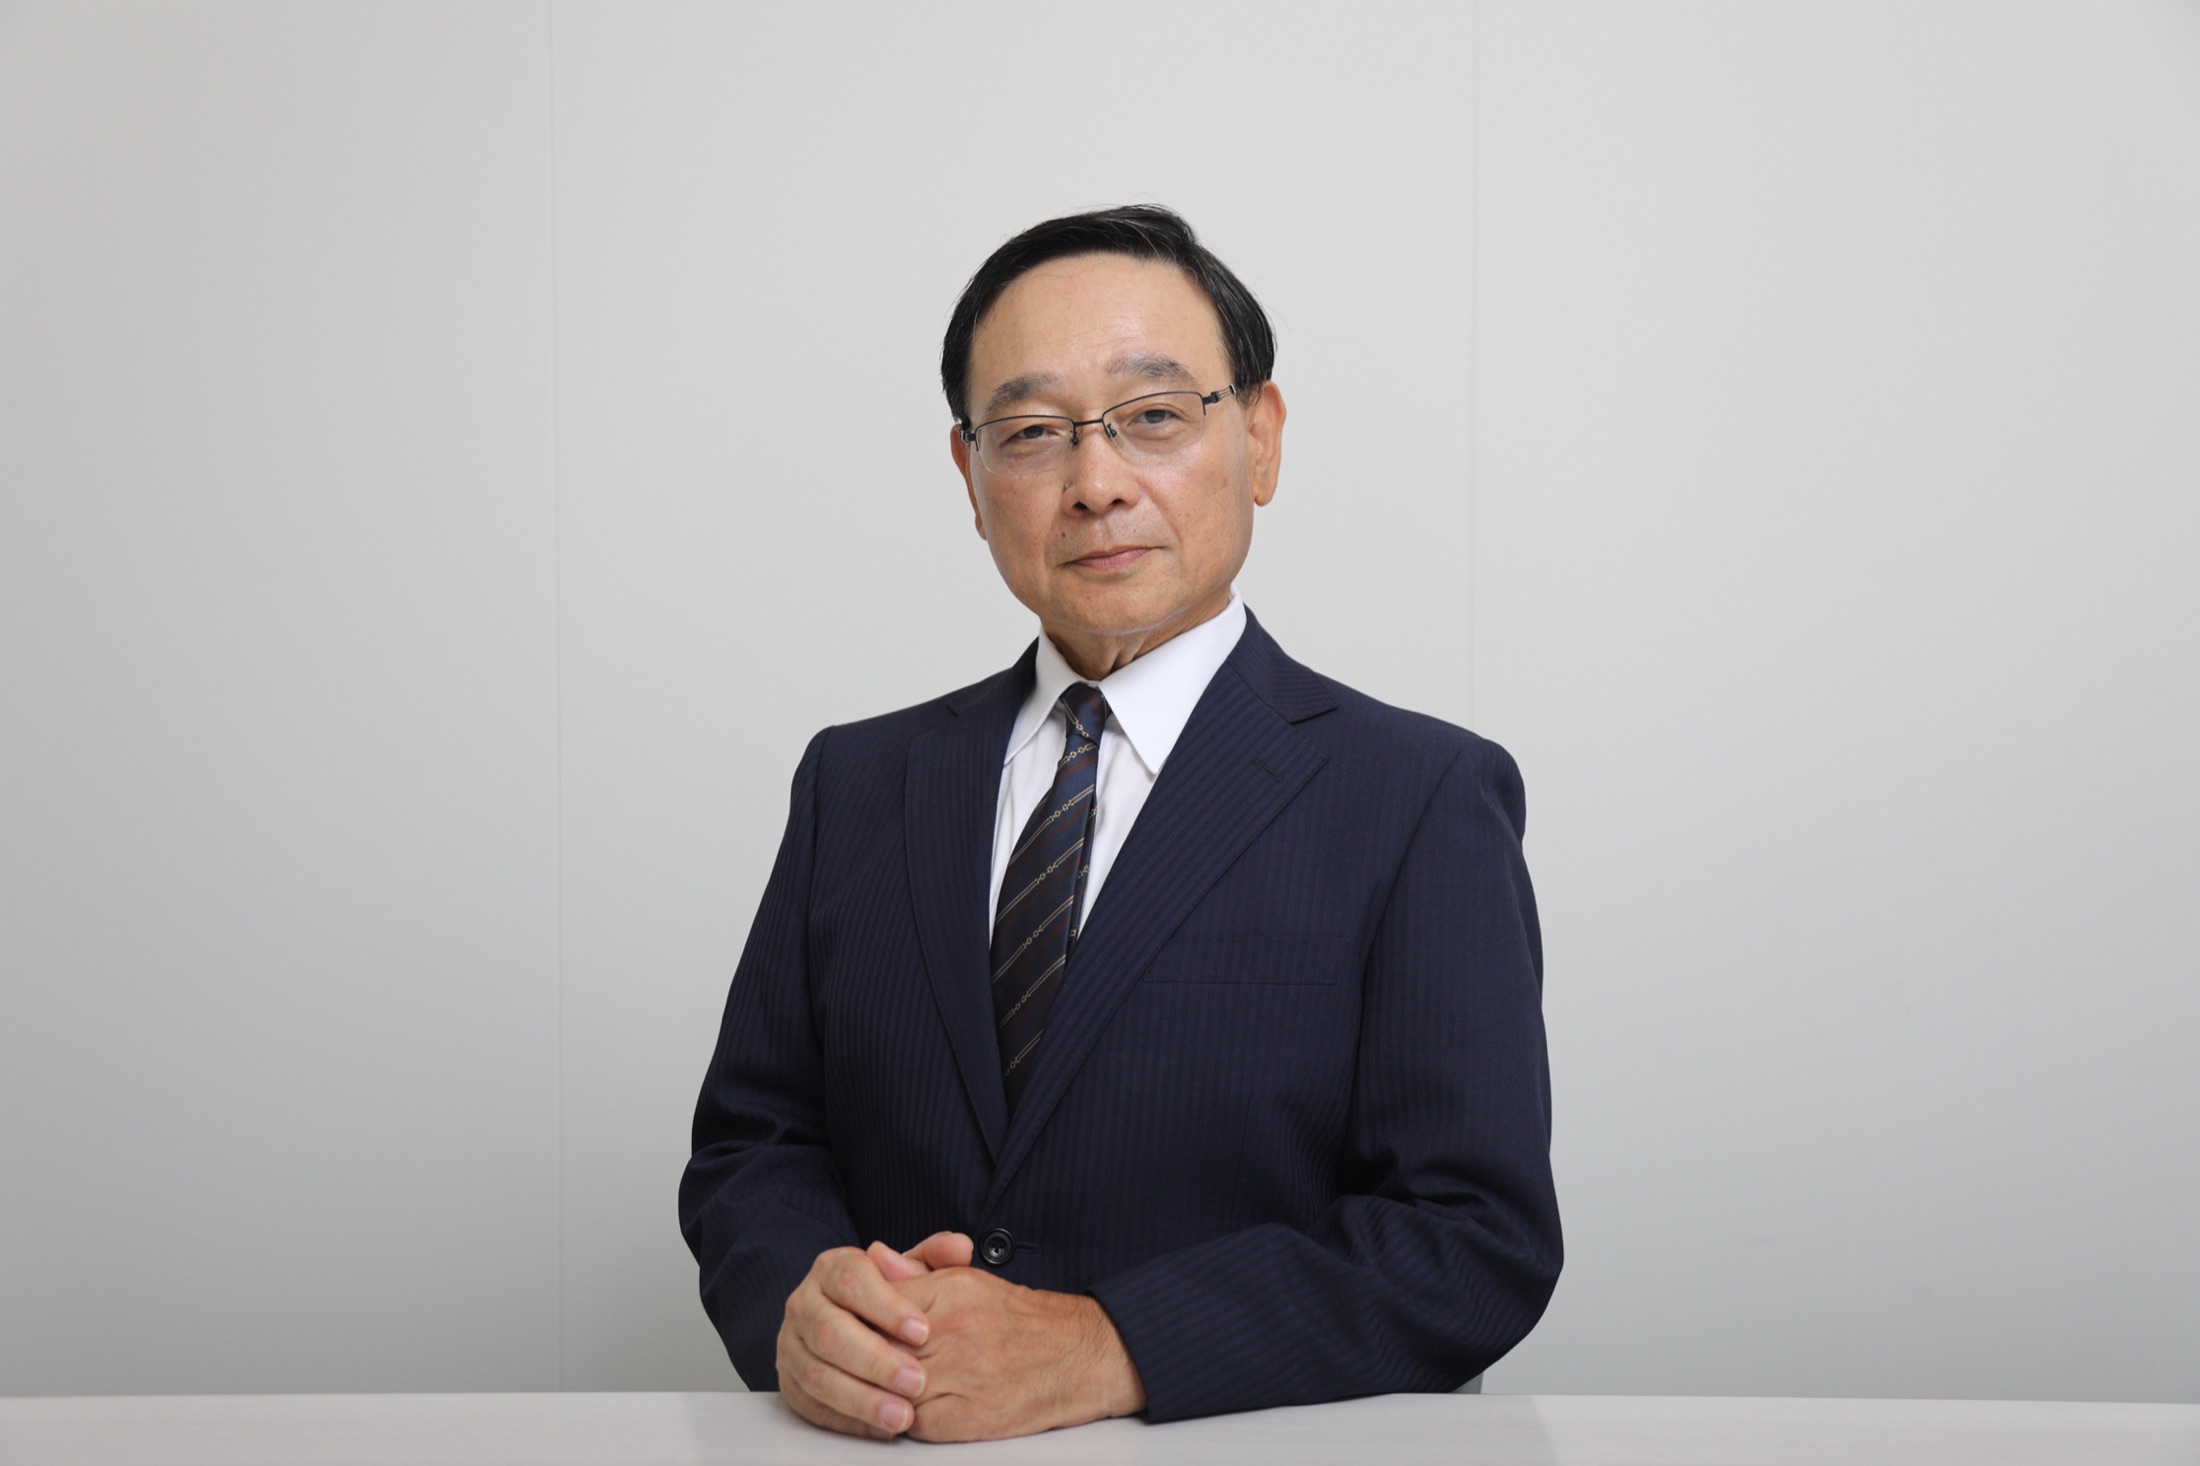
We aim to be the sort of company where each and every one of our employees perceives the importance of his or her place in this organization.In accordance with a recognition that people constitute the greatest asset that we, as a small- to medium-sized enterprise, possess, we will continue to forge a corporate climate in which information is shared irrespective of hierarchical differences and people are free to make statements and act in a free and open manner. In thus embracing the notion that we should reflect on what has been done rather than regret what has not been done, we have made prioritizing courses of action that are taken without fear of the results as our management policy.
We believe that, no matter how much we fail, the accumulation of what we learn from such failures will nourish future results.
Sogo Pharmaceutical Co., Ltd.
Representative Director & President 
| Company name | Sogo Pharmaceutical Co.,Ltd. |
|---|---|
| Representative | President Jun Sawada |
| Founding | 5th April, 1955 |
| Head office location | 〒100-0005 Tekko Bld., 1-8-2 Marunouchi, Chiyoda-Ku, Tokyo |
| Tel | +81-3-6273-4621 |
| FAX | +81-3-5222-0021 |
| Capital | 200 million yen |
| Number of employees | 120 people (as of October 2026) |
| Business Contents | Manufacture, sales, and import/export of active pharmaceutical ingredients, functional cosmetic ingredients, advanced chemicals, and other fine chemical products as well as chemical industrial products |
| Banks | MUFG Bank, Ltd. Yaesudohri branch / Sumitomo Mitsui Banking Corp. Tokyo-Chuo branch |
| Plants | Fukuoka Plant: 〒809-0003 408-1 Sonegasaki, kamisokoino, Nakama-City, Fukuoka Pref. Tel +81-93-246-1971 Fax +81-93-244-0194 Iwaki Plant: 〒972-8312 28-3 Hebinami, Jyoubanshimofunaocyou, Iwaki-City, Fukushima Pref. Tel +81-246-43-5200 Fax +81-246-43-5215 |
| Sogo Trading Co.,Ltd. | Daidou Bld., 3-5-5 Uchikanda, Chiyoda-Ku, Tokyo Tel +81-3-3256-1502 Fax +81-3-3256-1504 https://www.sogo-trd.co.jp/ |
|---|---|
| SPC(Shanghai) Co.,Ltd. | Room 908, No.6333-1 Hu Min Road, TODTOWN TOWER, Minhang District, Shanghai, China Tel +86-21-5417-6229 Fax +86-21-5417-6232 http://en.spc.sh.cn/ |
| Fiscal year end | Net sales (million yen) | Operating profit (million yen) | Ordinary profit (million yen) | Net profit (million yen) |
|---|---|---|---|---|
| Fiscal year ending March 2022 | 3,192 | 167 | 273 | 232 |
| Fiscal year ending March 2023 | 3,141 | 93 | 218 | 171 |
| Fiscal year ending March 2024 | 3,121 | 98 | 173 | 146 |
| Fiscal year ending March 2025 | 3,367 | 158 | 233 | 173 |
| Fiscal year ending March 2026 | 3,348 | 130 | 231 | 212 |
→ Scroll horizontally to see more
| April 1955 | Founded in Kawasaki City, Kanagawa Prefecture. |
|---|---|
| February 1960 | Relocated our plant to Sagamihara City, Kanagawa Prefecture. |
| February 1962 | Opened the Tokyo Office in Chuo-ku, Tokyo. |
| April 1967 | Relocated the Tokyo Office to Otemachi, Chiyoda-ku, Tokyo. |
| May 1969 | Established Sogo Trading Co., Ltd. (formerly Sogo Junyaku Co., Ltd.) as a subsidiary. |
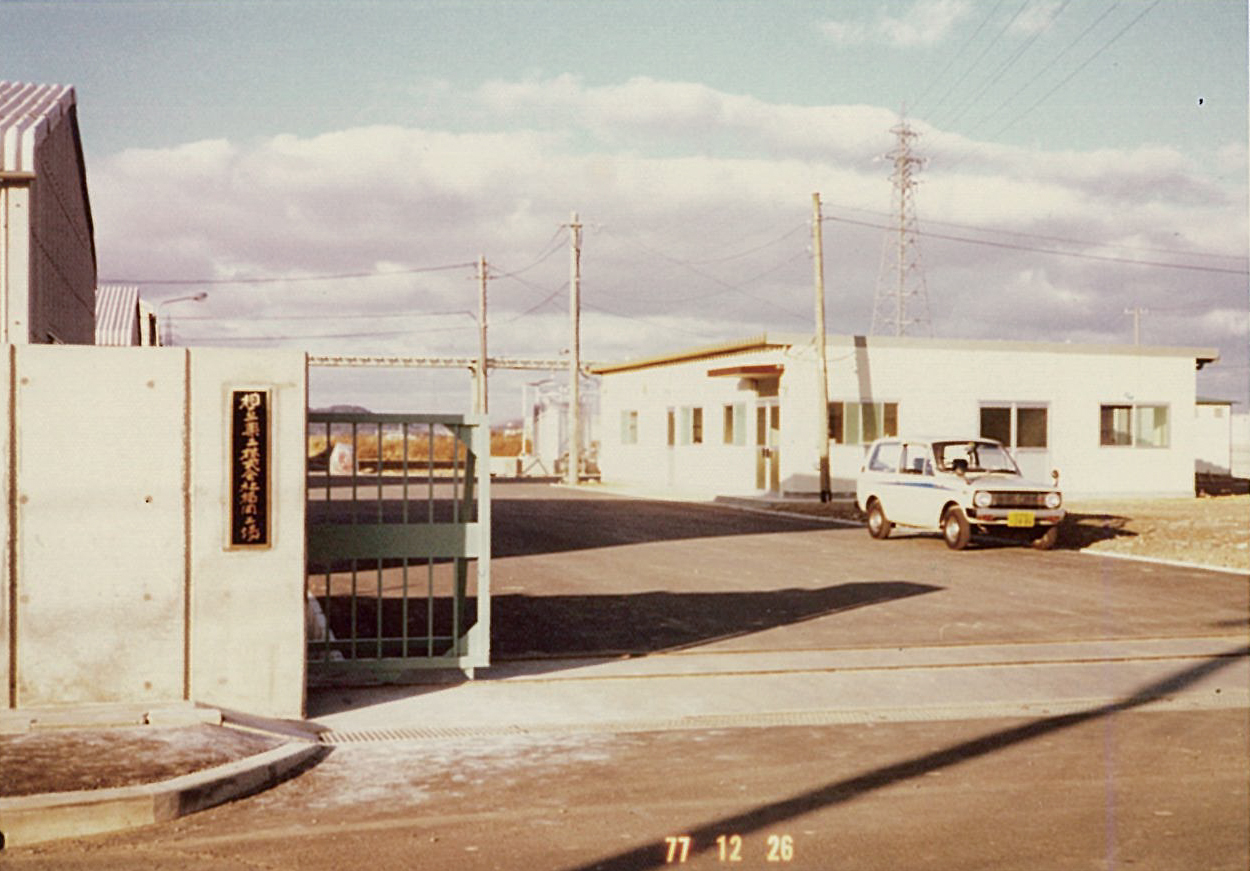
| October 1977 | Completed the Fukuoka Factory in Nakama City, Fukuoka Prefecture. |
| November 1983 | Changed the location of our main office from the Sagamihara Factory to the site of the Tokyo Office and made it our head office. |
| June 1991 | Completed the Iwaki Plant in Iwaki City, Fukushima Prefecture. |
| December 2005 | Established SPC (Shanghai) Co., Ltd. as a subsidiary. |
| June 2011 | Shut down the Sagamihara Factory. |
| November 2015 | Relocated our head office to the Tekko Building in Marunouchi, Chiyoda-ku, Tokyo. |
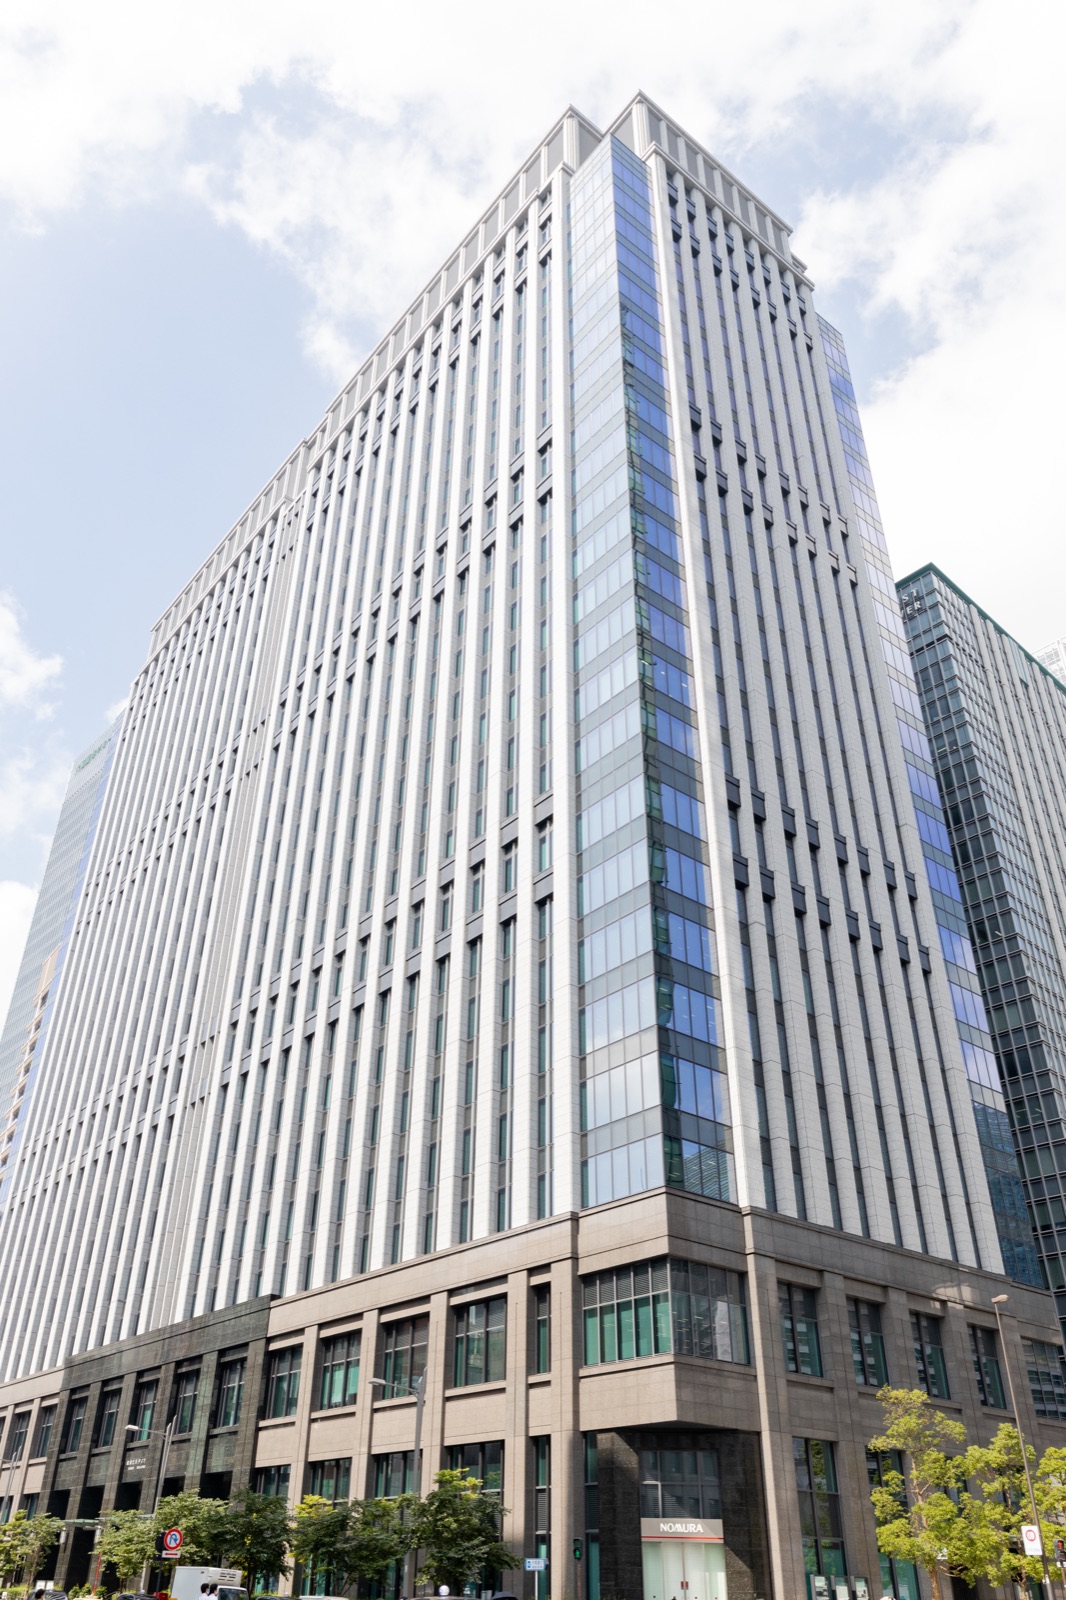
Head Office
〒100-0005 Tekko Bld., 1-8-2 Marunouchi, Chiyoda-Ku, Tokyo Tel +81-3-6273-4621 Fax +81-3-5222-0021
Approx. 2 minutes by walk from the Yaesu North Exit or Nihombashi Exit of Tokyo Station / Directly connected to Otemachi Station (Exit B10) / Approx. 3 minutes by walk from Nihombashi Station (Exit A3) / Approx. 3 minute by walk from Mitsukoshimae Station (Exit B2; via the Hanzomon Line)
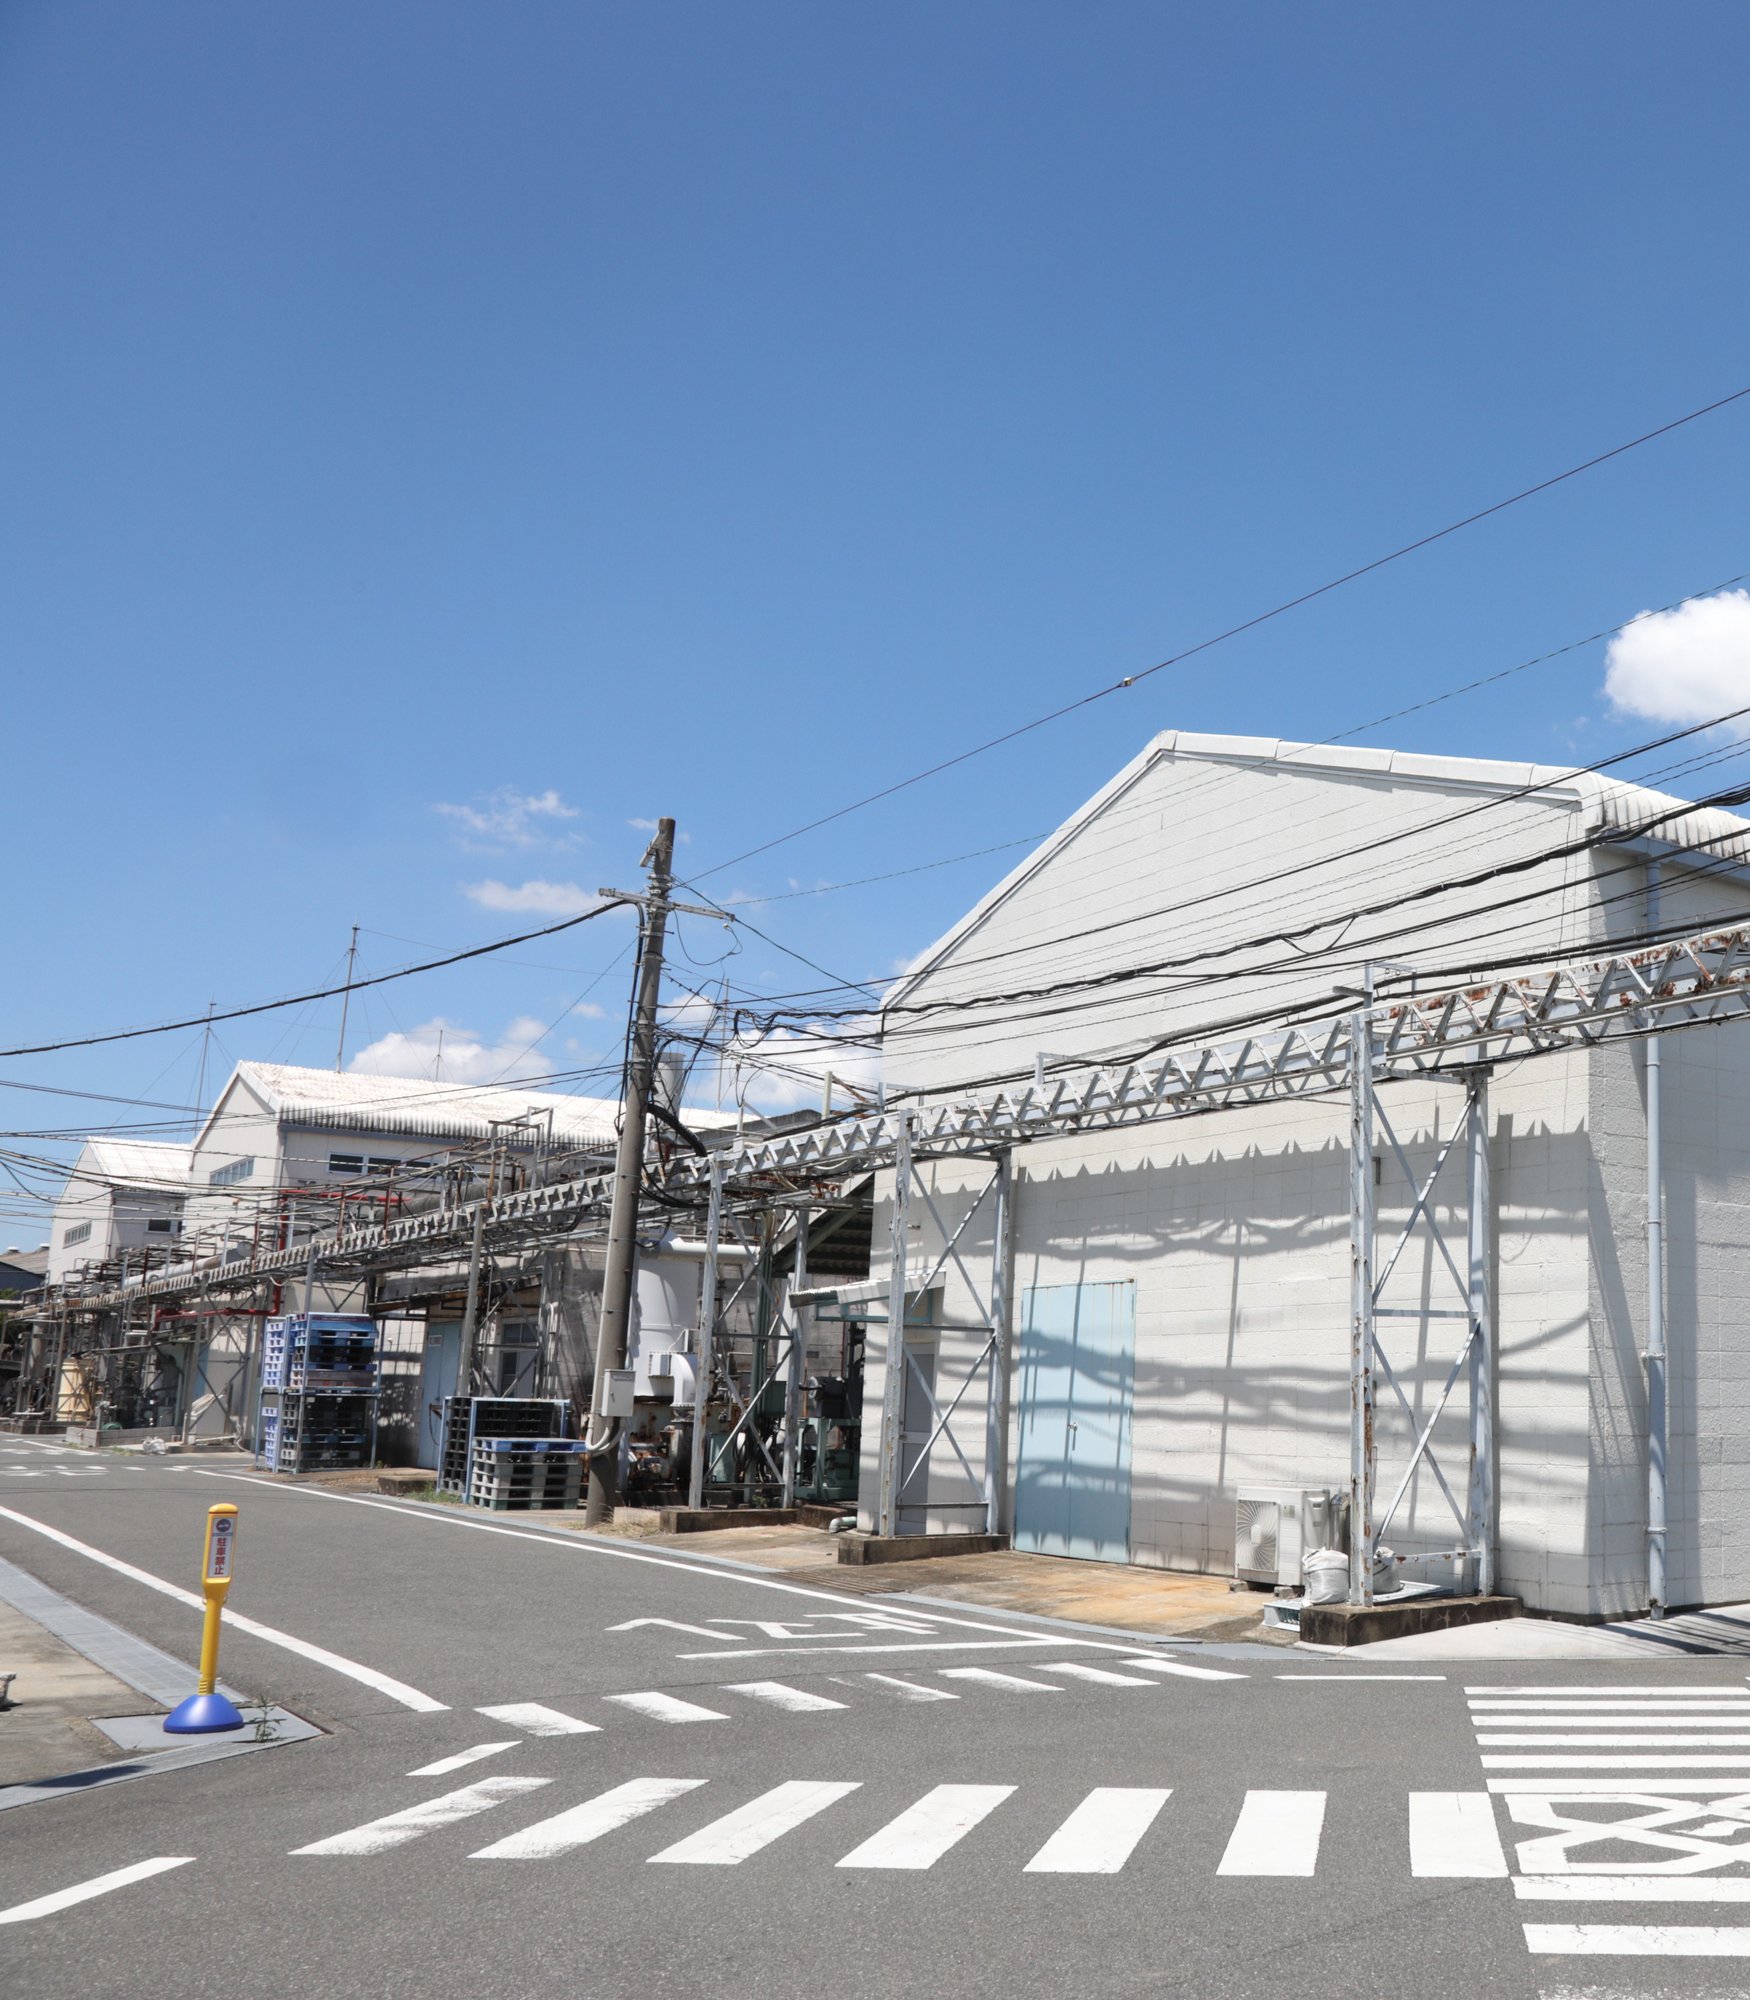
Fukuoka Plant
〒809-0003 408-1 Sonegasaki, kamisokoino, Nakama-City, Fukuoka Pref. Tel +81-93-246-1971 Fax +81-93-244-0194
Approx. 20-minutes by walk from Chikuzen-Habu Station (JR Fukuhoku Yutaka Line) or approx. 10-minutes by taxi from Ongagawa Station (JR Kagoshima Main Line).
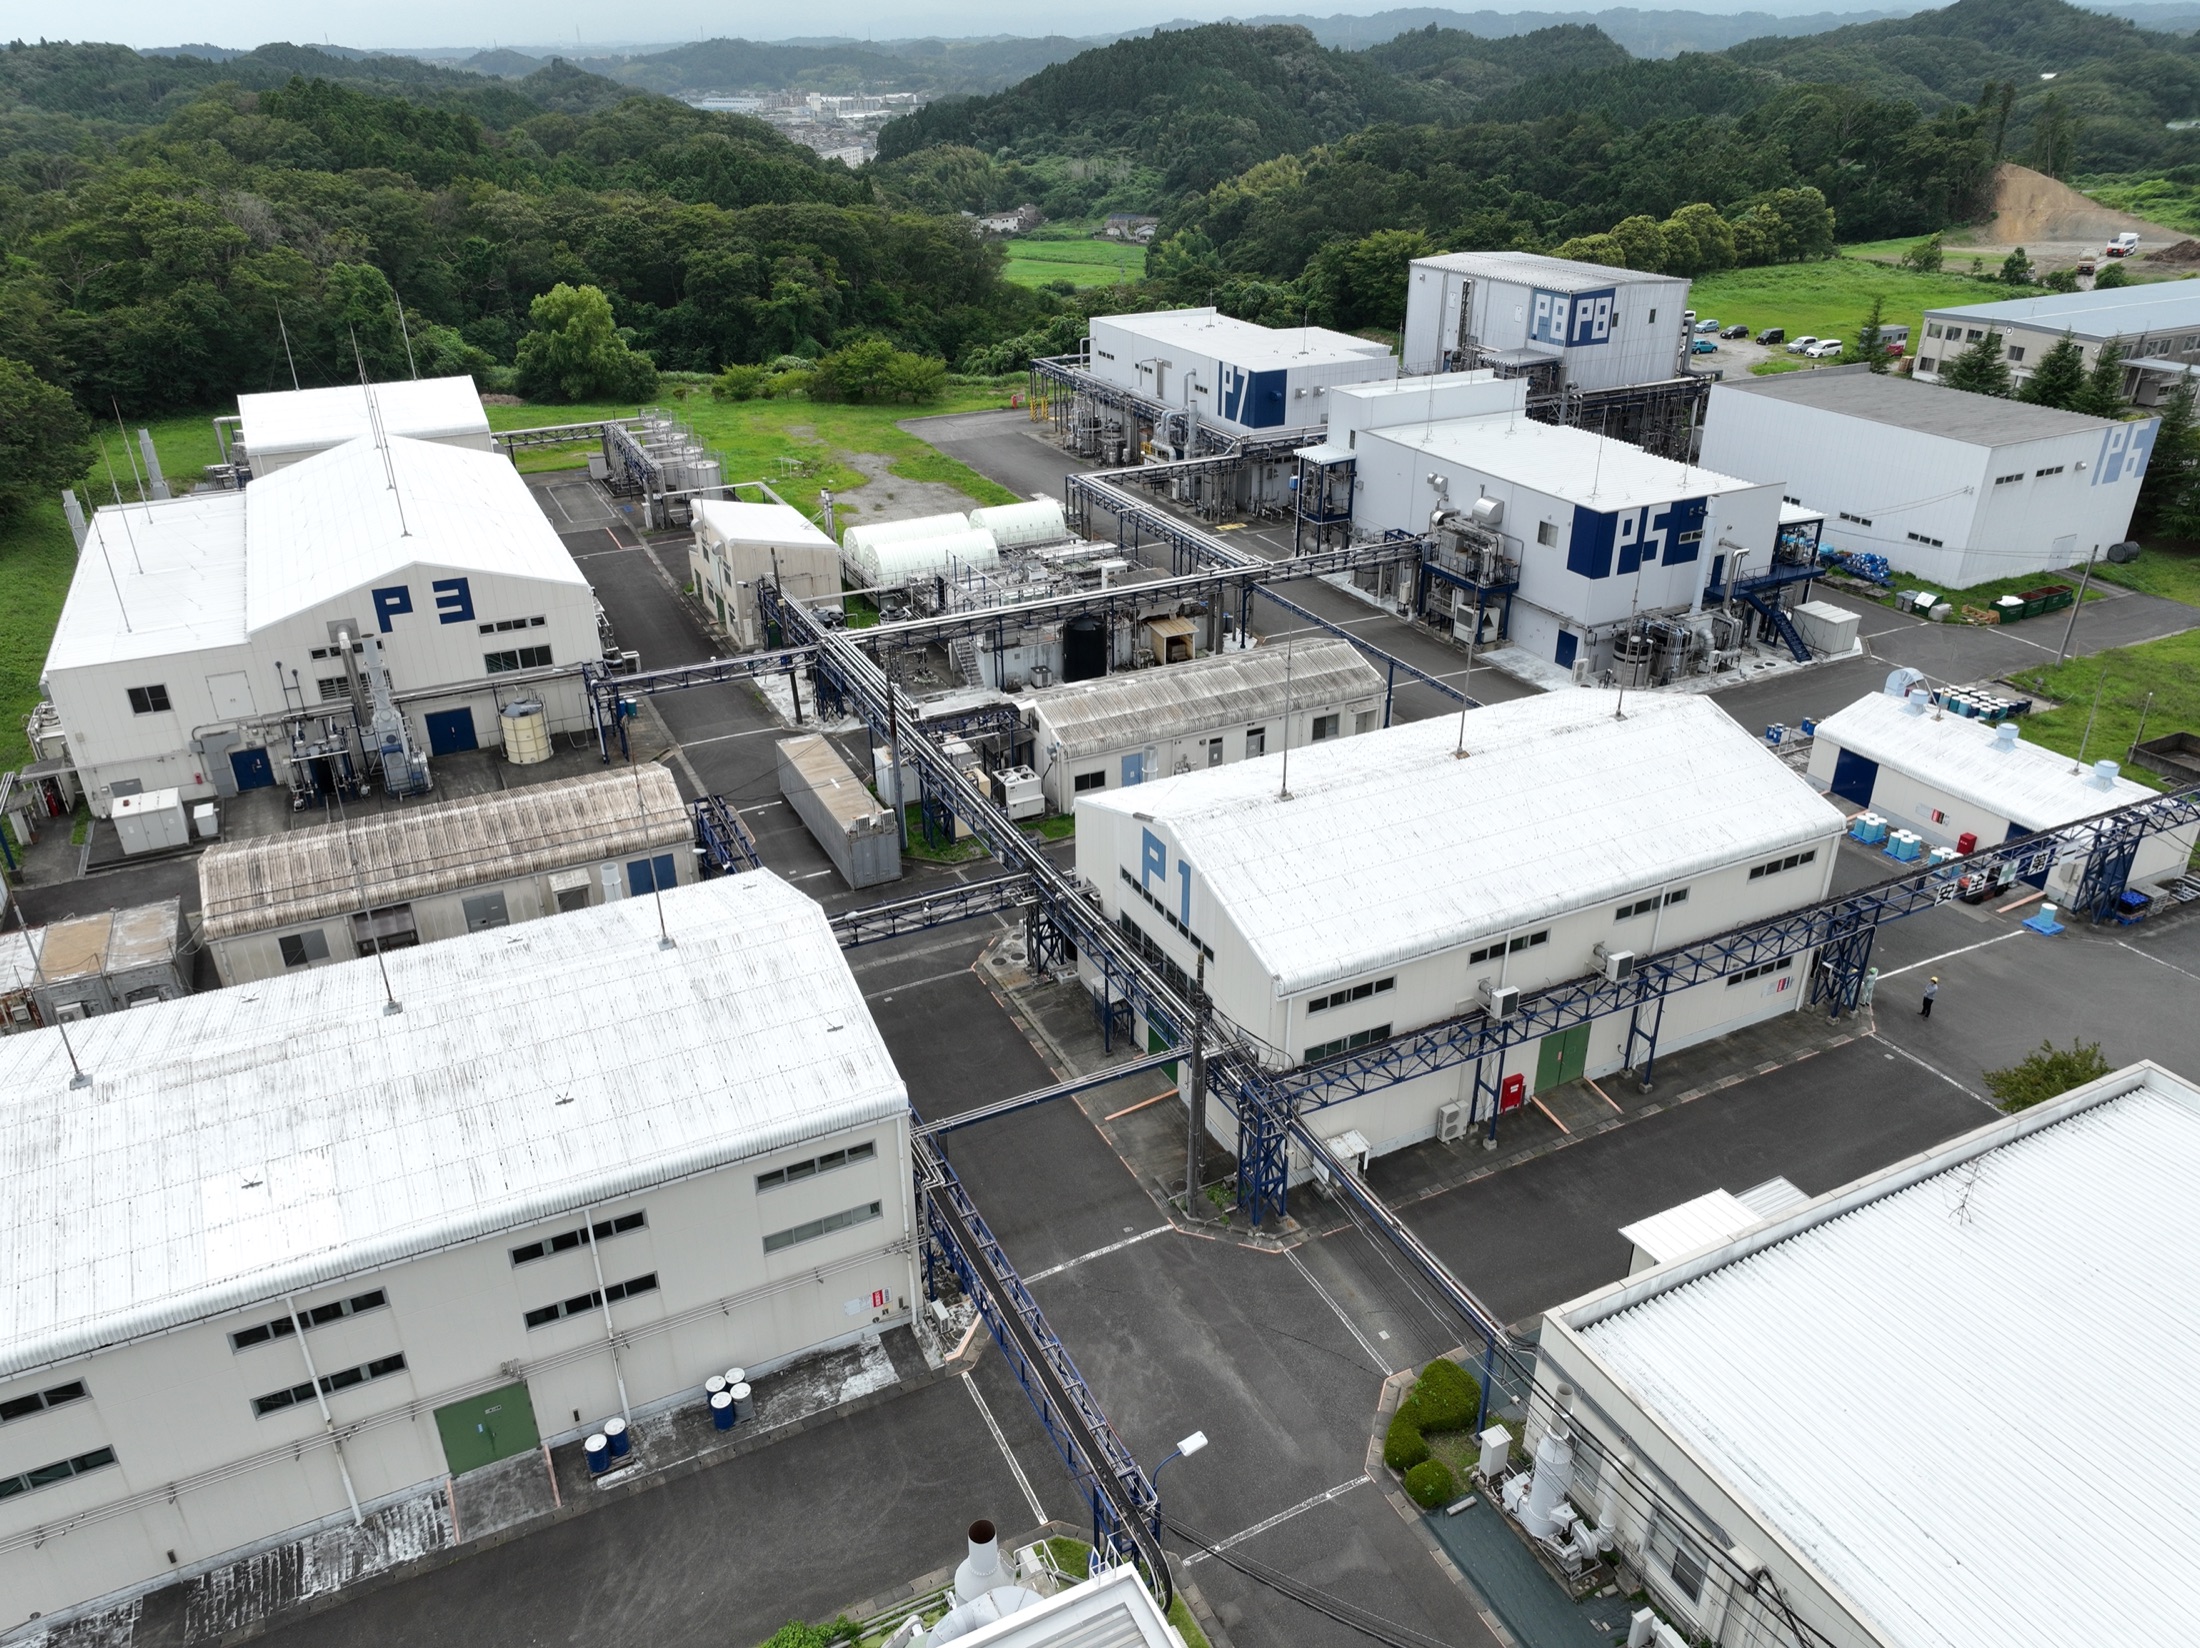
Iwaki Plant
〒972-8312 28-3 Hebinami, Jyoubanshimofunaocyou, Iwaki-City, Fukushima Pref. Tel +81-246-43-5200 Fax +81-246-43-5215
Approx. 10 minutes by taxi from Yumoto Station on the JR Joban Line
Our head office, Fukuoka Plant, and Iwaki Plant collaborate with one another to handle production, quality, and research and development functions. A system has been developed for underpinning quality and safety across the entire group by harnessing the expertise of each department.
→ Scroll horizontally to see more
Made up of Sogo Pharmaceutical Co., Ltd., SOGO Trading Co., Ltd., and SPC (Shanghai) Co., Ltd., the Sogo Pharmaceutical Group regards compliance as complying with laws and regulations as well as acting in accordance with higher ethical standards as required by society as reflected in social norms and morality. In the constantly changing business segments corresponding to pharmaceuticals and chemicals, having foresight, being willing to take on the challenge of developing new products, and speed are valued highly. We believe, however, that taking on this challenge must be done at all times in a manner that is consistent with social ethics, in other words, compliance. Since avoiding incidents and disasters is deemed to be the starting point for ensuring our corporate continuity, we are committed to safe operations and the prevention of disasters. The Sogo Pharmaceutical Group sees taking on challenges, safe operations, and compliance as the cornerstones of our corporate activities. Accordingly, we engage in management with an emphasis placed on compliance. Proper awareness and actions on the part of each and every person working for the Sogo Pharmaceutical Group are important for realizing compliance. We feel that asking yourself each time whether an action—even if it technically comes within the bounds of the law—is correct and right is essential for conducting business in a fair manner. The Sogo Pharmaceutical Group aims to grow alongside society by earning the trust and meeting the expectations of clients, shareholders, business partners, employees, local communities, and all other stakeholders and by providing innovative products and services through actions undertaken by each and every officer and employee according to high ethical standards and an elevated sense of responsibility in the course of the performance of day-to-day duties.
Sogo Pharmaceutical Group Officers and Employees Compliance Code